ASTM A213 TP316 Stainless Steel Tube
What is ASTM A213 TP316 Stainless Steel Tube
ASTM A213 / A213M is the ASTM International product specification for seamless ferritic and austenitic alloy-steel boiler, superheater, and heat-exchanger tubes. Grade TP316 is the molybdenum-bearing austenitic listed under UNS S31600, built for chloride-leaning cooling water, process condensers, and other heat-exchanger duties where plain 18-8 chemistry is not enough. The stainless chemistry table holds carbon at ≤0.08%, chromium at 16.0–18.0%, nickel at 10.0–14.0%, and — the defining addition — molybdenum at 2.00–3.00%. Buyers who write “316 HX tube” or “316 condenser tube” on a bill of materials still need to name A213 (or the separate ASME SA-213 adoption) on the purchase order so the mill knows which tube product standard, minimum-wall rules, hardness tests, and marking clauses apply.
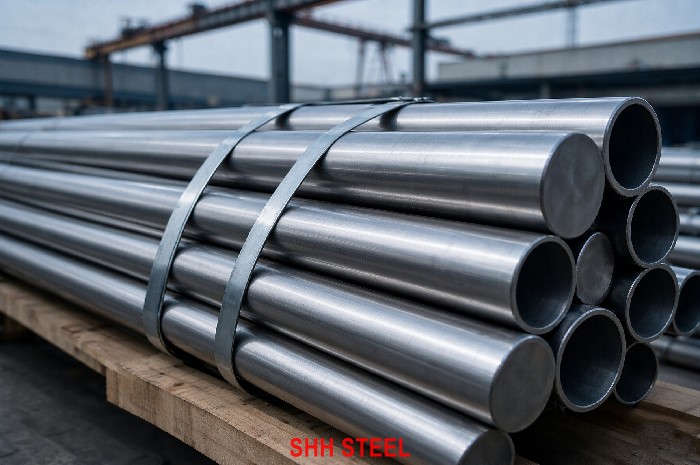
SHH STEEL can supply ASTM A213 TP316 stainless steel tube as seamless cold-finished and hot-finished product in the usual boiler and heat-exchanger OD × wall / BWG band, shipped with EN 10204 3.1 mill test certificates that report the full ladle chemistry — including the molybdenum window — and the Table 4 tensile and hardness results. When a project also needs ASME Code Book marking, we dual-mark A213 / SA-213 on the same lengths only if the purchase order says so — ASTM A213 and ASME SA-213 remain two independent standards. Browse the grade family on the A213/A213M hub.
Commercially, TP316 tube is still called 316, 18-8-2 Mo, or S31600 boiler/HX tube; none of those shop names replace the ASTM grade on the MTC or stencil. Sister grades under the same ASTM standard include A213 TP316L, A213 TP316H, A213 TP304 / A213 TP304L, A213 TP317L, and A213 TP321. A213 covers seamless tube only — there is no welded or HCW manufacturing type under this product standard — so cold-finished versus hot-finished seamless route is the finish/process choice, not a WLD/HCW stencil letter.
Chemical Composition of A213 TP316
Two chemistry layers matter for TP316 under ASTM A213. The melting (heat or ladle) analysis is mandatory for every heat under the stainless chemistry table, while product analysis on finished tube applies only when Supplementary Requirement wording or the purchase order invokes product analysis through the general requirements in ASTM A1016/A1016M. Product-analysis tolerances are not reprinted as a standalone chemistry table inside A213 itself; when ordered, they typically flow from ASTM A480/A480M Table A1.1 via that general-requirements path. SHH STEEL reports the actual ladle molybdenum inside 2.00–3.00% and does not advertise a “high-Mo shop grade” that the ASTM stainless table does not publish.
The tables below reproduce the heat analysis for TP316 / UNS S31600 and the product-analysis limits that result from applying A480 Table A1.1 tolerances. Values are maximum unless a range is shown, and an ellipsis (…) means the ordered edition sets no requirement for that element. Confirm the ordered A213/A213M edition on the purchase order — table number (Table 1 versus Table 2 for stainless) and any nitrogen row can shift by year.
Melting analysis (heat / ladle analysis)
| Element | TP316 (UNS S31600) melting analysis |
|---|---|
| Carbon (C) | ≤ 0.08 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 16.0 – 18.0 |
| Nickel (Ni) | 10.0 – 14.0 |
| Molybdenum (Mo) | 2.00 – 3.00 |
| Nitrogen (N) | … (no requirement; analysis method by agreement when reported) |
Source: ASTM A213/A213M stainless chemistry table for Grade TP316 / UNS S31600 (public specification table excerpts cross-checked). Confirm the ordered edition on the purchase order before treating any secondary catalogue as the acceptance text.
Product analysis — A480/A480M Table A1.1 tolerances applied to melt limits
| Element | Melting | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.08 | 0.01 over | ≤ 0.09 |
| Manganese (Mn) | ≤ 2.00 | 0.04 over | ≤ 2.04 |
| Phosphorus (P) | ≤ 0.045 | 0.010 over | ≤ 0.055 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 16.0 – 18.0 | 0.20 under / over | 15.80 – 18.20 |
| Nickel (Ni) | 10.0 – 14.0 | 0.10 under / 0.15 over | 9.90 – 14.15 |
| Molybdenum (Mo) | 2.00 – 3.00 | 0.05 under / 0.10 over | 1.95 – 3.10 |
Molybdenum is required, not optional, for TP316-family grades under A213 — a PMI gun that only reports Cr and Ni is not enough to clear the grade. Chromium sits lower than the TP304 band (16–18% versus 18–20%) while nickel sits higher (10–14% versus 8–11%), which is the classic Mo-bearing austenitic balance that stabilizes the structure once molybdenum is present. Carbon remains capped at 0.08% on the melt; heats that also meet the TP316L carbon ceiling can be dual-certified to A213 TP316L when both tensile floors and hardness limits are satisfied.
When product analysis is ordered, finished tube may read up to C 0.09%, Mn 2.04%, P 0.055%, S 0.035%, and Si 1.05%, with Cr 15.80–18.20%, Ni 9.90–14.15%, and Mo 1.95–3.10%. Those are the only product limits we quote from the A480 A1.1 path. Put any tighter project molybdenum floor or carbon ceiling on the purchase order before the heat is selected.
Mechanical Properties of A213 TP316
ASTM A213 Table 4 sets the tensile acceptance floor for TP316 at 75 ksi [515 MPa] tensile strength and 30 ksi [205 MPa] yield strength (0.2% offset), with elongation of 35% minimum in 2 in. or 50 mm — the same 75/30 ksi pair as TP304, not the lower L-grade floors. Unlike many ASTM A312 pipe rows for the same UNS number, A213 Table 4 also lists a hardness maximum for TP316 of 192 HBW / 200 HV or 90 HRB, and hardness tests are part of the lot acceptance scheme in the product standard. Every lot sampled under the edition’s specimen rules must meet those numbers after the final solution treatment.
| Property | TP316 requirement (Table 4) |
|---|---|
| Tensile strength, min | 75 ksi [515 MPa] |
| Yield strength (0.2% offset), min | 30 ksi [205 MPa] |
| Elongation in 2 in. or 50 mm, min | 35% |
| Hardness, max | 192 HBW / 200 HV or 90 HRB |
Source: ASTM A213/A213M Table 4 for TP316 / UNS S31600 (public specification summaries). Mechanical property requirements do not apply to tubing smaller than 1/8 in. [3.2 mm] inside diameter or thinner than 0.015 in. [0.4 mm] wall. Flattening and flaring tests are also required on a lot basis for finished tube; they sit beside tension and hardness rather than replacing them.
Actual mill certificates often clear the 75/30 ksi floor with margin, but design calculations should still use Table 4 unless the purchase order states higher guaranteed values that the mill has accepted in writing. For creep-range boiler service that needs a controlled carbon floor and grain-size language, open A213 TP316H rather than stretching standard TP316 beyond its intended framing. For as-welded IGC concern keep the molybdenum and step to A213 TP316L.
Dimensions and Tolerances
Dimensional supply for ASTM A213 TP316 is tube language — outside diameter × wall thickness (minimum wall or average wall) and, commercially, BWG / gauge — not ASME B36.19 pipe schedules as the primary size story. The sizes usually furnished under A213 run from about 1/8 in. [3.2 mm] inside diameter to 5 in. [127 mm] outside diameter, with minimum wall from about 0.015 to 0.500 in. [0.4 to 12.7 mm]; tubing with other diameters may be furnished when all other requirements of the specification are met. State on the purchase order whether wall is minimum or average, because that choice changes how the mill interprets tolerance and how the designer reads remaining wall after fabrication.
Outside-diameter and wall variations follow ASTM A1016/A1016M as invoked by A213, with cold-finished and hot-finished routes carrying different practical bands. Cold-finished tubes commonly hold tighter OD control; hot-finished tubes allow wider OD and wall windows. Permissible variations from a specified average wall for cold-finished tube are often summarized as ±10% of the specified average wall, while minimum-wall product is accepted to the A1016 minimum-wall tables rather than a symmetric ± window. Confirm the exact A1016 rows for the OD and finish route on the ordered edition — do not treat a catalogue one-liner as a substitute for the general-requirements table.
| Item | Typical A213 TP316 dimensional practice |
|---|---|
| Product form | Seamless only (cold-finished or hot-finished) |
| Usual size band | ~1/8 in. [3.2 mm] ID to 5 in. [127 mm] OD; wall ~0.015–0.500 in. [0.4–12.7 mm] min (or average wall if PO says so) |
| Wall basis | Minimum wall (default commercial practice) or average wall when specified |
| OD / wall tolerances | Per ASTM A1016/A1016M for the finish route and size; cold-finished average wall often ±10% |
| Length | Cut lengths for HX / boiler / condenser bundles, or mill random lengths by agreement |
| Secondary size note | ASME B36.19 schedules may appear only when a buyer asks for a pipe-schedule cross-reference — not as the primary A213 size callout |
Put the cut list, U-bend or straight-tube preference, and end preparation on the enquiry so mill and stock lengths can be mixed efficiently. Minimum wall is a first-class A213 concept: if the datasheet assumes average wall, say so explicitly before the heat is rolled.
Equivalent Grades
Equivalence language around TP316 tube is often looser than a chloride-service heat-exchanger purchase order can afford. ASTM A213 Grade TP316 / UNS S31600 is the governing designation for this article; EN 1.4401 and JIS SUS316 are approximate wrought names that point to similar Mo-bearing chemistry families but are not automatic substitutes on an A213 mill test certificate. When a datasheet says “equivalent to 316,” confirm which product standard, tensile/hardness table, and heat-treatment clause the mill will actually certify.
| Designation | Notes |
|---|---|
| ASTM A213 / A213M Grade TP316 | Governing ASTM seamless boiler / HX tube product standard for this article |
| UNS S31600 | Unified number listed in the stainless chemistry table |
| ASME SA-213 TP316 | Separate ASME Code Book adoption of the A213 grade text — dual-mark only when the PO asks |
| EN 1.4401 (X5CrNiMo17-12-2) | Approximate wrought Mo-bearing designation; order EN tube forms under the relevant EN tube specs |
| JIS SUS316 | Approximate Japanese grade name; confirm the Japanese tube product standard when ordering JIS product |
| Related plate | A240 / SA240 flat product in the same UNS family — order plate and tube under their own product standards |
ASME SA-213 TP316 is the separate Code Book adoption of the same grade text; dual A213/SA-213 marking is a purchase-order option, not a claim that the two standards are one document. Compare low-carbon, H-grade, and higher-Mo sisters (TP317 / TP317L) on their own ASTM A213 pages before swapping grades in a tube bundle.
Heat Treatment and Delivery Condition
TP316 under ASTM A213 is furnished solution treated at a minimum of 1900 °F [1040 °C], then quenched in water or cooled rapidly by other means at a rate sufficient to prevent carbide reprecipitation. That heat-treatment row applies to both cold-finished and hot-finished seamless tube. Molybdenum does not replace the anneal — under-cooling or skipping the quench can still leave a structure that sensitizes in service even when ladle Mo looked acceptable on paper.
Cold-finished versus hot-finished is a process and dimensional route, not a substitute for the anneal: cold-finished tube is typically drawn after hot working and then solution treated; hot-finished tube may be quenched after hot forming when the edition allows and finishing temperature is not below the minimum anneal. Delivery condition for SHH STEEL TP316 is solution annealed and pickled (or bright annealed by agreement), with heat-treatment temperature and quench method stated on the EN 10204 3.1 certificate. Straightening, cutting, and end finishing follow heat treatment.
When Supplementary Requirement language for intergranular-corrosion capability (commonly tied to ASTM A262 Practice E on specimens representative of the as-shipped condition for standard-carbon types) is ordered, the corrosion test report travels with the heat-treatment record. H-grade grain-size rules do not rewrite the TP316 path — use A213 TP316H when the datasheet calls for H-grade carbon and grain-size controls.
Corrosion Resistance
TP316’s molybdenum addition is the reason buyers step up from TP304 for chloride-bearing cooling water, coastal condensers, many brine-leaning process exchangers, and other services where pitting and crevice corrosion limit plain 18-8 tube. The chromium-nickel-molybdenum passive film handles oxidizing process fluids and a wider band of chloride-containing waters than TP304, but it is not a duplex or superaustenitic substitute — severe seawater, high-temperature chlorides, and under-deposit attack still need a design review and often a higher PREN grade such as A213 TP317L or A213 UNS S31254.
Intergranular corrosion risk after tube-to-tubesheet welding or after sensitizing thermal cycles is controlled by ordering A213 TP316L, by solution treating after fabrication when the sequence allows, or by invoking the contractual corrosion test on the tube PO. ASTM A213 itself does not publish a corrosion-rate or PREN table for TP316; selection remains engineering judgment against fluid, temperature, velocity, and inspection philosophy. When a specification calls for ASTM A262 Practice E, write that Supplementary Requirement onto the purchase order so the test is contractual rather than assumed from a verbal “full certs” note.
Applications of A213 TP316 Tube
TP316 is ordered when molybdenum is required for chloride or process corrosion resistance in seamless boiler, superheater, and heat-exchanger tube duty, and when standard carbon is acceptable for the fabrication sequence. The table below pairs typical application areas with a selection note so the grade is chosen for the fluid and temperature — not only for the familiar “316” name on the BOM.
| Application area | Typical use of TP316 tube | Selection note |
|---|---|---|
| Cooling-water / coastal condensers | Seamless condenser and cooler tubes in chloride-leaning utility water | Confirm chloride level, temperature, and cleaning chemistry; step to TP317L or S31254 if PREN is insufficient |
| Process heat exchangers | Straight and U-bend HX tubes in chemical and refining circuits needing Mo | State min vs average wall, BWG, and bend radius on the enquiry |
| Boiler and moderate-temperature steam | Seamless generating-bank and utility steam tubing ordered to A213 with Mo chemistry | For creep-critical H-grade service open TP316H |
| Pulp / paper and bleach-adjacent utilities | Utility HX where Mo-bearing austenitic tube is accepted | Severe bleach or high-chloride loops may need higher alloys |
| Food / pharmaceutical utilities | Utility and process HX where 316 stainless tube is accepted | Follow hygiene finish and welding procedure requirements; consider TP316L for as-welded joins |
| General corrosive tube duty | Seamless tube where A213 documentation and Mo chemistry are preferred over TP304 | Do not substitute A312 pipe paperwork for A213 tube acceptance |
For as-welded tube-to-tubesheet joints in sensitizing service consider TP316L or dual TP316/TP316L; for high-temperature creep-range boiler tubing open TP316H; for low-chloride oxidizing service A213 TP304 may still be the economical choice on the same A213/A213M hub.
Weldability
TP316 tube welds readily with matching or near-matching Mo-bearing austenitic filler for tube-to-tubesheet joints, attachment welds, and fabrication joins. Common practice uses ER316 / ER316L (or equivalent covered electrodes) under a qualified WPS; many exchanger fabricators prefer ER316L deposits for lower carbon in the weld metal even when the base tube is standard TP316. Heat input control, interpass limits, and post-weld cleaning remain the fabricator’s responsibility under the applicable boiler or pressure-vessel code — A213 governs the seamless tube product, not the field or shop weld procedure.
Because A213 TP316 is seamless, there is no mill longitudinal weld to radiograph the way welded pipe standards describe. Focus inspection language on tube integrity (hydro or NDE of each length), tube-to-tubesheet joint quality, and any contractual corrosion test on the base metal. For tube that will enter service as-welded in a sensitizing environment, many owners change the base metal to A213 TP316L rather than relying on a perfect weld procedure alone to protect standard-carbon TP316. Specify end preparation and surface finish on the tube PO when orbital or clean-service joins are planned.
Surface Finishes
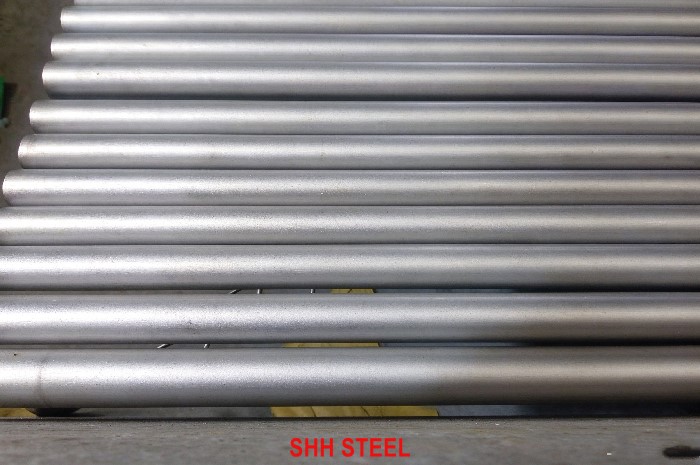
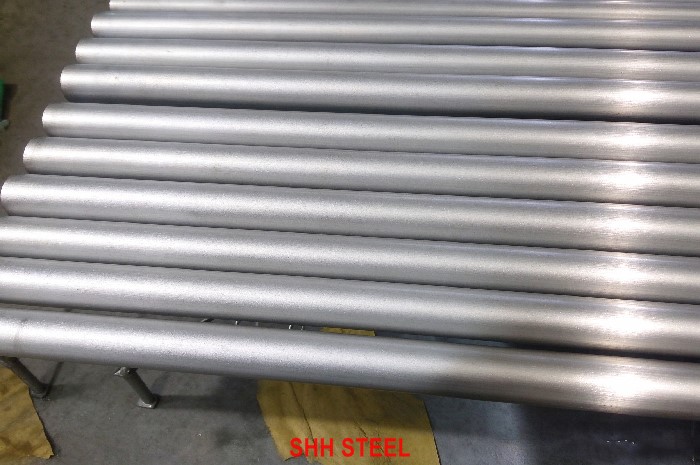
Standard mill delivery for ASTM A213 TP316 is solution annealed and pickled, leaving a clean matte finish suitable for most boiler, condenser, and heat-exchanger tube duty. Bright annealing under protective atmosphere produces a smoother reflective surface used on some clean-process and instrumentation tube lines and must be called out because it changes the heat-treatment route. Light polish or specified Ra on the bore or OD is a commercial or service-center operation on top of A213 product, not automatic with the grade stamp.
When a fouling-sensitive or hygienic exchanger specification quotes an Ra maximum on the bore, put it on the tube purchase order with its own acceptance language and sampling plan. SHH STEEL stencils grade and heat treatment as standard requirements; polish, special OD grind, and passivation after fabrication remain commercial extras unless the contract says otherwise. End preparation (plain, slightly beveled, or as needed for tube expanding) should be ordered together with finish so receiving inspection shares one acceptance language.
Inspection and Testing
Base ASTM A213 testing for TP316 includes heat analysis (with molybdenum inside 2.00–3.00%), tension tests to the Table 4 75/30 ksi floors, hardness tests to the Table 4 maximum, flattening and flaring tests on a lot basis, and either hydrostatic testing or nondestructive electric testing of each length. The manufacturer may choose hydro versus NDE unless the purchase order fixes the method; both are acceptance routes inside the product standard, not informal upgrades. Marking includes the ASTM designation, grade, size, heat number, and other clause-required data so receiving inspection can tie each length back to the MTC.
Supplementary Requirements commonly added on TP316 tube orders are summarized below. Invoke them by number or clear purchase-order wording; mills will not assume product analysis or intergranular-corrosion testing from a verbal “full certs” note.
| Option | Purpose |
|---|---|
| Product analysis | Confirms chemistry — including Mo — on finished tube (via A1016 / PO language) |
| Intergranular corrosion | A262 Practice E (or agreed practice) as a contractual Supplementary Requirement |
| Minimum vs average wall | States which wall basis the size callout uses |
| Fixed hydro or NDE method | Removes manufacturer’s option when the end user mandates one route |
| Third-party inspection / EN 10204 3.2 | Witnessed testing and certificate when the project requires it |
| Dual TP316/TP316L marking | When ladle carbon and both Table 4 rows support dual certification |
Lot definitions for continuous heat treatment or direct quench after hot forming follow the size-based lot sizes in A213; ask the mill to state lot identity clearly on the certificate so hardness and tension specimens map cleanly to the bundle you receive.
Packaging and Shipping
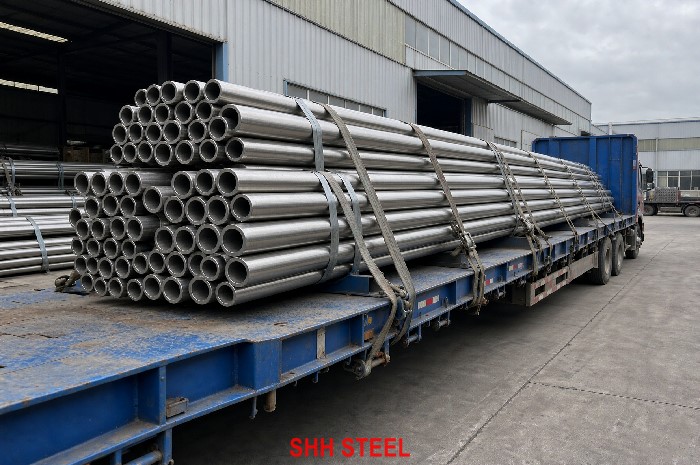
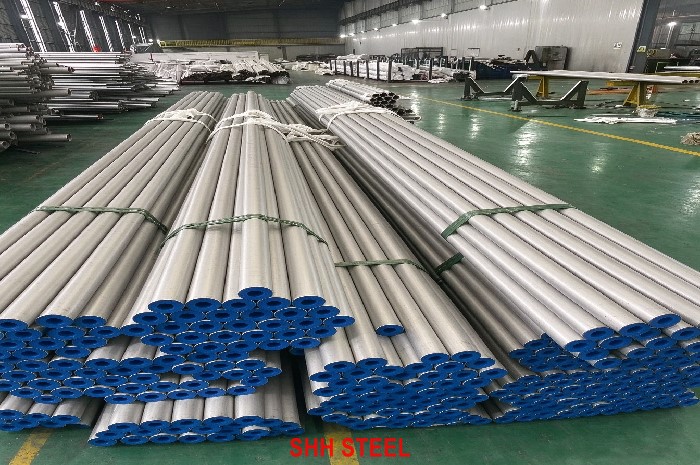
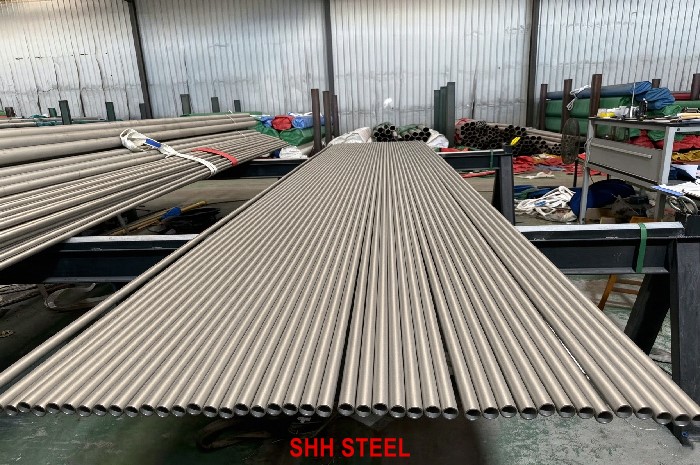
TP316 tube leaves SHH STEEL bundled, capped or end-protected, and tagged for export or domestic delivery according to the length mix and bend form on the order. Bundle tags repeat the ASTM A213 grade, OD × wall (or BWG), heat number, and PO reference so site receiving can check the shipment without opening every certificate packet first. U-bent tubes need extra cradle or case protection so bend radii and legs are not distorted in transit.
Export packing can be bare bundles, wrapped bundles, or wooden-cased lengths for bright-annealed, polished, or small-bore material. We ship under the Incoterms on the order acknowledgement — FOB, CFR, CIF, EXW, or other agreed terms. Inland trucking, bilingual destination marks, or project color coding for bundle tags should be stated on the enquiry beside the metallurgical notes.
Why Choose SHH STEEL
SHH STEEL treats ASTM A213 TP316 as a product standard with enforceable molybdenum chemistry, tensile, hardness, heat-treatment, and marking rules — not as a catalogue nickname for “any 316 tube.” The MTC reports the full ladle chemistry including Mo 2.00–3.00% and the Table 4 75/30 ksi tensile/hardness set; the stencil carries seamless tube identity under A213; and dual A213/SA-213 marking is offered only when requested so Code and non-Code jobs stay cleanly documented.
We keep the 316-family conversation honest for chloride and process HX duty. If as-welded intergranular resistance is the driver, we steer toward A213 TP316L or dual TP316/TP316L. If creep-range boiler service needs H-grade carbon and grain-size controls, we open A213 TP316H. If chlorides are mild enough that molybdenum is not justified, we open A213 TP304 / A213 TP304L. The A213/A213M hub is organized the same way — grade by grade under ASTM, seamless tube only.
Lead times combine near-term stock lengths with mill schedules; we say which is which on the quotation. Cut-to-length, U-bending, polish, and third-party inspection are defined extras. The tube that arrives should match the ASTM callout the engineer wrote, with paperwork a third-party inspector can read without translation.
Supply Capability
SHH STEEL can supply ASTM A213 TP316 stainless steel tube against the edition and finish route named on your enquiry. The capability table below summarizes the sizes, finishes, and documents we regularly quote for this molybdenum grade, followed by the Stock / Available sizes map buyers ask for when they need a quick sense of what to enquire against for condenser and heat-exchanger duty.
| Item | SHH STEEL capability for TP316 |
|---|---|
| Standard | ASTM A213 / A213M (dual SA-213 marking on request) Grade TP316 / UNS S31600 |
| Product form | Seamless only — cold-finished and hot-finished |
| Size | Typical OD × min wall (or average wall) in the A213 usual band; other diameters by agreement |
| Wall / gauge | Minimum wall or average wall; BWG / gauge callouts accepted on enquiry |
| Length | Cut-to-length for HX / condenser / boiler bundles; mill random by agreement; U-bends on enquiry |
| Finish | Annealed and pickled; bright annealed or light polish by agreement |
| Testing | Tension (75/30 ksi), hardness (max 192 HBW / 90 HRB), flattening, flaring, hydro or NDE per length; full ladle chemistry including Mo on MTC; product analysis / IGC on order |
| Documents | EN 10204 3.1 with full ladle chemistry; third-party inspection / 3.2 on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
Stock / Available sizes
SHH STEEL quotes TP316 tube against a practical stock-and-mill enquiry range rather than a frozen warehouse SKU list. The sizes below are the OD × wall / BWG combinations buyers most often request for chloride-service condensers and process exchangers; availability of any single line on a given week depends on mill drawing and our inbound schedule, so treat the table as a supply map for enquiry — not a guarantee that every line sits on the floor with a published tonnage.
| Item | Typical stock / enquiry range for TP316 |
|---|---|
| Outside diameter | 12.7, 15.88, 19.05, 25.4, 31.8, 38.1, 50.8, 63.5, 76.2 mm (and other HX/condenser ODs on enquiry; up through the usual A213 ~5 in. [127 mm] band) |
| Wall / BWG | BWG 10–20 class walls and metric min-wall equivalents; lighter and heavier walls by agreement |
| Common OD × wall examples | 19.05 × 1.65 mm; 19.05 × 2.11 mm; 25.4 × 2.11 mm; 25.4 × 2.77 mm; 31.8 × 2.77 mm; 38.1 × 2.77 mm; 50.8 × 2.77 mm — illustrative condenser/HX sizes, confirm min vs average wall |
| Length | Cut lengths for exchanger and condenser bundles; U-bends and straight random lengths on enquiry |
| Special | Non-standard OD/wall, bright anneal, polished bore, dual TP316/TP316L, and dual A213/SA-213 marking — confirm on enquiry before the heat is reserved |
When you send an enquiry, list OD × wall (or BWG), wall basis (minimum or average), cold-finished or hot-finished preference, quantity or cut list, required marking (A213 alone, dual A213/SA-213, and/or dual TP316/TP316L), and any Supplementary Requirements. We reply with what we can ship from near-term stock versus what needs a mill run, without inventing fake warehouse codes or tonnage claims.
Send the size list, finish route, quantity or cut lengths, required marking, Supplementary Requirements, and destination on one enquiry. We will confirm molybdenum chemistry and the 75/30 ksi tensile/hardness set against the ordered edition, state what ships from near-term availability versus mill production, and keep the offer aligned with the ASTM A213 / A213M product standard that governs this page. Related grades such as A213 TP317, A213 TP317L, and A213 UNS S31254 sit on the same hub when the datasheet steps beyond standard TP316.
FAQ
-
Is ASTM A213 the same as ASME SA-213 for TP316?
- No. ASTM A213 / A213M is the ASTM International product specification for seamless boiler, superheater, and heat-exchanger tubes; ASME SA-213 / SA-213M is the separate ASME Code Book adoption of that grade text. Chemistry, tensile, and hardness floors align closely for a given referenced edition, but they remain two independent standards. Dual-mark A213/SA-213 tube only when the purchase order asks for both names on the stencil and MTC.
-
Does ASTM A213 TP316 include welded or HCW tube?
- No. ASTM A213 covers seamless tube only. There is no WLD or HCW manufacturing type under this product standard the way ASTM A312 describes pipe. The process choice for TP316 under A213 is cold-finished versus hot-finished seamless tube, plus the heat-treatment and testing clauses of the ordered edition. If you need welded stainless pipe, that is a different product standard and a different steelspecs page family.
-
Why does TP316 require molybdenum under A213?
- Molybdenum at 2.00–3.00% on the melt is a required element for Grade TP316 / UNS S31600 in the A213 stainless chemistry table — it is not optional and not a shop upgrade. Mo improves resistance to chloride pitting and crevice corrosion relative to TP304 in many cooling-water and process exchanger services. A certificate or PMI report that omits molybdenum does not clear TP316 acceptance under A213.
-
Minimum wall vs average wall — which should I order for A213 TP316?
- Order minimum wall when the design and datasheet are written around a guaranteed minimum thickness after tolerance. Order average wall only when the purchase order explicitly allows average-wall product and the designer has accepted that basis. The two readings produce different tube from the same OD × wall line, so put the wall basis on the enquiry before the mill selects tooling and tolerance tables from A1016.
-
Hydrostatic test vs NDE — which do I get on TP316 tube?
- ASTM A213 requires each tube to be hydrostatically tested or nondestructively electrically tested. The manufacturer may choose the method unless the purchase order fixes one. Neither route is an informal upgrade over the other inside the product standard. State the preferred method on the enquiry if your end user or inspector mandates hydro only or a named NDE technique.
-
Does A213 Table 4 set a hardness limit for TP316?
- Yes. Table 4 for TP316 lists tensile strength 75 ksi, yield strength 30 ksi, elongation 35%, and a hardness maximum of 192 HBW / 200 HV or 90 HRB. Hardness tests are part of lot acceptance under A213, which differs from many A312 pipe rows for the same UNS number that omit a Table 4 hardness cap. If a project needs a tighter hardness window than Table 4, write it into the purchase order as an additional requirement.
-
What is the UNS number and chemistry of ASTM A213 TP316?
- TP316 is UNS S31600. Melting limits include carbon ≤0.08%, manganese ≤2.00%, phosphorus ≤0.045%, sulfur ≤0.030%, silicon ≤1.00%, chromium 16.0–18.0%, nickel 10.0–14.0%, and molybdenum 2.00–3.00%, with nitrogen as a no-requirement ellipsis in the public table excerpts used here. Product-analysis limits apply only when ordered, typically from A480 Table A1.1 tolerances via the A1016 general-requirements path.
-
TP316 vs TP316L — which A213 tube should I order?
- Order TP316 when the specification calls for the standard 75/30 ksi tensile floor, molybdenum 2.00–3.00%, and carbon ≤0.08% is acceptable. Order TP316L when as-welded intergranular resistance is also required and the lower 70/25 ksi floor is acceptable. Dual TP316/TP316L certification is possible on qualifying heats — ask for it on the PO rather than assuming it from a PMI gun reading.
-
TP304 vs TP316 — which A213 grade is better in chlorides?
- TP316 adds molybdenum and generally resists chloride pitting and crevice corrosion better than TP304 in seawater-leaning cooling water, brines, and many process exchangers. TP304 remains appropriate for many oxidizing and low-chloride steam and process services. ASTM A213 does not publish a chloride ranking table; open the TP316 tube page when chlorides dominate, and step further to TP317L or S31254 when PREN requirements exceed standard 316.
-
TP316 vs TP316H — when do I need the H grade under A213?
- Order TP316H when the boiler or superheater datasheet needs the H-grade carbon range, grain-size controls, and creep-rupture framing that the H designation carries under A213. Standard TP316 remains appropriate for many moderate-temperature HX and chloride-service tube duties. Do not treat "316H" as a synonym stamp for ordinary TP316 on the MTC.
-
What heat treatment does ASTM A213 require for TP316?
- TP316 is solution treated at a minimum of 1900 °F [1040 °C] and then water quenched or rapidly cooled to prevent carbide reprecipitation. Both cold-finished and hot-finished seamless tube follow that heat-treatment requirement. Ask the mill to state anneal temperature and quench method on the EN 10204 3.1 certificate so receiving inspection can clear the heat without chasing verbal confirmations.
-
Can you dual-certify ASTM A213 and ASME SA-213 TP316, or TP316/TP316L?
- Yes on both axes when the heat and testing support it. Dual A213/SA-213 marking is available when the purchase order requests both independent standards on the stencil and MTC. Dual TP316/TP316L is available when ladle chemistry meets the tighter carbon rules and tensile plus hardness results clear both Table 4 rows. Spell the required marking on the enquiry so the heat is selected correctly.
Conclusion
ASTM A213 TP316 / UNS S31600 is the molybdenum-bearing seamless stainless steel tube grade for boiler, superheater, and heat-exchanger service when chloride or process corrosion resistance requires Mo 2.00–3.00% and standard carbon is acceptable. SHH STEEL supplies cold-finished and hot-finished seamless tube in the usual OD × wall / BWG band, solution annealed, tested to the Table 4 75/30 ksi tensile and hardness limits, and documented on EN 10204 3.1 certificates — with dual SA-213 marking only when the order asks for that separate ASME standard. For sister grades and stock-oriented size discussions, start from the A213/A213M hub, then send your OD × wall list, wall basis, and marking requirements so we can align mill and near-term availability to the ASTM callout.
Contact: admin@steelspecs.com
Quality Steel Needed? Inquire for Offers
Related Products