ASTM A213 TP321 Stainless Steel Tube
What is ASTM A213 TP321 Stainless Steel Tube
ASTM A213 / A213M is the product specification for seamless ferritic and austenitic alloy-steel boiler, superheater, and heat-exchanger tubes. Grade TP321 / UNS S32100 is the titanium-stabilized chromium-nickel austenitic listed for tube duty where grain-boundary chromium carbides must be tied up without dropping to an L-grade carbon ceiling: melting carbon is capped at 0.08%, chromium at 17.0–19.0%, nickel at 9.0–12.0%, and titanium held to a formula minimum of five times (C + N) with a 0.70% absolute ceiling. Molybdenum is an ellipsis — no requirement — so TP321 is not a chloride-pitting upgrade over A213 TP304; it is a stabilization upgrade. Table 4 sets tensile at 75 ksi [515 MPa] / 30 ksi [205 MPa] with elongation 35% minimum and hardness max 192 HBW / 90 HRB.
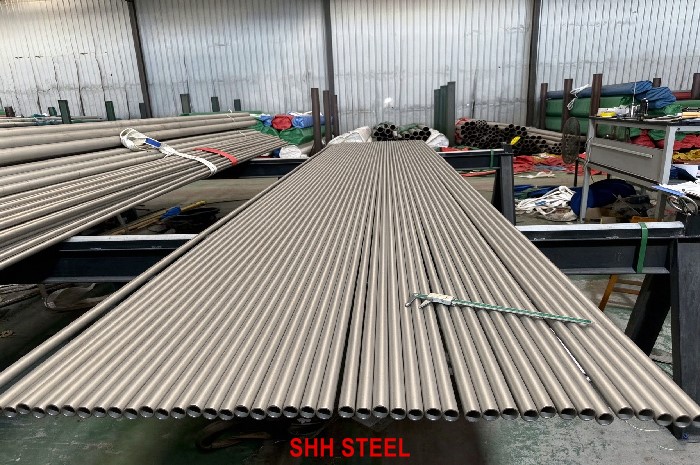
SHH STEEL can supply ASTM A213 TP321 stainless steel tube as seamless cold-finished and hot-finished product in the usual boiler and heat-exchanger OD × wall / BWG band, shipped with EN 10204 3.1 mill test certificates that report the full ladle chemistry — titanium against measured C + N — plus the Table 4 tensile and hardness results. Dual A213 / SA-213 marking is offered only when the purchase order asks for both independent standards. Start from the A213/A213M hub for sister stabilized and L-grade tube rows.
Commercial shorthand such as 321, S32100, or “Ti-stabilized HX tube” never replaces the ASTM grade on the MTC or stencil. Sister grades under the same ASTM standard include A213 TP321H, A213 TP347, A213 TP304L, A213 TP316Ti, and A213 TP304. A213 covers seamless tube only — there is no welded or HCW manufacturing type — so cold-finished versus hot-finished seamless route is the finish/process choice.
Chemical Composition of A213 TP321
Two chemistry layers matter for TP321 under ASTM A213. Melting analysis is mandatory for every heat; product analysis on finished tube applies only when Supplementary Requirement wording or the purchase order invokes it through ASTM A1016/A1016M, with tolerances typically from ASTM A480/A480M Table A1.1. The line that defines the grade is titanium ≥5 × (C + N) and ≤0.70%: a heat with C + N = 0.08% needs at least 0.40% Ti, while a leaner C + N heat can clear the formula with less titanium, still capped at 0.70%. Chromium 17.0–19.0% and nickel 9.0–12.0% sit near the 18-8 family but are not identical to TP304’s 18–20 / 8–11 windows. Molybdenum and niobium are ellipses — no requirement — so do not expect Mo on a TP321 MTC the way A213 TP316Ti requires it.
The tables below reproduce the melt limits for TP321 / UNS S32100, the product-analysis limits from A480 Table A1.1 practice, and a short titanium / Mo snapshot against TP304L, TP316Ti, and TP347. Later A213 editions place austenitic stainless grades in Table 2 (older editions used Table 1); confirm the ordered edition on the purchase order.
Melting analysis (heat / ladle analysis)
| Element | TP321 (UNS S32100) melting analysis |
|---|---|
| Carbon (C) | ≤ 0.08 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 17.0 – 19.0 |
| Nickel (Ni) | 9.0 – 12.0 |
| Molybdenum (Mo) | … (no requirement) |
| Nitrogen (N) | … (no requirement; analysis method by agreement when reported for the Ti formula) |
| Titanium (Ti) | ≥ 5 × (C + N), ≤ 0.70 |
Source: ASTM A213/A213M stainless chemistry table for Grade TP321 / UNS S32100 (public mill / specification PDF excerpt — _ref_a213.txt / A213–13 table text). Confirm the ordered edition. Where ellipses appear, the ordered edition sets no requirement for that element; nitrogen must still be known when titanium is checked against the 5 × (C + N) formula.
Product analysis — A480/A480M Table A1.1 tolerances applied
| Element | Melting | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.08 | 0.01 over | ≤ 0.09 |
| Manganese (Mn) | ≤ 2.00 | 0.04 over | ≤ 2.04 |
| Phosphorus (P) | ≤ 0.045 | 0.010 over | ≤ 0.055 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 17.0 – 19.0 | 0.20 under / over | 16.80 – 19.20 |
| Nickel (Ni) | 9.0 – 12.0 | 0.10 under / 0.15 over | 8.90 – 12.15 |
| Titanium (Ti) | ≥ 5 × (C+N), ≤ 0.70 | 0.05 over on max (Ti to 1.00 band practice) | max ≤ 0.75 product; min tied to heat C+N |
Stabilization snapshot — TP304L / TP321 / TP316Ti / TP347
| Element | TP304L (S30403) | TP321 (S32100) | TP316Ti (S31635) | TP347 (S34700) |
|---|---|---|---|---|
| C | ≤ 0.035 | ≤ 0.08 | ≤ 0.08 | ≤ 0.08 |
| Cr / Ni | 18–20 / 8–12 | 17–19 / 9–12 | 16–18 / 10–14 | 17–20 / 9–13 |
| Mo | … | … | 2.00 – 3.00 | … |
| Stabilizer | low C | Ti ≥5×(C+N) ≤0.70 | Ti ≥5×(C+N) ≤0.70 | Nb 10×C – 1.10 |
Read titanium against measured carbon and nitrogen on the same heat. Versus A213 TP304L, TP321 accepts a higher carbon ceiling because titanium does the stabilization work. Versus A213 TP316Ti, TP321 has no molybdenum requirement. Versus A213 TP347, stabilization is titanium rather than niobium. Dual TP321/TP304L is not a meaningful path: the carbon and titanium rules do not line up as a single heat story.
When product analysis is ordered, finished tube may read C ≤0.09%, Mn ≤2.04%, P ≤0.055%, S ≤0.035%, Si ≤1.05%, Cr 16.80–19.20%, Ni 8.90–12.15%, and Ti max ≤0.75% with the formula minimum still tied to heat C + N. Put any tighter project titanium floor on the purchase order before the heat is selected.
Mechanical Properties of A213 TP321
ASTM A213 Table 4 sets the tensile acceptance floor for TP321 at 75 ksi [515 MPa] tensile strength and 30 ksi [205 MPa] yield strength (0.2% offset), with elongation of 35% minimum in 2 in. or 50 mm and hardness max 192 HBW / 200 HV or 90 HRB — the same room-temperature pair as TP304 and TP316Ti. Unlike H grades, the heat-treatment table does not print a mandatory ASTM grain-size number for TP321; titanium stabilization, not coarse-grain control, is the elevated-temperature differentiation this grade brings. Supplementary Requirement S3 (unstraightened tubes) may reduce the Table 4 yield by 5 ksi [35 MPa] when ordered — put that on the PO rather than assuming it.
| Property | TP321 requirement (Table 4) |
|---|---|
| Tensile strength, min | 75 ksi [515 MPa] |
| Yield strength (0.2% offset), min | 30 ksi [205 MPa] |
| Elongation in 2 in. or 50 mm, min | 35% |
| Hardness, max | 192 HBW / 200 HV or 90 HRB |
| Grain size | No mandatory ASTM grain-size number in the public heat-treatment table for TP321 |
Source: ASTM A213/A213M Table 4 for TP321 / UNS S32100 (public specification PDF excerpt — _ref_a213.txt). Mechanical property requirements do not apply to tubing smaller than 1/8 in. [3.2 mm] inside diameter or thinner than 0.015 in. [0.4 mm] wall. Flattening and flaring tests are also required on a lot basis.
A tensile-only MTC that omits titanium is incomplete for TP321 — ask for Ti against C + N on the EN 10204 3.1 certificate before releasing the heat to fabrication. When a datasheet also wants H-grade carbon and grain-size controls, open A213 TP321H rather than stretching a standard TP321 heat into an H-grade story.
Dimensions and Tolerances
Dimensional supply for ASTM A213 TP321 is tube language — OD × wall (minimum or average) and commercially BWG / gauge — not ASME B36.19 pipe schedules as the primary size story. Usual A213 sizes run from about 1/8 in. [3.2 mm] ID to 5 in. [127 mm] OD, with minimum wall about 0.015–0.500 in. [0.4–12.7 mm]; other diameters may be furnished when all other requirements are met. State min versus average wall on the purchase order — boiler and heat-exchanger datasheets almost always assume minimum wall.
OD and wall variations follow ASTM A1016/A1016M as invoked by A213. Cold-finished tubes commonly hold tighter OD control; hot-finished tubes allow wider windows. Cold-finished average-wall product is often summarized as ±10% of the specified average wall; minimum-wall product follows the A1016 minimum-wall tables. Confirm the exact rows for the OD and finish route on the ordered edition.
| Item | Typical A213 TP321 dimensional practice |
|---|---|
| Product form | Seamless only (cold-finished or hot-finished) |
| Usual size band | ~1/8 in. [3.2 mm] ID to 5 in. [127 mm] OD; wall ~0.015–0.500 in. [0.4–12.7 mm] min (or average wall if PO says so) |
| Wall basis | Minimum wall (default commercial practice) or average wall when specified |
| OD / wall tolerances | Per ASTM A1016/A1016M for the finish route and size |
| Length | Cut lengths for HX / boiler bundles, or mill random lengths by agreement |
| Secondary size note | ASME B36.19 schedules only as a buyer-requested cross-reference — not the primary A213 callout |
Put the cut list, U-bend preference, and end preparation on the enquiry. Minimum wall remains a first-class A213 concept regardless of titanium stabilization.
Equivalent Grades
Equivalence language around 321 tube often collapses plate and tube product forms into one nickname, or treats TP321 as “304 with titanium.” ASTM A213 Grade TP321 / UNS S32100 is the governing designation for this article; EN 1.4541 and JIS SUS321 are approximate wrought names that point to similar Ti-stabilized chemistry families but are not automatic substitutes on an A213 MTC.
| Designation | Notes |
|---|---|
| ASTM A213 / A213M Grade TP321 | Governing ASTM seamless boiler / HX tube product standard for this article |
| UNS S32100 | Unified number in the stainless chemistry table |
| ASME SA-213 TP321 | Separate ASME Code Book adoption — dual-mark only when the PO asks |
| Related H-grade | A213 TP321H — C 0.04–0.10, Ti 4×(C+N)–0.70, grain-size path |
| Related Nb-stabilized | A213 TP347 — Nb stabilizer, no Ti formula |
| Related Mo + Ti | A213 TP316Ti — Ti formula plus Mo 2–3% |
| Related L-grade | A213 TP304L — low C without Ti |
| Related plate | A240 / SA240 flat product in the 321 family — order plate and tube under their own standards |
Dual A213/SA-213 marking is a purchase-order option. Compare TP321H, TP347, and TP316Ti on their own ASTM A213 pages before swapping stabilized tube inside a boiler or exchanger list.
Heat Treatment and Delivery Condition
TP321 under ASTM A213 is furnished solution treated at a minimum of 1900 °F [1040 °C], then quenched in water or cooled rapidly by other means. The public heat-treatment table marks this row with Footnotes F and H. Footnote F ties quench capability to A262 Practice E demonstrability when that test is ordered (Supplementary Requirement S4); Footnote H warns that a solution treating temperature above 1950 °F [1065 °C] may impair intergranular-corrosion resistance after subsequent sensitizing exposure, and allows a purchaser-specified lower-temperature stabilization or resolution anneal after the higher solution anneal. The public table does not print a mandatory ASTM grain-size number for TP321.
Supplementary Requirement S2 lists TP321 among grades that shall be given a stabilization heat treatment at a temperature lower than the initial solution anneal when the purchaser specifies S2 — temperature as agreed between purchaser and vendor. Supplementary Requirement S1 allows stress-relieved annealed TP321 (1500–1650 °F [815–900 °C] after roll straightening) for certain chloride stress-corrosion services when ordered. Neither S1 nor S2 is automatic with the grade stamp.
Cold-finished versus hot-finished is a process and dimensional route, not a substitute for the anneal. Delivery condition for SHH STEEL TP321 is solution annealed and pickled (or bright annealed by agreement), with anneal temperature, quench method, and titanium result on the EN 10204 3.1 certificate. For H-grade carbon and grain-size controls open A213 TP321H.
Corrosion Resistance
TP321’s defining corrosion claim versus standard TP304 is titanium stabilization: free carbon (and nitrogen) are tied as titanium carbides/nitrides so grain-boundary chromium carbides are less likely to form during slow cooling or repeated thermal exposure in the sensitizing range. That makes TP321 a common choice for welded and thermally cycled exchanger and moderate-temperature boiler tube where L-grade carbon is not mandated but IGC resistance still matters. It does not add molybdenum — chloride pitting and crevice performance remain in the 18Cr-Ni family, so coastal or brine-leaning services usually step to A213 TP316 / A213 TP316L or A213 TP316Ti.
ASTM A213 itself does not publish a corrosion-rate table for TP321; selection remains engineering judgment against fluid, temperature, velocity, and inspection philosophy. When a specification calls for ASTM A262 Practice E, write Supplementary Requirement S4 onto the purchase order so the test is contractual, and consider S2 stabilization when the Ti-bearing grade needs that path to clear Practice E. SHH STEEL will not rank TP321 as equal to Mo-bearing grades in chlorides.
Applications of A213 TP321 Tube
Because TP321 combines an 18Cr-Ni austenitic base with titanium stabilization, it shows up in process heat exchangers and condensers where as-welded or thermally cycled IGC resistance is needed without an L-grade carbon mandate, moderate-temperature steam and process circuits that historically named 321, and exhaust or recovery exchangers that sit below H-grade creep framing. The table below pairs typical application areas with a selection note.
| Application area | Typical use of TP321 tube | Selection note |
|---|---|---|
| Ti-stabilized process HX | Straight and U-bend tubes when Ti formula is named | Confirm Ti ≥5×(C+N) on MTC, not PMI of “some Ti” |
| As-welded moderate-temp steam | When L-grade is not mandated but IGC still matters | Consider S2 / S4 when A262 is contractual |
| Creep-critical H-grade lists | Usually prefer TP321H rather than TP321 | H-grade carbon + grain-size path |
| Chloride-leaning cooling water | Step to TP316 / TP316L / TP316Ti | TP321 has no Mo requirement |
| Nb-stabilized preference | Open TP347 on the same hub | Different stabilizer chemistry |
For H-grade open A213 TP321H; for Mo + Ti open A213 TP316Ti; for low-carbon without Ti open A213 TP304L; browse the rest on the A213/A213M hub.
Weldability
TP321 tube welds with matching or near-matching titanium-bearing austenitic filler for tube-to-tubesheet joints, attachment welds, and fabrication joins. Common practice uses ER321 / ER347 under a qualified WPS so weld-metal stabilization tracks the Ti-bearing base tube; some fabricators prefer niobium-bearing ER347 deposits for lower titanium sensitivity in the weld metal. Heat input control, interpass limits, and post-weld cleaning remain the fabricator’s responsibility — A213 governs the seamless tube product, not the field or shop weld procedure.
Because A213 TP321 is seamless, there is no mill longitudinal weld to radiograph the way welded pipe standards describe. Focus inspection language on tube integrity (hydro or NDE of each length), tube-to-tubesheet joint quality, and any contractual corrosion test on the base metal. For chloride services after welding, changing the base metal to A213 TP316Ti or A213 TP316L is usually a better move than relying on filler selection alone. Specify end preparation and surface finish on the tube PO when orbital or clean-service joins are planned.
Surface Finishes
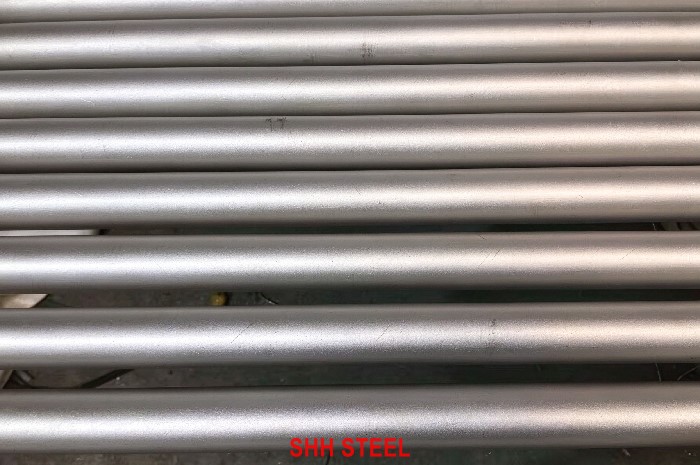
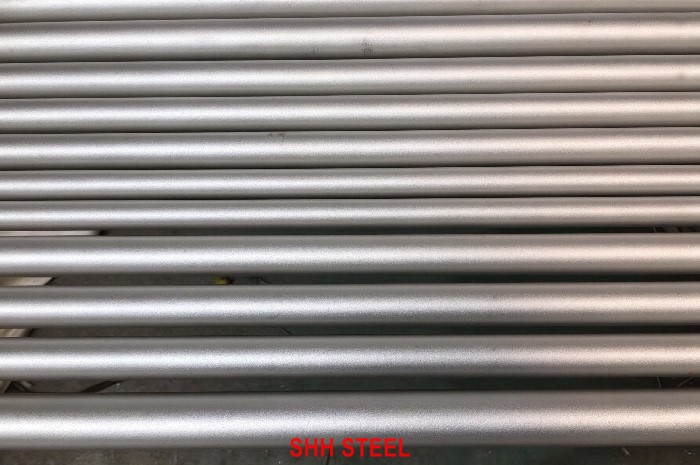
Standard mill delivery for ASTM A213 TP321 is solution annealed and pickled, leaving a clean matte finish suitable for most boiler and heat-exchanger tube duty. Bright annealing under protective atmosphere produces a smoother reflective surface used on some clean-process and instrumentation tube lines and must be called out because it changes the heat-treatment route. Light polish or specified Ra on the bore or OD is a commercial or service-center operation on top of A213 product, not automatic with the grade stamp.
When a hygienic or fouling-sensitive exchanger specification quotes an Ra maximum on the bore, put it on the tube purchase order with its own acceptance language and sampling plan. SHH STEEL stencils grade and heat treatment as standard requirements; polish, special OD grind, and passivation after fabrication remain commercial extras unless the contract says otherwise. End preparation (plain, slightly beveled, or as needed for tube expanding) should be ordered together with finish so receiving inspection shares one acceptance language.
Inspection and Testing
Lot testing for ASTM A213 TP321 follows tension, hardness, flattening, and flaring under A213 / A1016. Chemistry verification must include titanium against the 5 × (C + N) formula with the 0.70% ceiling, chromium 17.0–19.0%, and nickel 9.0–12.0%. Tensile reporting must use the Table 4 75/30 ksi pair and 35% elongation. NDE follows the ordered edition — hydrostatic testing or non-destructive electric testing of each length is the usual A213 path unless the purchase order states otherwise.
EN 10204 3.1 certificates from SHH STEEL report ladle chemistry with Ti, Table 4 tensile / yield / 35% elongation / hardness, and heat-treatment condition. When S2 stabilization, S1 stress relief, or S4 / A262 Practice E is ordered, those results appear as specified. Dual A213/SA-213 marking and third-party witness are available when written into the enquiry. A certificate missing titanium is not a complete TP321 release package.
Packaging and Shipping
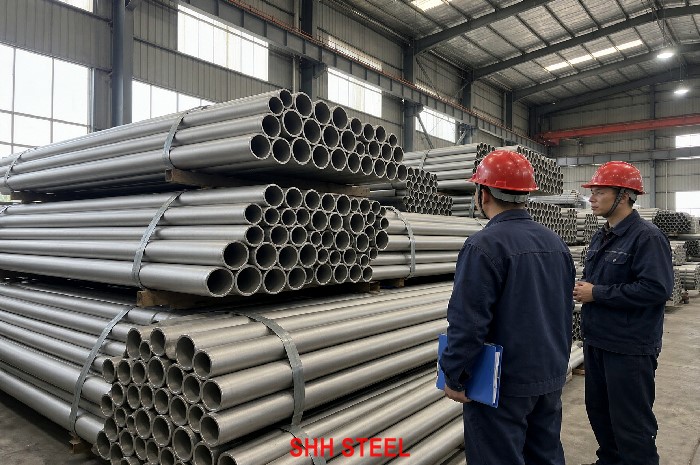
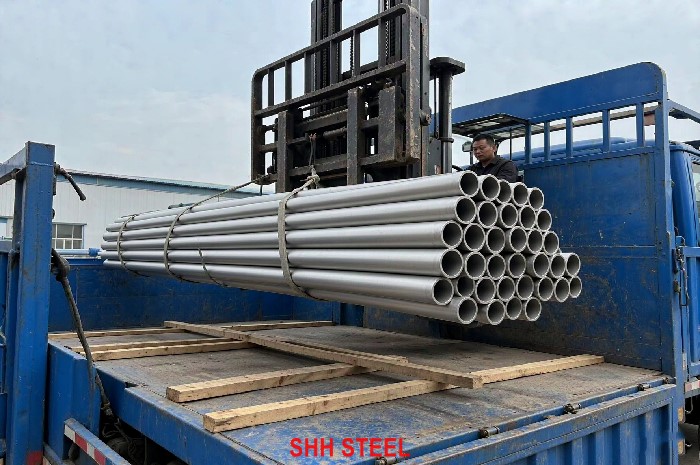
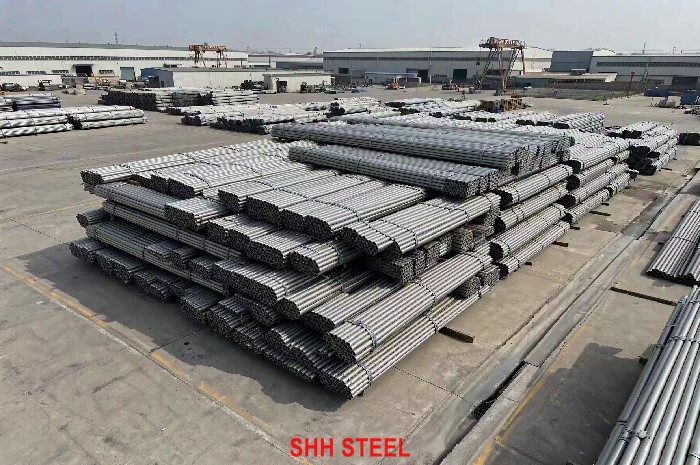
TP321 tubes ship in capped or plugged bundles with weather protection matched to the route. Cut lengths for boiler and exchanger bundles are labeled by heat and size; export packing uses cases or steel-frame crates when required.
Marking includes ASTM A213, grade TP321 / UNS S32100, size, heat number, and SHH STEEL identification. Dual SA-213 marking appears only when the purchase order requests it. Packing lists track the same heat numbers shown on the EN 10204 3.1 certificates so the titanium formula result stays tied to the shipped lengths.
Why Choose SHH STEEL
SHH STEEL treats ASTM A213 TP321 as a titanium-stabilized specification product: C ≤0.08%, Cr 17–19%, Ni 9–12%, Ti ≥5 × (C + N) ≤0.70%, Table 4 75/30 ksi, and elongation 35% minimum are checked together before a heat is offered. Quotations state OD × wall / BWG, wall basis, finish route, S1/S2/S4 options, and whether dual A213/SA-213 marking is required.
We refuse nickname assemblies that stamp TP304 as 321 without clearing the titanium formula, or that claim Mo pitting performance from a grade with no Mo requirement. EN 10204 3.1 documentation includes Ti against C + N. Compare sisters on the A213/A213M hub before freezing the exchanger tube list.
Supply Capability
SHH STEEL supplies ASTM A213 TP321 seamless stainless steel tube in cold-finished and hot-finished routes across the usual boiler, superheater, and heat-exchanger OD × wall / BWG band. Capability below is an enquiry range — not a frozen warehouse SKU or tonnage claim.
| Capability | SHH STEEL practice for TP321 |
|---|---|
| Product form | Seamless cold-finished and hot-finished tube |
| Standards | ASTM A213 / A213M; dual SA-213 when PO asks |
| Size band | Typical within ~1/8 in. ID to 5 in. OD; other diameters by agreement |
| Wall basis | Minimum wall or average wall as specified |
| Documentation | EN 10204 3.1 MTC with Ti ≥5×(C+N); S1/S2/S4 / A262 / third-party witness on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
Stock / Available sizes
SHH STEEL quotes TP321 against a stock-and-mill enquiry range rather than a frozen SKU/tonnage list. Representative OD × wall / BWG combinations for boiler and heat-exchanger tube appear below.
| Item | Typical stock / enquiry range for TP321 |
|---|---|
| Outside diameter | 12.7, 19.05, 25.4, 31.8, 38.1, 50.8, 63.5, 76.2 mm (and other boiler/HX ODs on enquiry; through the usual A213 ~5 in. [127 mm] band) |
| Wall / BWG | BWG 10–20 class walls and metric min-wall equivalents; heavier walls by agreement |
| Common OD × wall examples | 19.05 × 2.11 mm; 25.4 × 2.11 mm; 25.4 × 2.77 mm; 31.8 × 2.77 mm; 38.1 × 2.77 mm; 50.8 × 2.77 mm — illustrative, confirm min vs average wall |
| Length | Cut lengths for boiler / exchanger bundles; bends and random mill lengths on enquiry |
| Special | Non-standard OD/wall, bright anneal, dual A213/SA-213, S1 stress relief, S2 stabilization, S4 / A262 Practice E, third-party witness — confirm before heat reservation |
Send OD × wall (or BWG), wall basis, finish route, quantity or cut list, marking (A213 or dual A213/SA-213), and Ti / S1 / S2 / S4 notes on one enquiry. We confirm C ≤0.08%, Cr 17–19% / Ni 9–12%, Ti ≥5 × (C + N) ≤0.70%, Table 4 75/30 ksi, and elongation 35% minimum without inventing fake warehouse codes. Sisters A213 TP321H, A213 TP347, and A213 TP316Ti sit on the same hub.
FAQ
-
Is ASTM A213 the same as ASME SA-213 for TP321?
- No. ASTM A213 / A213M is the ASTM International product specification for seamless boiler, superheater, and heat-exchanger tubes; ASME SA-213 / SA-213M is the separate ASME Code Book adoption. Dual-mark only when the purchase order asks for both names on the stencil and MTC. Chemistry and tensile floors align closely for a given referenced edition, but the standards remain independent documents.
-
Does ASTM A213 TP321 include welded or HCW tube?
- No. ASTM A213 covers seamless boiler, superheater, and heat-exchanger tubes only. There is no WLD or HCW manufacturing-type letter under A213. Cold-finished versus hot-finished describes the seamless process route and dimensional tolerances — not a welded product form. Order welded stainless pipe under a different product standard when that form is required.
-
What is the chemistry of ASTM A213 TP321?
- Melting analysis for TP321 / UNS S32100 is C ≤0.08%, Mn ≤2.00%, P ≤0.045%, S ≤0.030%, Si ≤1.00%, Cr 17.0–19.0%, Ni 9.0–12.0%, and Ti ≥5 × (C + N) ≤0.70%, with molybdenum as a no-requirement ellipsis. Nitrogen has no standalone requirement but must be known for the titanium formula. Confirm the ordered A213 edition.
-
TP321 vs TP304L — when do I need titanium instead of low carbon?
- Order TP304L when the specification wants C ≤0.035% (or Footnote D 0.040% on small-OD / light-wall) without a titanium formula and accepts the 70/25 ksi tensile floor. Order TP321 when titanium stabilization with C ≤0.08% and the 75/30 ksi floor is named. They are different IGC strategies — do not treat "321" as a synonym stamp for 304L on the MTC.
-
TP321 vs TP316Ti — why choose one over the other?
- Both use a Ti ≥5 × (C + N) ≤0.70% formula and Table 4 75/30 ksi. TP316Ti adds mandatory Mo 2.00–3.00%, tighter Si ≤0.75%, and N ≤0.10%, with Cr 16–18 / Ni 10–14. TP321 has no Mo requirement and uses Cr 17–19 / Ni 9–12. Order TP316Ti when chloride pitting plus Ti stabilization are both required; stay on TP321 when Mo is not justified.
-
TP321 vs TP321H — when do I need the H grade?
- Order TP321H when the boiler or superheater datasheet needs the H-grade carbon range (0.04–0.10%), the Ti 4 × (C + N) ≤0.70% rule, and grain-size / creep-rupture framing that the H designation carries under A213. Standard TP321 remains appropriate for many moderate-temperature HX and stabilized general corrosive tube duties. Do not treat "321H" as a synonym stamp for ordinary TP321 on the MTC.
-
What do Footnotes F and H mean for TP321 heat treatment?
- Footnote F ties the water quench or rapid cool to A262 Practice E capability when that test is ordered (S4). Footnote H warns that solution treating above 1950 °F [1065 °C] may impair IGC resistance after later sensitizing exposure, and allows a purchaser-specified lower-temperature stabilization or resolution anneal after the higher solution anneal. Confirm the footnote text on the ordered edition.
-
What is Supplementary Requirement S2 for TP321?
- S2 requires a stabilization heat treatment at a temperature lower than the initial solution anneal for listed grades including TP321, when the purchaser specifies S2. Temperature is as agreed between purchaser and vendor. S2 is not automatic with the grade stamp — write it onto the purchase order when stabilization after solution anneal is contractual, especially when S4 / A262 Practice E must also be cleared.
-
Does Table 4 set a hardness limit for TP321?
- Yes. Table 4 lists hardness maximum 192 HBW / 200 HV or 90 HRB with 75 ksi tensile, 30 ksi yield, and 35% elongation. Hardness, titanium formula, and Cr–Ni band all belong on the release package — none replaces the others for 321 boiler or HX tube.
-
Minimum wall vs average wall for A213 TP321 — which should I specify?
- Boiler and heat-exchanger datasheets almost always expect minimum wall. Average wall is allowed when the purchase order says so, with A1016/A1016M tolerances for that basis. State wall basis on the enquiry rather than relying on pipe schedule numbers as the primary A213 wall story.
-
Can I dual-certify TP321 with TP304 on the same heat?
- Only when titanium clears the 5 × (C + N) ≤0.70% formula and every overlapping TP304 limit is also met — most TP304 heats have no intentional titanium addition and will fail the TP321 formula. Ask for dual marking on the purchase order rather than assuming it from a PMI gun that only reads "18-8."
-
Is TP321 a good choice for chloride-rich cooling water?
- Usually not as the first choice. TP321 has no molybdenum requirement, so chloride pitting and crevice performance stay in the plain 18Cr-Ni family. For chloride-leaning condensers and cooling-water exchangers, many owners move to A213 TP316 / TP316L or TP316Ti. Keep TP321 for Ti-stabilized duty where Mo is not justified by the fluid.
Conclusion
ASTM A213 TP321 / UNS S32100 is the titanium-stabilized seamless stainless steel tube for boiler, superheater, and heat-exchanger service when Ti ≥5 × (C + N) ≤0.70% with Cr 17–19% / Ni 9–12% and C ≤0.08% must deliver IGC resistance without an L-grade carbon mandate or a molybdenum addition. SHH STEEL supplies cold-finished and hot-finished seamless tube in the usual OD × wall / BWG band, solution annealed at 1900 °F [1040 °C] (Footnotes F, H), tested to Table 4 75/30 ksi, 35% elongation, and hardness limits, with titanium reported on EN 10204 3.1 certificates — dual SA-213 marking only when the purchase order asks.
Contact: admin@steelspecs.com
Quality Steel Needed? Inquire for Offers
Related Products