ASME SA312 TP304H Stainless Steel Pipe | SA 312/SA 312M
What is ASME SA312 TP304H Stainless Steel Pipe
ASME SA-312/SA-312M covers seamless, welded, and heavily cold-worked austenitic stainless steel pipe for high-temperature and general corrosive service, and it is the ASME Code adoption of ASTM A312/A312M. TP304H / UNS S30409 is the high-temperature version of ASME SA312 TP304 Stainless Steel Pipe. Clause 1.2 groups it with the other H grades (TP309H, TP309HCb, TP310H, TP310HCb, TP316H, TP321H, TP347H, and TP348H) as modifications intended for service where creep and stress-rupture properties matter, and that is really the only reason to buy it.
Table 1 sets C 0.04–0.10%, Mn ≤2.00%, P ≤0.045%, S ≤0.030%, Si ≤1.00%, Cr 18.0–20.0%, and Ni 8.0–11.0%, with no molybdenum or nitrogen requirement. The carbon minimum is the point of the grade: plain TP304 has no minimum and a modern heat may run at 0.02–0.03%, which is fine at ambient temperature but gives away creep strength. On top of chemistry, Table 5 requires an ASTM grain size of No. 7 or coarser, Table 2 lists a 1900 °F [1040 °C] minimum anneal for both cold- and hot-finished pipe, clause 6.2 requires reheating rather than quenching from the hot-working heat, and clause 17 requires heat-treatment lot marking. Table 4 sets 75 ksi [515 MPa] tensile and 30 ksi [205 MPa] yield, and Table 6 lists ER308.
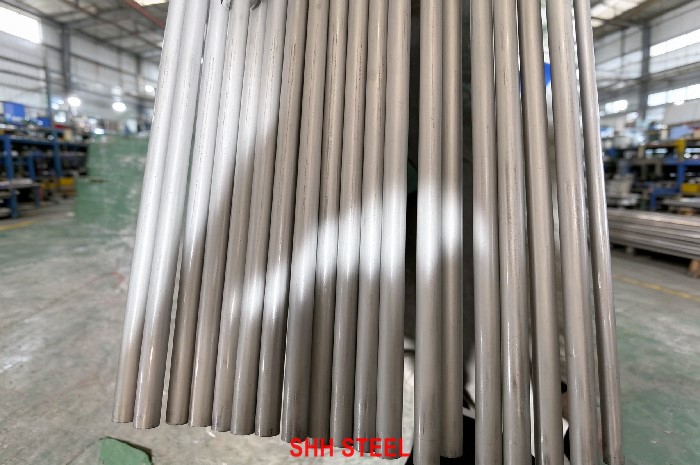
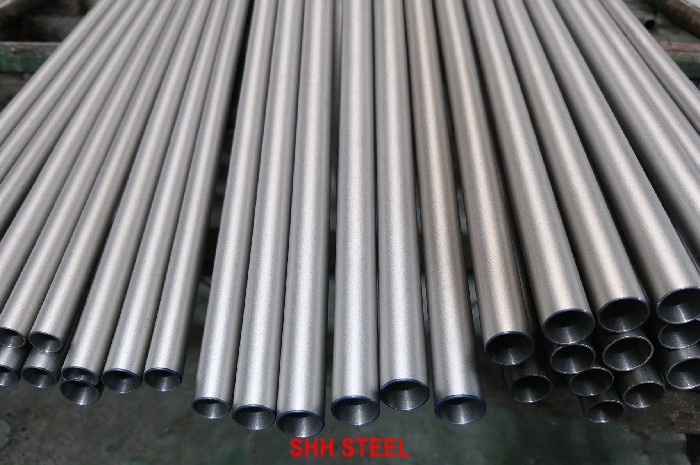
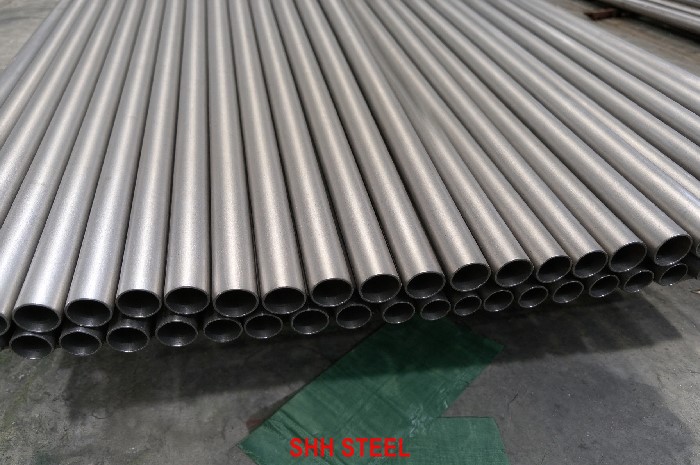
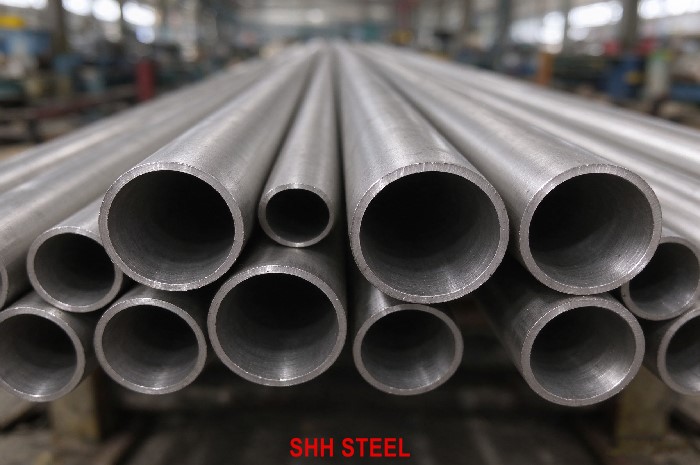
SHH STEEL can supply ASME SA312 TP304H stainless steel pipe to the edition named on the enquiry, in seamless (SML), welded (WLD), and heavily cold-worked (HCW) form. We quote ASME B36.19 schedules and special OD/wall by agreement, ship with EN 10204 3.1 mill test certificates reporting carbon inside the 0.04–0.10% band, the grain size per heat-treatment lot, the 75/30 ksi results, and the anneal and reheat statements, and offer dual SA-312/A312 and dual TP304/TP304H marking when the heat qualifies. Please confirm NPS, wall or schedule, design temperature, finish, and any supplementary tests when you enquire.
The names below are the ones buyers commonly use, and they map to the ordered product as shown. Always put both the TP name and the UNS number on the order, because the H requirements are invisible on the pipe surface and only the paperwork proves them.
- ASME SA312 TP304H / UNS S30409 — preferred marking language for ASME-code and dual-marked pipe
- ASTM A312 TP304H — same grade tables when the ASTM edition is referenced
- “304H” — common shorthand; acceptable in conversation, but the certificate must show the carbon band and grain size
- EN 1.4948 / JIS SUS304HTP — commonly cited high-temperature equivalents, approximate only
Sister grades buyers compare with TP304H include ASME SA312 TP304 Stainless Steel Pipe (C ≤0.08% with no minimum and no H rules), ASME SA312 TP304L Stainless Steel Pipe (low carbon, unsuitable for creep design), ASME SA312 TP316H Stainless Steel Pipe when molybdenum is wanted, and stabilized ASME SA312 TP347H Stainless Steel Pipe. Grade hub: ASME SA 312/SA 312M.
Manufacturing Types (SML / WLD / HCW)
ASME SA-312 recognizes three manufacturing routes for TP304H pipe, and the route is a purchase-order decision driven by the design code, the size range, wall thickness, and how the owner wants the pipe inspected. The route never changes the chemistry: whichever way the pipe is made, the heat must still meet C 0.04–0.10%, Mn ≤2.00%, P ≤0.045%, S ≤0.030%, Si ≤1.00%, Cr 18.0–20.0%, and Ni 8.0–11.0%, and every length must still go through the solution anneal at 1900 °F [1040 °C] minimum before it is released.
- Seamless (SML) — no welding at any stage. Seamless dominates superheater and reheater headers, high-pressure steam lines, and thick-wall heater piping. Hot-finished seamless must receive a separate solution treatment by reheating under clause 6.2, not a quench from the hot-working heat.
- Welded (WLD) — automatic welding without filler metal, with the weld finished so the pipe meets dimensional and mechanical requirements after the final heat treatment. The strip or plate heat must itself carry the full TP304H chemistry, so ask for the coil or plate heat number on the certificate.
- Heavily cold-worked (HCW) — welded pipe cold worked to at least 35% reduction of wall and weld before the final anneal, again without filler in the longitudinal seam, with the weld radiographed before cold work. Order HCW when the project specifically wants that marking and the process controls SA-312 writes around it.
Every finished length is hydrostatically tested or nondestructively electrically tested, and the mill may choose the method unless the purchase order fixes one. Pipe NPS 10 and larger may ship marked “NH” only when the purchaser accepts a system test in place of the hydrotest, and lots for mechanical testing follow clause 11.1. Because TP304H is an H grade, clause 17 requires heat-treatment lot marking in addition to the heat number, and clause 11.4 requires the E112 grain-size determination per heat-treatment lot. Dual TP304/TP304H marking is common when the heat carbon sits at 0.04–0.08% and the grain-size and reheat requirements are met.
TP304H is produced regularly for power and refinery work, but not every stockist carries genuine H-grade material with grain-size reporting, so check the certificate before accepting stock offered as “304H”. Heavy-wall seamless and special sizes are mill-run items; tell us the route, sizes, wall, edition year, and whether dual TP304/TP304H is wanted so carbon and grain size can be targeted from the start.
Chemical Composition of SA312 TP304H
Two chemistry layers matter for TP304H. The melting (heat or ladle) analysis is mandatory for every heat under SA-312/A312 Table 1, while product analysis on finished pipe applies only when it is ordered through Supplementary Requirement S1 or purchase-order wording. Product tolerances are not printed in SA-312 itself; they come through ASTM A999/A999M §6.3 from ASTM A480/A480M Table A1.1. SHH STEEL reports the actual ladle values and, when ordered, the product values, and never quotes tighter catalogue windows that the standard does not publish.
The tables below reproduce the Table 1 heat analysis for TP304H and the product-analysis limits that result from applying the A480 Table A1.1 tolerances. Values are maximum unless a range is shown, and an ellipsis (…) means the ordered edition sets no requirement for that element, so it need not be determined or reported on the certificate.
Melting analysis (heat / ladle analysis) — Table 1
| Element | TP304H (UNS S30409) melting analysis |
|---|---|
| Carbon (C) | 0.04 – 0.10 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 18.0 – 20.0 |
| Nickel (Ni) | 8.0 – 11.0 |
| Nitrogen (N) | … (no requirement) |
| Molybdenum (Mo) | … (no requirement) |
Product analysis — A480/A480M Table A1.1 tolerances applied to Table 1
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | 0.04 – 0.10 | 0.01 under / over | 0.03 – 0.11 |
| Manganese (Mn) | ≤ 2.00 | 0.04 over | ≤ 2.04 |
| Phosphorus (P) | ≤ 0.045 | 0.010 over | ≤ 0.055 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 18.0 – 20.0 | 0.20 under / over | 17.80 – 20.20 |
| Nickel (Ni) | 8.0 – 11.0 | 0.10 under / 0.15 over | 7.90 – 11.15 |
| Element | TP304L (S30403) | TP304 (S30400) | TP304H (S30409) |
|---|---|---|---|
| C | ≤ 0.035 | ≤ 0.08 | 0.04 – 0.10 |
| Mn | ≤ 2.00 | ≤ 2.00 | ≤ 2.00 |
| Cr | 18.0 – 20.0 | 18.0 – 20.0 | 18.0 – 20.0 |
| Ni | 8.0 – 13.0 | 8.0 – 11.0 | 8.0 – 11.0 |
Carbon at 0.04–0.10% is the defining element and the first value to check on receipt. Chromium and nickel are identical to ASME SA312 TP304 Stainless Steel Pipe, so a handheld PMI gun reading Cr and Ni cannot tell TP304H from TP304 or TP304L; carbon has to come from the certified analysis or an OES test. If dual TP304/TP304H marking is ordered, the heat carbon must sit within 0.04–0.08% so it satisfies both rows, while dual TP304L/TP304H is impossible because the carbon windows do not overlap.
On product analysis the finished pipe may read C 0.03–0.11%, Mn up to 2.04%, P 0.055%, S 0.035%, and Si 1.05%, with Cr 17.80–20.20% and Ni 7.90–11.15%. Note that the product tolerance applies to the minimum as well, so a product reading of 0.035% carbon is still acceptable under A480 even though the heat itself must be at 0.04% or above. State any tighter project carbon band on the purchase order before the heat is selected.
Mechanical Properties of SA312 TP304H
Room-temperature tensile requirements for TP304H come from SA-312 Table 4 and are summarized below. These are minimum release values for the lot, not typical values, and design allowables must always be taken from the governing code tables for UNS S30409 rather than from a neighbouring grade.
| Property (SA-312 Table 4) | TP304H |
|---|---|
| Tensile strength, min | 75 ksi [515 MPa] |
| Yield strength (0.2% offset), min | 30 ksi [205 MPa] |
| Elongation in 2 in. or 50 mm (or 4D), min | 35% longitudinal / 25% transverse |
| Grain size (Table 5) | ASTM No. 7 or coarser |
| Hardness | No maximum in Table 4 |
The room-temperature floors of 75/30 ksi are identical to ASME SA312 TP304 Stainless Steel Pipe, which is why the H requirements are easy to overlook. The real difference is in the elevated-temperature allowable stresses that the ASME Code gives UNS S30409, which depend on guaranteed carbon and coarse grain; a fine-grained, low-carbon heat can pass every room-temperature test and still be wrong for creep design. Table 4 lists no hardness maximum for TP304H.
Design in the creep range must use the code allowables listed for S30409, not TP304 or TP304L values, and the grain-size result per heat-treatment lot must accompany the tensile results on the MTC. A result finer than No. 7 fails the grade regardless of how good the chemistry or tensile performance looks.
Dimensions and Tolerances
Dimensional supply for SA312 TP304H pipe follows ASME B36.19 schedules for the common NPS and schedule combinations, with special OD and wall available by agreement when a project needs a section the schedules do not cover. Outside-diameter variations follow ASTM A999/A999M, and wall-thickness variations follow SA-312 Table 3 as summarized below. State on the purchase order whether wall is nominal or minimum (Supplementary S8), because the two readings produce different pipe from the same size line.
| NPS designator | Over | Under |
|---|---|---|
| 1/8 – 2-1/2, all t/D | 20.0% | 12.5% |
| 3 – 18, t/D ≤ 5% | 22.5% | 12.5% |
| 3 – 18, t/D > 5% | 15.0% | 12.5% |
| ≥ 20 welded | 17.5% | 12.5% |
| ≥ 20 seamless, t/D ≤ 5% | 22.5% | 12.5% |
| ≥ 20 seamless, t/D > 5% | 15.0% | 12.5% |
Source: SA-312 Table 3; outside diameter variations per A999/A999M.
- Lengths — single random, double random, or cut-to-length on order
- Cut lengths — typically no more than 1/4 in. [6 mm] over the ordered length unless the PO states a tighter band
- Ends — plain or beveled; confirm bevel angle and root face when the WPS is already frozen
Many power, refinery, and petrochemical buyers order by OD × wall rather than NPS and schedule, which is fine as long as the enquiry says so clearly. Straightness, end finish, and length tolerance should be written into export orders so receiving inspection has an agreed acceptance basis instead of arguing after arrival. On thin schedules with threaded or socket-weld ends, check that the remaining wall is still adequate after the 12.5% under-tolerance. Jointers are not permitted unless the purchase order allows them, so cut-to-length programmes should include an allowance for fit-up scrap rather than expecting the mill to ship short pieces.
Equivalent Grades
TP304H / UNS S30409 has commonly cited high-temperature equivalents in European and Japanese standards. Any cross-reference has to be checked against carbon range, grain size, and heat treatment, not just chromium and nickel, before it is used in a materials discussion.
| Designation | Relationship |
|---|---|
| ASME SA-312 / ASTM A312 TP304H | Governing pipe grade |
| UNS S30409 | Unified number in Table 1 |
| ASME SA-213 TP304H | Same grade designation for boiler and heat-exchanger tubes (separate specification) |
| ASME SA-240 304H | Plate for fabricated components (separate specification) |
| EN 1.4948 (X6CrNi18-10) | Commonly cited European heat-resisting counterpart; chemistry and creep data differ—review before substitution |
| JIS SUS304HTP | Commonly cited Japanese pipe counterpart; verify against JIS G3459 or G3463 |
EN 1.4948 and JIS SUS304HTP are commonly cited equivalents but were not verified against the EN or JIS texts for this page, so treat them as approximate; they do not authorize code substitution. Dual TP304/TP304H certification is valid only when carbon is 0.04–0.08% and the grain-size and reheat rules are met. Related SA-312 pages: ASME SA312 TP304 Stainless Steel Pipe, ASME SA312 TP316H Stainless Steel Pipe, and ASME SA312 TP347H Stainless Steel Pipe.
Heat Treatment and Delivery Condition
Table 2 lists TP304H at 1900 °F [1040 °C] minimum for both cold-finished and hot-finished pipe, followed by rapid cooling. Clause 6.2 of the ASME edition requires H grades to be reheated to the solution temperature before quenching, so a direct quench from the hot-working heat, which is allowed for some non-H grades, is not acceptable for TP304H. The anneal is what develops the coarse grain needed for Table 5, so the anneal record and the grain-size result belong together on the certificate.
Clause 17 requires the heat-treatment lot to be marked alongside the heat number, so each length can be traced to the anneal that produced its grain size. Bright annealing is possible by agreement where the mill can hold temperature in a protective atmosphere. If pipe is hot bent or formed later, a fresh solution anneal is needed to restore the structure, and any post-weld heat treatment for creep service should be specified by the owner rather than improvised in the field.
Corrosion Resistance
SA-312 has no corrosion table, so this section is engineering commentary rather than a specification requirement. At ambient temperature TP304H resists general corrosion much like TP304, but its higher carbon makes it more prone to sensitization if it spends time roughly in the 800–1500 °F range, which is exactly where many H-grade lines operate. TP304H is therefore a high-temperature strength grade, not a wet-corrosion grade.
- High-temperature oxidation — good in air and steam at typical 304H service temperatures (general guidance, around 1600 °F in air)
- Sigma phase — long service roughly in the 1100–1650 °F range can embrittle the structure in very long-life designs
- Polythionic acid cracking — a known refinery shutdown concern for sensitized H grades; follow the owner’s neutralization practice
- Intergranular corrosion — higher risk than TP304L; S7 (A262 Practice E) can be ordered when proof is needed
Where the line sees creep-range temperatures and wet corrosive conditions during shutdowns, discuss stabilized options such as ASME SA312 TP347H Stainless Steel Pipe with the materials engineer. Do not swap TP304H for TP304L to gain corrosion resistance in creep service, because the low-carbon grade loses the elevated-temperature allowables that the design relies on, and the pipe could end up overstressed at temperature.
Applications of SA312 TP304H Pipe
Applications for TP304H pipe are driven by elevated design temperature, typically in the creep range above roughly 1000 °F [540 °C] as general guidance, with the governing code making the final call. The table below summarizes where buyers typically specify the grade.
| Sector | Typical TP304H use | Why the H grade |
|---|---|---|
| Power generation | Superheater and reheater headers, main steam and hot reheat links | Higher code allowables in the creep range |
| Refining | Heater outlet piping, transfer lines, hydrogen units | Creep strength; often with polythionic acid precautions |
| Petrochemical | Cracking furnace and high-temperature process lines | Strength and oxidation resistance |
| Heat recovery and HRSG | High-temperature sections of recovery systems | Coarse grain for creep resistance |
| Industrial furnaces | Hot gas ducting and radiant section piping | Oxidation resistance |
| Dual-use plants | Lines that run hot but also see cleaning cycles | Dual 304/304H certification gives flexibility |
Typical users include utility and industrial boilers (superheater and reheater headers and links), refinery heater and transfer piping, petrochemical furnaces, and hot gas lines. Enquiries should state the design temperature and code, whether dual TP304/TP304H marking is required, the grain-size reporting basis, and any PWHT or bending plans, so the mill can plan the heat treatment correctly. For molybdenum-bearing creep service see ASME SA312 TP316H Stainless Steel Pipe.
Weldability
SA-312 Table 6 lists ER308 (given in the pack source as S30880 / W30840) as the filler for TP304H. Many fabricators specify ER308H on creep-range welds so the deposit carbon matches the base metal, but that is a fabrication preference rather than an SA-312 requirement, and the final choice should be fixed on the WPS and PQR. Low-carbon ER308L is generally avoided in creep-range joints because the weld would be weaker than the pipe at temperature.
- Qualify on TP304H — procedure qualification on the actual H grade
- Control heat input and interpass temperature — to limit sensitization in the HAZ
- Back-purge roots — to protect the ID from oxidation
- Post-weld heat treatment — only when the owner specifies it, to the agreed cycle
Mill longitudinal welds on WLD and HCW pipe are made without filler, so Table 6 applies to repairs and fabrication joints. Weld strength reduction factors for creep-range welded pipe come from the B31 piping codes, not from SA-312, so check them before choosing welded over seamless for hot lines. Girth-weld NDE extent is a fabrication-code decision separate from the mill test on each length.
Surface Finishes
Surface condition for SA312 TP304H pipe should be stated on the purchase order rather than left to mill default. For stainless pipe, embedded free iron, residual scale, and chloride-bearing residues are where corrosion starts, so the finish is part of the material performance and not just appearance. The finishes we regularly quote for this grade are listed below.
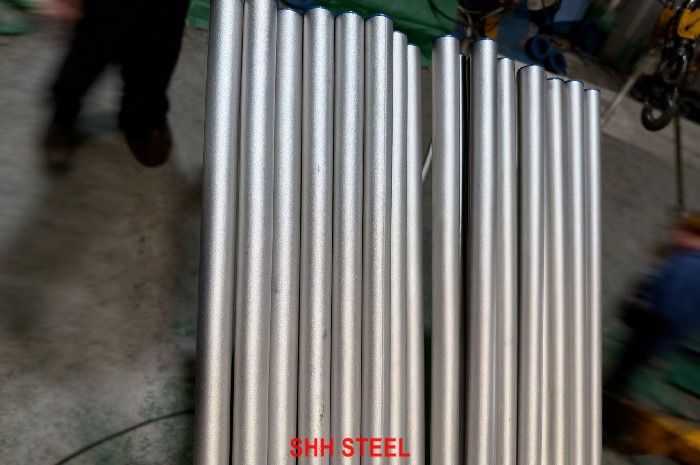
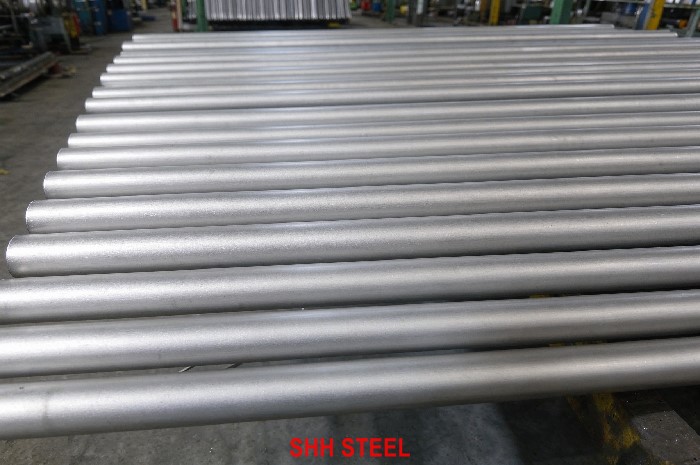
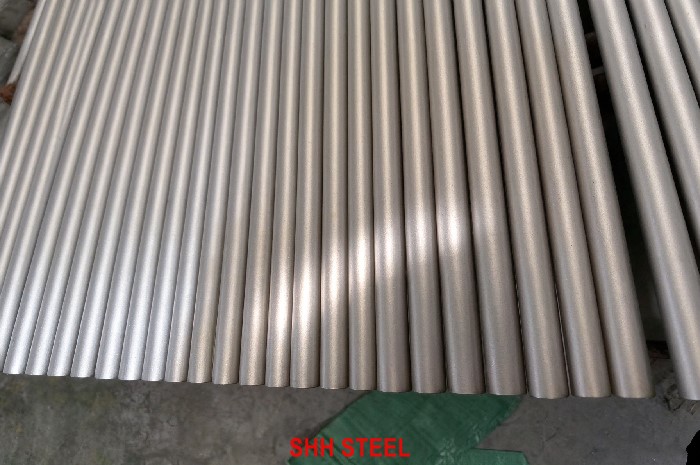
- Annealed and pickled (AP) — solution annealed at 1900 °F [1040 °C] minimum, then descaled in acid pickle or an equivalent process to a matte grey finish; the standard choice for process pipe
- Blasted and pickled — common on heavy-wall seamless where blasting first makes scale removal more reliable
- Bright annealed (BA) — annealed in a protective atmosphere where mill capability exists for the size; the anneal temperature still has to meet the Table 2 practice for TP304H
- Mechanically polished — OD and/or ID polish to an agreed grit or Ra when ordered; polishing never replaces the solution anneal
- Bead-finished welded OD — weld bead rolled or ground flush as agreed on WLD and HCW product
For TP304H the usual choice is annealed and pickled, because the pipe is bought for high-temperature service where a clean, scale-free surface matters far more than appearance. Passivation after pickling or polishing can be added when the end-user specification calls for it, even though SA-312 itself does not require it. If the project bans chloride-bearing marking inks, say so on the order; otherwise the mill will apply its normal stencil practice and ship its default AP finish.
Inspection and Testing
The base acceptance package for SA-312 TP304H pipe combines chemistry, tensile testing, heat-treatment evidence, and a pressure or electrical integrity test on every length. The items below make up the usual package; supplementary requirements and project corrosion tests only apply when they are written on the purchase order.
- Heat (melting) analysis — mandatory per heat against Table 1 for TP304H: C 0.04–0.10%, Mn ≤2.00%, P ≤0.045%, S ≤0.030%, Si ≤1.00%, Cr 18.0–20.0%, and Ni 8.0–11.0%
- Product analysis — when ordered (Suppl. S1 or PO wording), using A480 Table A1.1 tolerances via A999 §6.3
- Tension test — 75 ksi [515 MPa] tensile and 30 ksi [205 MPa] yield minimum, plus 35% L / 25% T elongation, with Table 5 grain size No. 7 or coarser on a lot basis
- Flattening test — or the alternate bend test where the standard permits
- Hydrostatic or nondestructive electric test — every length; manufacturer’s option unless the order fixes the method
- Visual and dimensional check — against ordered NPS/schedule or OD × wall, with TP304H (UNS S30409) and the heat-treatment lot on every stencil
Mill test certificates: EN 10204 3.1 is the standard documentation from SHH STEEL supply. For TP304H the certificate must report the full Table 1 chemistry with carbon inside 0.04–0.10%, the Table 5 grain size per heat-treatment lot, the 75/30 ksi results with 35%/25% elongation, the hydro or NDE method, the 1900 °F anneal, the clause 6.2 reheat, and the heat-treatment lot identity. EN 10204 3.2 or third-party witness by SGS, Bureau Veritas, TÜV, or the buyer’s nominated agency is arranged when specified, and it should be booked before final testing rather than after the heat has been released. Dual ASME SA-312 / ASTM A312 certification is available when chemistry, heat treatment, mechanical tests, and marking satisfy both editions named on the order.
| Option | Purpose |
|---|---|
| S1 product analysis | Confirms chemistry on finished pipe |
| S5 radiography | Weld integrity on WLD pipe |
| S7 intergranular corrosion | A262 Practice E after sensitizing treatment |
| S8 minimum wall | Wall interpreted as minimum rather than nominal |
| S9 weld decay | Compares weld and base-metal loss rates |
Receiving review should confirm carbon 0.04–0.10% (or 0.04–0.08% for dual TP304/TP304H), Cr and Ni, grain size No. 7 or coarser, the 75/30 ksi results, the anneal and reheat statements, and the heat-treatment lot marking. Third-party inspectors should check that the stencil reads TP304H and not only TP304, and remember that PMI guns cannot separate TP304H from TP304L.
Packaging and Shipping
Export and domestic shipments of SA312 TP304H pipe are packed for handling and for ocean or land transport. The packing we normally apply is summarized below, and anything beyond it can be agreed on the order.
- Seaworthy bundles — pipes strapped or cradled in bundles sized for container or break-bulk handling, with non-metallic separators where the finish needs protecting
- End caps — plastic or metal caps on plain or beveled ends to keep out damage and contamination in transit
- Marking — specification, grade (TP304H (UNS S30409) and the heat-treatment lot), heat number, size, manufacturing type (SML / WLD / HCW), test letters, and mill identity as SA-312 and the purchase order require
- Export protection — waterproof wrapping or desiccant as agreed for polished or bright-annealed finishes, with low-chloride inks on request
Segregate TP304H from ASME SA312 TP304 Stainless Steel Pipe and ASME SA312 TP304L Stainless Steel Pipe on the packing list and in the yard, because these grades look identical and carbon cannot be checked with a handheld PMI gun. Use separate bundles and distinct tags on mixed shipments, and have receiving check heat and lot numbers against the MTC for every length. Keep interiors dry and capped so chloride-bearing moisture cannot stain or pit the surface before installation. Shipping documents normally include the packing list, invoice, bill of lading or air waybill, and the 3.1 or 3.2 MTC with full Table 1 chemistry, plus origin and customs papers to suit the agreed Incoterms.
Why Choose SHH STEEL
SHH STEEL supplies specification-driven stainless plate and pipe, and for SA312 TP304H we quote against the edition you name rather than a generic catalogue sheet. We report the full Table 1 chemistry on the MTC with carbon shown inside the 0.04–0.10% band, together with the Table 5 grain size per heat-treatment lot, the 75/30 ksi results, and the 1900 °F anneal and clause 6.2 reheat statements. Heat identity stays unbroken from the melt to the finished length, so receiving inspection can clear each heat against Table 1 and Table 4 without chasing paperwork after the pipe has arrived.
We check supplier certificates before shipment for missing grain-size results, carbon below 0.04%, absent lot marking, and ordinary 304 stock relabelled as 304H, so problems are caught at the mill rather than at the fabricator. Where you need dual TP304/TP304H marking, we confirm before the order that the heat carbon will sit inside the 0.04–0.08% overlap.
- Specification fidelity — chemistry and tensile to SA-312/A312 Table 1 and Table 4 for TP304H; C 0.04–0.10% reported; Table 5 grain size No. 7 or coarser; 1900 °F anneal and clause 6.2 reheat stated; lot marking applied
- Mill resources — SML, WLD, and HCW from qualified stainless pipe mills with heat traceability; cutting and beveling on confirmed orders
- Documentation — EN 10204 3.1 MTCs as standard with full Table 1 chemistry; 3.2 or third-party inspection on request
- Dual marking — ASME SA-312 and ASTM A312 when the heat and tests meet both editions you name
- Related grades — ASME SA312 TP304 Stainless Steel Pipe, ASME SA312 TP316H Stainless Steel Pipe, ASME SA312 TP347H Stainless Steel Pipe, and ASME SA312 TP304L Stainless Steel Pipe when a project buys a matched package
- Export packing — seaworthy bundles, end protectors, and durable grade, heat, size, and type marking
Quotations follow your purchase-order language for edition year, manufacturing type, size, wall, finish, and any supplementary tests you name (S1, S5, S7, S8, S9). If the same project also needs plate or fittings, ask for coordinated heats so the chemistry lines up across product forms. Grade hub: ASME SA 312/SA 312M.
Supply Capability
SHH STEEL can supply ASME SA312 TP304H stainless steel pipe against the edition and manufacturing type named on your enquiry. The capability table below summarizes the routes, sizes, finishes, and documents we regularly quote for this grade.
| Item | SHH STEEL capability for TP304H |
|---|---|
| Standard | ASME SA-312/SA-312M and/or ASTM A312/A312M Grade TP304H / UNS S30409 |
| Manufacturing types | SML, WLD, HCW |
| Size | NPS 1/8 and up per ASME B36.19; special OD/wall by agreement |
| Schedules | 5S, 10S, 40S, 80S and non-standard walls |
| Length | SRL, DRL, or cut-to-length |
| Finish | Annealed and pickled; blasted and pickled; bright annealed or polished by agreement |
| Testing | Tension (75/30 ksi), Table 5 grain size No. 7 or coarser per heat-treatment lot, flattening/bend, hydro or NDE per length; C 0.04–0.10% on MTC; 1900 °F anneal and clause 6.2 reheat stated |
| Documents | EN 10204 3.1 with full Table 1 chemistry; third-party inspection / 3.2 on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
Common TP304H and dual TP304/TP304H sizes are sometimes available from stock, but check that the stock certificate shows the carbon band, grain size, and lot marking before accepting it. Heavy-wall seamless and special sizes are usually mill-order items. Enquiries should state the SA-312 edition, TP304H (UNS S30409) and the heat-treatment lot, SML/WLD/HCW, NPS or OD × wall (and whether wall is nominal or minimum), length practice, finish, and any product-analysis, corrosion-test, or 3.2 requirements, so mill slots line up with your need date. Cut lengths, beveling, and packing-list marking are available on confirmed orders, and grouping project sizes onto one heat keeps the chemistry consistent while helping meet mill minimums without over-ordering.
FAQ
-
Is ASME SA312 the same as ASTM A312 for TP304H?
- For chemistry (Table 1), tensile (Table 4), manufacturing types, heat treatment, and most testing language, ASME SA-312/SA-312M matches ASTM A312/A312M of the referenced edition. Dual SA312/A312 marking is common when it is ordered. Name both editions on the purchase order and make sure the mill test certificate repeats them, so inspectors can verify the heat against the books you cited.
-
Seamless vs welded TP304H — which is better?
- Neither is universally better. Seamless is the usual choice for heavy walls, high-pressure lines, and piping classes written around seamless product, while WLD and HCW are fully legitimate SA-312 forms when they are tested and annealed to the standard and usually cost less in common sizes. Choose the route your design code and datasheet allow, and check that SML, WLD, or HCW appears on both the stencil and the MTC.
-
Hydrostatic test vs NDE — which do I get on TP304H pipe?
- Every length is either hydrostatically tested or nondestructively electrically tested, and the manufacturer may choose unless the purchase order fixes the method. If your piping class or client specification requires one of them, state it on the PO and confirm the chosen test on the MTC for each length. NPS 10 and larger may be marked NH only when you accept a system test instead.
-
Does SA-312 Table 4 set a hardness limit for TP304H?
- No. Table 4 lists tensile strength, yield strength, and elongation for TP304H, but no hardness maximum, so catalogue Brinell or Rockwell figures are not specification requirements. If hardness matters for your fabrication or for an end-user rule, write the limit and the test method on the purchase order, and we will make sure the mill reports it on the certificate alongside the grain size.
-
What is the UNS number and chemistry of TP304H?
- Table 1 lists TP304H as UNS S30409 with C 0.04–0.10%, Mn ≤2.00%, P ≤0.045%, S ≤0.030%, Si ≤1.00%, Cr 18.0–20.0%, and Ni 8.0–11.0%, with no molybdenum or nitrogen requirement. Carbon is the defining element. Put both TP304H and S30409 on the purchase order, the stencil, and the certificate.
-
How does TP304H differ from TP304?
- TP304 allows C up to 0.08% with no minimum and has no grain-size or reheat rules. TP304H requires C 0.04–0.10%, Table 5 grain size No. 7 or coarser, the clause 6.2 reheat, and heat-treatment lot marking. Room-temperature tensile floors are the same 75/30 ksi; the difference shows up in creep-range allowable stresses.
-
Can TP304H pipe be dual certified TP304/TP304H?
- Yes, when the heat carbon sits in the 0.04–0.08% overlap and the H-grade grain-size, reheat, and lot-marking requirements are met. Dual TP304L/TP304H is impossible because the carbon windows do not overlap. Write the dual grade on the purchase order before the heat is allocated, so the mill can target carbon and grain size together.
-
What heat treatment does Table 2 require for TP304H?
- Table 2 lists TP304H at 1900 °F [1040 °C] minimum for both cold-finished and hot-finished pipe, followed by rapid cooling. ASME clause 6.2 requires H grades to be reheated to temperature before quenching, so a direct quench from the hot-working heat is not acceptable. The anneal and the grain-size result should appear together on the MTC.
-
Why does SA-312 control grain size on TP304H?
- Coarse grains improve creep and stress-rupture strength, which is the whole purpose of the H grade. Table 5 requires ASTM grain size No. 7 or coarser, determined to E112 per heat-treatment lot under clause 11.4. A result finer than No. 7 fails the grade even if chemistry and tensile pass, so ask for the grain-size result on the MTC.
-
What filler metal is listed for TP304H?
- SA-312 Table 6 lists ER308 for TP304H. Many fabricators specify ER308H on creep-range joints so the weld deposit carbon matches the pipe, which is a fabrication preference rather than an SA-312 rule. Avoid low-carbon ER308L in creep service. Mill seams on WLD and HCW pipe are autogenous, so Table 6 applies to repairs and site joints.
-
Is TP304H a good choice for wet corrosive service?
- Generally not. Its higher carbon makes it more prone to sensitization and intergranular attack than TP304L, especially after exposure in the 800–1500 °F range. TP304H is bought for elevated-temperature strength. For aqueous corrosive service choose TP304L or TP316L, and for hot lines that also see wet shutdown conditions discuss stabilized TP347H with your materials engineer.
Conclusion
ASME SA312 TP304H / UNS S30409 is the creep-service member of the 304 family, with C 0.04–0.10%, Cr 18.0–20.0%, and Ni 8.0–11.0% in Table 1, a 75/30 ksi Table 4 floor with 35% L / 25% T elongation, Table 5 grain size No. 7 or coarser, a 1900 °F [1040 °C] Table 2 anneal for cold- and hot-finished pipe, the clause 6.2 reheat, clause 17 lot marking, and ER308 filler from Table 6. It is not a drop-in for ASME SA312 TP304L Stainless Steel Pipe or plain ASME SA312 TP304 Stainless Steel Pipe in creep design. Order the manufacturing type, size and wall, finish, carbon and grain-size reporting, any dual TP304/TP304H marking, and supplementary tests explicitly. For stock checks, mill certificates, or dual SA-312/A312 supply questions, contact SHH STEEL at admin@steelspecs.com or browse the ASME SA 312/SA 312M category on steelspecs.com.
Quality Steel Needed? Inquire for Offers
Related Products