ASME SA312 UNS S30615 Stainless Steel Pipe | SA 312/SA 312M
What is ASME SA312 UNS S30615 Stainless Steel Pipe
ASME SA-312/SA-312M (identical in its grade tables to ASTM A312/A312M) covers seamless, welded, and heavily cold-worked austenitic stainless steel pipe for high-temperature and general corrosive service. UNS S30615 is listed in Table 1 with no TP designation, so it is ordered, stencilled, and certified by UNS number alone. Write it on the PO as “ASME SA-312/SA-312M [edition], UNS S30615”; a trade name or a “high-silicon 309-type” description is not enough, because S30615 has its own Table 1 row and must be certified to it.
The chemistry is built for hot gas, not for acid: carbon 0.16–0.24%, silicon 3.2–4.0%, aluminium 0.80–1.50%, chromium 17.0–19.5%, nickel 13.5–16.0%, with Mn ≤2.00%, P ≤0.030%, and S ≤0.03%. Table 4 sets 90 ksi [620 MPa] tensile and 40 ksi [275 MPa] yield minimum with 35% longitudinal / 25% transverse elongation—high for an austenitic heat-resisting grade. S30615 has no individual Table 2 row, so the general 1900 °F [1040 °C] minimum solution treatment applies. It is not listed in Table 6, so no filler class is named, and it is not an H grade. Buyers used to low-carbon stainless should note that a carbon reading of about 0.20% on an S30615 certificate is correct and necessary.
Each addition does a high-temperature job. Silicon and aluminium build an adherent oxide that slows carbon pickup and scaling in hot carburizing, oxidizing, and sulfur-bearing atmospheres; the high carbon gives elevated-temperature strength through stable carbides; and nickel keeps the matrix austenitic despite the large silicon and aluminium additions. That is why the grade turns up in heat-treatment furnace radiant tubes, muffles, retorts, furnace rolls, and petrochemical furnace parts, where it can outlast higher-chromium grades in carburizing service at a lower nickel content than 310-type alloys.
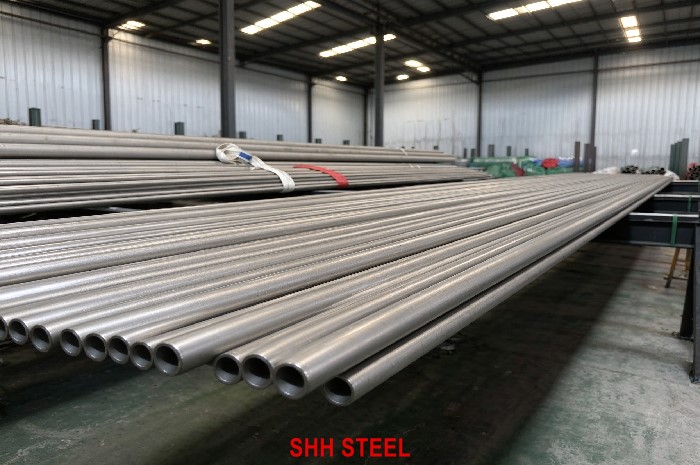
SHH STEEL can supply ASME SA312 UNS S30615 stainless steel pipe to the edition named on the enquiry, as seamless (SML), welded (WLD), or heavily cold-worked (HCW) pipe; in ASME B36.19 schedules or special OD × wall to the furnace builder’s drawing; with EN 10204 3.1 mill test certificates reporting the full Table 1 window, including carbon, silicon, and aluminium, and the solution-treatment temperature against the 1900 °F minimum; and with dual SA-312/A312 marking when heat, heat treatment, tests, and marking satisfy both editions on the order. Seamless is limited in this alloy, so we confirm the size range before quoting.
Names you may meet and how they map to the ordered product:
- ASME SA312 UNS S30615 / SA-312 S30615 — correct Code form; no TP name exists
- ASTM A312 UNS S30615 — ASTM parent with the same chemistry and tensile rows
- Producer trade names — the chemistry is sold under proprietary names; order and certify by UNS S30615
- EN / JIS — no one-to-one designation is asserted here
Do not confuse S30615 with the acid-service high-silicon grades ASME SA312 UNS S30600 Stainless Steel Pipe and ASME SA312 UNS S30601 Stainless Steel Pipe: their ultra-low carbon and S30615’s high carbon plus aluminium point to completely different services, and a mix-up either way would be a serious material error. For hot-gas duty where carburization is less severe, ASME SA312 UNS S30815 Stainless Steel Pipe or ASME SA312 UNS S30415 Stainless Steel Pipe may be easier to source, while ASME SA312 TP309S Stainless Steel Pipe and ASME SA312 TP310S Stainless Steel Pipe rely on chromium and nickel rather than silicon and aluminium and can still be preferred in purely oxidizing air at the very top of the temperature range. Family hub: ASME SA 312/SA 312M.
Manufacturing Types (SML / WLD / HCW)
ASME SA-312 recognizes three manufacturing routes for UNS S30615 pipe, and the route is a purchase-order decision driven by the design code, the size range, wall thickness, and how the owner wants the pipe inspected. The route never changes the chemistry: whichever way the pipe is made, the heat must still meet the Table 1 window of C 0.16–0.24%, Si 3.2–4.0%, Al 0.80–1.50%, Cr 17.0–19.5%, and Ni 13.5–16.0%, and every length must still go through the solution anneal at the general 1900 °F [1040 °C] minimum (no individual Table 2 row) before it is released.
- Seamless (SML) — no welding at any stage. Preferred for high-pressure service, thick walls, and owners who exclude welded pipe from the design class. Seamless S30615 is available in a limited size range; clause 6.2 permits direct quenching after hot forming for this grade, provided the temperature is not below the 1900 °F minimum.
- Welded (WLD) — automatic welding without filler metal, with the weld finished so the pipe meets dimensional and mechanical requirements after the final heat treatment. The strip or plate heat must itself carry the full UNS S30615 chemistry, so ask for the coil or plate heat number on the certificate.
- Heavily cold-worked (HCW) — welded pipe cold worked to at least 35% reduction of wall and weld before the final anneal, again without filler in the longitudinal seam, with the weld radiographed before cold work. Order HCW when the project specifically wants that marking and the process controls SA-312 writes around it.
Every finished length is hydrostatically tested or nondestructively electrically tested, and the mill may choose the method unless the purchase order fixes one. Pipe NPS 10 and larger may ship marked “NH” only when the purchaser accepts a system test in place of the hydrotest, and lots for mechanical testing follow clause 11.1. Because S30615 is usually bought for furnace components rather than pressure piping, the PO often adds straightness, ovality, or end-squareness requirements that SA-312 itself does not cover.
Welded pipe is the more common product, and heavy sections are sometimes made from heavy plate or replaced by castings for the most massive furnace parts. With 0.16–0.24% carbon, some carbon may not dissolve fully at the 1900 °F minimum and some producers anneal higher; SA-312 only fixes the minimum, so if the project needs a particular anneal temperature, put it on the PO and ask for it on the MTC. Availability can shape the furnace design, so discuss sizes with the supplier before drawings are frozen, and compare lead times against ASME SA312 UNS S30815 Stainless Steel Pipe when the atmosphere allows either.
Chemical Composition of SA312 UNS S30615
Heat analysis must conform to Table 1. Product analysis (S1) is judged with ASTM A480/A480M Table A1.1 tolerances via A999.
Melting analysis (heat / ladle analysis) — Table 1
Heat analysis for UNS S30615. Values are maximum unless a range is shown; ellipses (…) mean no requirement.
| Element | UNS S30615 melting analysis |
|---|---|
| Carbon (C) | 0.16 – 0.24 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.030 |
| Sulfur (S) | ≤ 0.03 |
| Silicon (Si) | 3.2 – 4.0 |
| Chromium (Cr) | 17.0 – 19.5 |
| Nickel (Ni) | 13.5 – 16.0 |
| Aluminum (Al) | 0.80 – 1.50 |
| Molybdenum (Mo) | … (no requirement) |
| Nitrogen (N) | … (no requirement) |
Source: ASME SA-312/SA-312M ≡ ASTM A312/A312M Table 1, UNS S30615 (grade column “…”); aluminium shown in the Aluminum column.
Product analysis — A480/A480M Table A1.1 tolerances applied to Table 1
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | 0.16 – 0.24 | 0.01 under / 0.02 over | 0.15 – 0.26 |
| Manganese (Mn) | ≤ 2.00 | 0.04 over | ≤ 2.04 |
| Phosphorus (P) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Sulfur (S) | ≤ 0.03 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | 3.2 – 4.0 | 0.15 under / over | 3.05 – 4.15 |
| Chromium (Cr) | 17.0 – 19.5 | 0.20 under / over | 16.80 – 19.70 |
| Nickel (Ni) | 13.5 – 16.0 | 0.15 under / over | 13.35 – 16.15 |
| Aluminum (Al) | 0.80 – 1.50 | 0.10 under / over | 0.70 – 1.60 |
Tolerance notes: carbon is unusual in spanning two A480 rows—the 0.16 minimum lies in “over 0.030 to 0.20” (0.01 under), while the 0.24 maximum lies in “over 0.20 to 0.60” (0.02 over). Aluminium 0.80–1.50% falls in the “over 0.50 to 2.00” row (0.10). Silicon 3.2–4.0% uses the “over 3.00 to 6.00” row (0.15). Nickel 13.5–16.0% is in the 10–20% row (0.15). Comparing the three high-silicon grades in SA-312 (Table 1):
| Element | S30600 | S30601 | S30615 |
|---|---|---|---|
| C | ≤ 0.018 | ≤ 0.015 | 0.16 – 0.24 |
| Si | 3.7 – 4.3 | 5.0 – 5.6 | 3.2 – 4.0 |
| Cr | 17.0 – 18.5 | 17.0 – 18.0 | 17.0 – 19.5 |
| Ni | 14.0 – 15.5 | 17.0 – 18.0 | 13.5 – 16.0 |
| Al | … | … | 0.80 – 1.50 |
| Purpose | Hot sulfuric acid | Hot strong sulfuric acid | Hot carburizing / oxidizing gases |
Element roles in S30615:
- Carbon 0.16–0.24% — elevated-temperature strength through carbides
- Silicon 3.2–4.0% — oxidation and carburization resistance via silica-rich scale
- Aluminium 0.80–1.50% — alumina-forming tendency that further improves oxidation and carburization resistance
- Chromium 17.0–19.5% — chromia scale and general oxidation resistance
- Nickel 13.5–16.0% — austenite stability against the ferrite-forming Si and Al
Mechanical Properties of SA312 UNS S30615
| Property (SA-312 Table 4) | UNS S30615 |
|---|---|
| Tensile strength, min | 90 ksi [620 MPa] |
| Yield strength (0.2% offset), min | 40 ksi [275 MPa] |
| Elongation in 2 in. or 50 mm (or 4D), min | 35% longitudinal / 25% transverse |
| Hardness | No maximum listed in Table 4 |
These floors are well above those of common heat-resisting grades; for example TP309S is listed in Table 4 at 75/30 ksi, reflecting the strengthening from carbon, silicon, and aluminium.
| Grade | UNS | Tensile min, ksi [MPa] | Yield min, ksi [MPa] |
|---|---|---|---|
| — | S30415 | 87 [600] | 42 [290] |
| — | S30615 | 90 [620] | 40 [275] |
| — | S30815 | 87 [600] | 45 [310] |
At service temperature, strength and creep behaviour are what matter for furnace parts. Producers publish elevated-temperature data for this chemistry; for code pressure design, use only allowable stresses listed for S30615 in the governing code.
Creep and sag: furnace tubes and rolls often fail by creep sag or distortion rather than by bursting. High carbon helps S30615 resist this through carbide strengthening. Designers should still use producer creep and rupture data for the actual operating temperature and support span, and allow for oxide thinning over the planned life.
Ductility after service: high-carbon heat-resisting alloys can lose room-temperature ductility after long exposure as carbides and other phases precipitate. This is expected behaviour, not a defect, but it affects repair welding and handling of used parts. Testing per SA-312: tension per lot, flattening or bend on 5% of pipes, hydro or NDE on every length. Elevated-temperature tests are PO options.
Dimensions and Tolerances
S30615 pipe follows ASME B36.19 schedules (5S, 10S, 40S, 80S) and special OD/wall by agreement. Furnace components such as radiant tubes and muffles are often ordered by OD and wall to the furnace builder’s drawing.
| NPS designator | Wall over | Wall under |
|---|---|---|
| 1/8 to 2-1/2 incl., all t/D | 20.0% | 12.5% |
| 3 to 18 incl., t/D up to 5% | 22.5% | 12.5% |
| 3 to 18 incl., t/D over 5% | 15.0% | 12.5% |
| 20 and larger, welded, all t/D | 17.5% | 12.5% |
| 20 and larger, seamless, t/D up to 5% | 22.5% | 12.5% |
| 20 and larger, seamless, t/D over 5% | 15.0% | 12.5% |
Source: SA-312 Table 3; outside diameter variations per A999/A999M.
- Lengths: NPS 1/8 to 8 up to 24 ft (15–24 ft range) unless agreed
- Cut lengths: up to 1/4 in. [6 mm] over, never under
- Jointers: not permitted unless specified
For radiant tubes and furnace rolls, straightness and ovality may matter more than SA-312 tolerances alone. Specify any tighter straightness, ovality, or end-squareness requirements on the PO. Heavy-wall seamless sizes are uncommon in this alloy, so designs needing thick sections sometimes use welded pipe from heavy plate or castings for the most massive parts. Discuss the size range with the supplier before finalising drawings, because availability can shape the design.
Thermal expansion of austenitic heat-resisting alloys is high; furnace designs accommodate growth with sliding supports and hangers. Length and support spacing should allow for this, especially with thin-wall welded pipe that may sag at temperature.
Equivalent Grades
| Designation | Relationship to S30615 |
|---|---|
| ASME SA-312 / ASTM A312, UNS S30615 | Governing pipe grade (no TP name) |
| ASTM A240 S30615 | Plate and sheet counterpart (separate specification) |
| EN / JIS | No one-to-one designation asserted |
| Producer trade names | Sold under proprietary names; order by UNS S30615 |
Alternatives for hot-gas service, depending on temperature and atmosphere, include ASME SA312 UNS S30815 Stainless Steel Pipe (Si-N-Ce micro-alloyed), ASME SA312 UNS S30415 Stainless Steel Pipe, TP309S and TP310S, and nickel-base alloys for the most severe conditions. They are not interchangeable without engineering review.
Do not confuse S30615 with the acid-service high-silicon grades ASME SA312 UNS S30600 Stainless Steel Pipe and ASME SA312 UNS S30601 Stainless Steel Pipe: their ultra-low carbon and S30615’s high carbon and aluminium point to completely different services.
Heat Treatment and Delivery Condition
S30615 has no individual row in SA-312 Table 2. The general requirement therefore applies: solution treat at 1900 °F [1040 °C] minimum, then quench in water or cool rapidly by other means at a rate sufficient to prevent carbide re-precipitation (demonstrable by A262 Practice E when S7 is ordered).
ASME clause 6.2 permits direct quenching of seamless pipe after hot forming for S30615 (it is not an H grade and not one of S33228, S30815, S31272), provided the temperature is not below the Table 2 minimum.
With 0.16–0.24% carbon, a portion of the carbon may not dissolve fully at the minimum temperature, and some producers anneal higher. SA-312 specifies only the minimum; if a project requires a particular anneal temperature, specify it on the PO and request it on the MTC.
- Delivered solution annealed and rapidly cooled
- Pickled or blasted, free of scale and exogenous iron
- Passivation on request (of limited relevance for high-temperature service)
- In service, the alloy will precipitate carbides; this is normal
Note on S7: an intergranular corrosion test is rarely meaningful for a high-carbon heat-resisting alloy intended for hot gas service, and is seldom ordered for S30615.
Corrosion Resistance
S30615 is a high-temperature gas corrosion alloy. Its value is in hot atmospheres, not aqueous corrosion.
- Carburization: silicon and aluminium form oxide layers that hinder carbon ingress; S30615 is widely described as resistant to carburizing atmospheres used in heat treatment
- Oxidation: Cr, Si, and Al together give good scaling resistance in air and combustion gases
- Sulfidation: the moderate nickel level and Si/Al oxide help in sulfur-bearing gases compared with high-nickel alloys, though severe reducing sulfidizing conditions remain aggressive
- Nitriding: silicon improves resistance to nitrogen pickup
- Aqueous corrosion: high carbon makes the alloy prone to sensitization; it is not intended for wet corrosive service
Thermal cycling: the oxide layer formed on Si/Al-bearing alloys tends to adhere well, reducing spalling. Furnace parts in cyclic service benefit from this. Performance in specific furnace atmospheres depends on temperature, gas composition, carbon potential, and cycling. Producer data and field experience should guide selection. SA-312 provides no high-temperature corrosion data; statements here are general guidance.
Metal dusting: some carbon-rich, low-oxygen atmospheres at intermediate temperatures cause metal dusting—a catastrophic carburization mechanism that pits and thins metal rapidly. Silicon- and aluminium-bearing alloys are sometimes used to resist it, but performance varies widely. Specialist advice is essential where metal dusting is possible.
Condensation during shutdown is a common cause of unexpected attack in heat-resisting alloys: acidic condensates from sulfur-bearing fuels can corrode sensitized material at low temperature. Design for drainage and dry shutdown where possible.
Applications of SA312 UNS S30615 Pipe
| Application | Role of S30615 | Note |
|---|---|---|
| Heat-treatment furnace radiant tubes | Carburization and oxidation resistance at temperature | Support design to limit sag |
| Muffles and retorts | Carburizing and nitriding furnaces | Often fabricated from plate and pipe together |
| Petrochemical furnace parts | Tube supports, hangers, and hot-gas piping | Confirm atmosphere compatibility |
| Furnace rolls and conveyor components | Strength and wear at temperature | Straightness critical |
| Thermowells and protection tubes | Hot-gas exposure | Wall thickness for life |
| Burner components and recuperators | Oxidizing and sulfur-bearing combustion gas | Condensate risk at cold end |
Typical service temperatures: furnace components in this alloy class commonly operate in the range where carburizing heat treatment is performed and above; producers quote use up to high furnace temperatures depending on atmosphere and load. Those figures come from producer literature and are not SA-312 values. For pressure-retaining parts, the code’s temperature limits for S30615 govern.
Life-cycle view: furnace parts are consumables, replaced on a schedule. Selecting S30615 is typically justified by longer replacement intervals in carburizing atmospheres, reducing downtime. Track actual life and wall loss so that future orders can be optimised.
For hot-gas applications where carburization is less severe, ASME SA312 UNS S30815 Stainless Steel Pipe or ASME SA312 UNS S30415 Stainless Steel Pipe may be more readily available.
Weldability
S30615 can be welded by GTAW, GMAW, and SMAW, but its high carbon, silicon, and aluminium make it more demanding than common heat-resisting grades. Filler metal and Table 6: UNS S30615 is not listed in SA-312 Table 6. No AWS A5.9 class is specified, and filler choice is by agreement, recorded on the WPS (and on the certificate for any seam repair under clause 15). Fabricators generally use matching consumables recommended by the alloy producer or, for some joints, nickel-base fillers that tolerate dilution; the choice affects the weld’s carburization and oxidation resistance.
- Hot cracking: Si and Al raise solidification-cracking risk; use low heat input and stringer beads
- Preheat: not normally required for austenitic alloys; follow producer guidance
- Interpass temperature: keep controlled and moderate
- Cleanliness: remove oils and markings that could contaminate the weld
- Aluminium oxide: clean joint surfaces thoroughly; Al-bearing oxides can interfere with fusion
Joining to other alloys: furnace assemblies often combine S30615 with 309, 310, or nickel alloys. Dissimilar joints are commonly made with nickel-base fillers that tolerate dilution from both sides and accommodate expansion differences. The joint will then have the corrosion characteristics of the filler, which should be considered when it sits in the hottest or most carburizing zone.
Repair of service-exposed parts: after high-temperature service, carbides and other precipitates reduce ductility and can make repair welding difficult. A solution anneal before repair, or careful buttering procedures, may be needed. Consult the producer.
Procedures should be qualified to ASME Section IX on S30615 base metal.
Surface Finishes
Surface condition for UNS S30615 pipe should be stated on the purchase order rather than left to mill default. For stainless pipe, embedded free iron, residual scale, and chloride-bearing residues are where corrosion starts, so the finish is part of the material performance and not just appearance. The finishes we regularly quote for this grade are listed below.
- Annealed and pickled (AP) — solution annealed at the 1900 °F [1040 °C] minimum, then descaled in acid pickle or an equivalent process to a matte grey finish; the standard choice for process pipe
- Blasted and pickled — common on heavy-wall seamless where blasting first makes scale removal more reliable
- Bright annealed (BA) — annealed in a protective atmosphere where mill capability exists for the size; the anneal temperature still has to meet the Table 2 practice for UNS S30615
- Mechanically polished — OD and/or ID polish to an agreed grit or Ra when ordered; polishing never replaces the solution anneal
- Bead-finished welded OD — weld bead rolled or ground flush as agreed on WLD and HCW product
For furnace service the cosmetic finish matters less than a clean, scale-free surface that lets the Si/Al oxide form evenly in first heat-up. Annealed and pickled or blasted and pickled is normal; bright annealing and polishing are rarely worth specifying for this grade. Remove oils, markings, and shop residues before first firing, because they can carburize or contaminate the surface locally. Passivation after pickling or polishing can be added when the end-user specification calls for it, even though SA-312 itself does not require it. If the project bans chloride-bearing marking inks, say so on the order; otherwise the mill will apply its normal stencil practice and ship its default AP finish.
Inspection and Testing
The base acceptance package for SA-312 UNS S30615 pipe combines chemistry, tensile testing, heat-treatment evidence, and a pressure or electrical integrity test on every length. The items below make up the usual package; supplementary requirements and project corrosion tests only apply when they are written on the purchase order.
- Heat (melting) analysis — mandatory per heat against Table 1 for UNS S30615: C 0.16–0.24%, Mn ≤2.00%, P ≤0.030%, S ≤0.03%, Si 3.2–4.0%, Cr 17.0–19.5%, Ni 13.5–16.0%, Al 0.80–1.50%
- Product analysis — when ordered (Suppl. S1 or PO wording), using A480 Table A1.1 tolerances via A999 §6.3; finished-pipe limits are C 0.15–0.26%, Si 3.05–4.15%, and Al 0.70–1.60%
- Tension test — 90 ksi [620 MPa] tensile, 40 ksi [275 MPa] yield, 35% L / 25% T elongation on a lot basis
- Flattening test — or the alternate bend test where the standard permits
- Hydrostatic or nondestructive electric test — every length; manufacturer’s option unless the order fixes the method
- Visual and dimensional check — against ordered NPS/schedule or OD × wall, with “UNS S30615” on every stencil
Mill test certificates: EN 10204 3.1 is the standard documentation from SHH STEEL supply. For S30615 the certificate should show carbon inside 0.16–0.24% (not below it), silicon inside 3.2–4.0%, aluminium inside 0.80–1.50%, and the solution-treatment temperature at or above 1900 °F. The S7 intergranular test in the table below is rarely meaningful for a high-carbon heat-resisting alloy in dry hot-gas service and is seldom ordered for S30615. EN 10204 3.2 or third-party witness by SGS, Bureau Veritas, TÜV, or the buyer’s nominated agency is arranged when specified, and it should be booked before final testing rather than after the heat has been released. Dual ASME SA-312 / ASTM A312 certification is available when chemistry, heat treatment, mechanical tests, and marking satisfy both editions named on the order.
| Option | Purpose |
|---|---|
| S1 product analysis | Confirms chemistry on finished pipe |
| S5 radiography | Weld integrity on WLD pipe |
| S7 intergranular corrosion | A262 Practice E after sensitizing treatment |
| S8 minimum wall | Wall interpreted as minimum rather than nominal |
| S9 weld decay | Compares weld and base-metal loss rates |
Receiving PMI needs care with this grade: XRF confirms chromium, nickel, and silicon approximately, but carbon and aluminium need OES or laboratory analysis, so a handheld gun alone cannot separate S30615 from other high-silicon stock. For radiant tubes and rolls, check straightness and ovality against the drawing as well as the SA-312 wall and OD tolerances.
Packaging and Shipping
Export and domestic shipments of UNS S30615 pipe are packed for handling and for ocean or land transport. The packing we normally apply is summarized below, and anything beyond it can be agreed on the order.
- Seaworthy bundles — pipes strapped or cradled in bundles sized for container or break-bulk handling, with non-metallic separators where the finish needs protecting
- End caps — plastic or metal caps on plain or beveled ends to keep out damage and contamination in transit
- Marking — specification, grade (UNS S30615), heat number, size, manufacturing type (SML / WLD / HCW), test letters, and mill identity as SA-312 and the purchase order require
- Export protection — waterproof wrapping or desiccant as agreed for polished or bright-annealed finishes, with low-chloride inks on request
Keep S30615 bundles segregated from the acid-service grades S30600 and S30601 and from 309S/310S stock, since the stencil shows only a UNS number and all of them look alike. Straightness-critical furnace tubes and rolls should be cradled or boxed so they arrive within the drawing tolerance rather than bowed from transport. Keep interiors dry and capped so chloride-bearing moisture cannot stain or pit the surface before installation. Shipping documents normally include the packing list, invoice, bill of lading or air waybill, and the 3.1 or 3.2 MTC with full Table 1 chemistry, plus origin and customs papers to suit the agreed Incoterms.
Why Choose SHH STEEL
SHH STEEL supplies specification-driven stainless plate and pipe, and for ASME SA312 UNS S30615 / S30615 we quote against the edition you name rather than a generic catalogue sheet. For S30615 the commercial risks are specific: a heat certified to the wrong high-silicon row, carbon reported below the 0.16% floor, or aluminium not reported at all. We source from mills that melt this chemistry regularly and check carbon, silicon, and aluminium against Table 1 before the pipe is released. Heat identity stays unbroken from the melt to the finished length, so receiving inspection can clear each heat against Table 1 and Table 4 without chasing paperwork after the pipe has arrived.
We are also straightforward about what SA-312 does not cover. Table 6 names no filler for S30615, the Table 2 default fixes only a 1900 °F minimum, and furnace performance depends on atmosphere, temperature, and cycling that the standard says nothing about. We write the filler, any higher anneal, and straightness requirements into the order, and if a carburizing duty is mild enough for S30815 or TP309S we will say so.
- Specification fidelity — certified as UNS S30615 with C, Si, and Al reported against Table 1 and the 1900 °F minimum solution treatment confirmed on the MTC
- Mill resources — SML, WLD, and HCW from qualified stainless pipe mills with heat traceability; cutting and beveling on confirmed orders
- Documentation — EN 10204 3.1 MTCs as standard with full Table 1 chemistry; 3.2 or third-party inspection on request
- Dual marking — ASME SA-312 and ASTM A312 when the heat and tests meet both editions you name
- Related grades — UNS S30815, UNS S30415, TP309S, and TP310S when a project buys a matched package
- Export packing — seaworthy bundles, end protectors, and durable grade, heat, size, and type marking
Quotations follow your purchase-order language for edition year, manufacturing type, size, wall, finish, and any supplementary tests you name (S1, S5, S7, S8, S9). If the same project also needs plate or fittings, ask for coordinated heats so the chemistry lines up across product forms. Grade hub: ASME SA 312/SA 312M.
Supply Capability
SHH STEEL can supply ASME SA312 UNS S30615 stainless steel pipe against the edition and manufacturing type named on your enquiry. The capability table below summarizes the routes, sizes, finishes, and documents we regularly quote for this grade.
| Item | SHH STEEL capability for UNS S30615 |
|---|---|
| Standard | ASME SA-312/SA-312M and/or ASTM A312/A312M (edition per PO; grade marked UNS S30615, no TP name) |
| Manufacturing types | SML, WLD, HCW |
| Size | NPS 1/8 and up per ASME B36.19; special OD/wall by agreement |
| Schedules | 5S, 10S, 40S, 80S and non-standard walls |
| Length | SRL, DRL, or cut-to-length |
| Finish | Annealed and pickled; blasted and pickled; bright annealed or polished by agreement |
| Testing | Hydrostatic or NDE per length; S1 product analysis with OES for C and Al; straightness/ovality checks when ordered |
| Documents | EN 10204 3.1 with full Table 1 chemistry; third-party inspection / 3.2 on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
S30615 is normally made to order, with welded pipe more readily available than seamless, and remnant lengths sometimes cover small replacement lots for furnace maintenance. Send the furnace builder’s drawing, OD × wall, lengths, quantities, and the atmosphere and temperature so feasibility and lead time can be confirmed before the outage date is fixed. Enquiries should state the SA-312 edition, UNS S30615 (no TP name), SML/WLD/HCW, NPS or OD × wall (and whether wall is nominal or minimum), length practice, finish, and any product-analysis, corrosion-test, or 3.2 requirements, so mill slots line up with your need date. Cut lengths, beveling, and packing-list marking are available on confirmed orders, and grouping project sizes onto one heat keeps the chemistry consistent while helping meet mill minimums without over-ordering.
FAQ
-
Does UNS S30615 have a TP grade name in SA-312?
- No. Table 1 lists S30615 with an ellipsis in the grade column, so there is no TP designation. Order and mark it as “ASME SA-312 UNS S30615” or ASTM A312 UNS S30615 with the edition year. A trade name or a loose “high-silicon 309” description does not identify the Table 1 row the heat must meet.
-
What is ASME SA312 UNS S30615 pipe used for?
- It is a heat-resisting grade for hot carburizing, oxidizing, and sulfur-bearing gases—heat-treatment furnace radiant tubes, muffles and retorts, furnace rolls, thermowells, and petrochemical furnace parts. Silicon and aluminium form an adherent oxide that slows carbon pickup and scaling. It is not intended for wet corrosive service, where its high carbon is a liability.
-
Why is carbon so high in UNS S30615?
- Table 1 requires 0.16–0.24% carbon on purpose. The carbon forms stable carbides that give strength and creep resistance at furnace temperatures, which helps tubes and rolls resist sag. A reading near 0.20% on the MTC is correct; a heat below 0.16% does not meet the grade, even though low carbon would be welcome in other stainless steels.
-
What does aluminium do in S30615?
- Aluminium at 0.80–1.50% works with the 3.2–4.0% silicon to build an oxide layer that resists scaling and slows carbon ingress in carburizing atmospheres, and that oxide tends to adhere well through thermal cycling. Because handheld XRF does not measure aluminium reliably, ask for it on the heat analysis and use OES if you need product verification.
-
What are the Table 4 mechanical requirements for S30615?
- Table 4 sets 90 ksi [620 MPa] minimum tensile and 40 ksi [275 MPa] minimum yield, with 35% longitudinal and 25% transverse elongation and no hardness limit. Those floors are well above TP309S at 75/30 ksi. For furnace parts, creep and sag at temperature matter more, so size walls and support spans from producer data and the governing code.
-
What heat treatment applies to UNS S30615 pipe?
- S30615 has no individual Table 2 row, so the general requirement applies: solution treat at 1900 °F [1040 °C] minimum, then quench in water or cool rapidly. Clause 6.2 allows direct quenching of seamless pipe after hot forming for this grade. Some producers anneal higher because of the carbon level; specify any required temperature on the PO.
-
Which filler metal is specified for welding S30615?
- None. S30615 is not listed in SA-312 Table 6, so filler is by agreement and must be recorded on the WPS, and on the certificate for any seam repair. Fabricators use matching consumables recommended by the alloy producer or, for dissimilar joints, nickel-base fillers that tolerate dilution; the choice affects the weld’s carburization resistance.
-
How does S30615 differ from UNS S30600 and S30601?
- All three carry a lot of silicon, but S30600 and S30601 are ultra-low carbon (≤0.018% and ≤0.015%) for hot concentrated sulfuric acid, while S30615 has 0.16–0.24% carbon plus 0.80–1.50% aluminium for hot gases. They are opposite designs, and putting one where another is specified would be a serious error, so always check the UNS number.
-
How does UNS S30615 compare with UNS S30815?
- S30815 is a 21Cr–11Ni grade micro-alloyed with silicon, nitrogen, and cerium, with 87/45 ksi minima and a reheated 1920 °F anneal; it is aimed at cyclic oxidation. S30615 relies on silicon, aluminium, and high carbon, with 90/40 ksi minima, and is preferred where carburization is the main threat. Choose by atmosphere and temperature, not by price alone.
-
Is UNS S30615 suitable for wet corrosive service?
- No. With 0.16–0.24% carbon the alloy sensitizes readily, so it is not chosen for aqueous corrosion. Watch for acidic condensate from sulfur-bearing fuels during furnace shutdowns, which can attack sensitized material at low temperature. Design for drainage and dry shutdown where possible, and keep S30615 to the hot-gas duty it was developed for.
-
Is UNS S30615 an H grade?
- No. It is not listed in clause 1.2 as an H grade, has no Table 5 grain-size requirement, and is not one of the grades that clause 6.2 requires to be reheated before quenching. Its high carbon serves the same strength purpose that H grades target, but the H-grade rules in SA-312 do not apply to it.
-
Can UNS S30615 be supplied seamless?
- SA-312 permits seamless, welded, and heavily cold-worked S30615, and all routes must meet the same Table 1 chemistry and 1900 °F minimum solution treatment. Seamless supply is limited, especially in heavy walls, so welded pipe is more common. For radiant tubes and rolls, write straightness and ovality limits on the PO, since SA-312 covers only wall and OD.
Conclusion
ASME SA312 UNS S30615 is a TP-less heat-resisting austenitic pipe grade with C 0.16–0.24%, Si 3.2–4.0%, and Al 0.80–1.50% on a Cr 17.0–19.5% / Ni 13.5–16.0% base, meeting 90 ksi [620 MPa] tensile and 40 ksi [275 MPa] yield minima after the 1900 °F [1040 °C] default solution treatment. It is built for hot carburizing and oxidizing gases, is not related in service to the acid-grade UNS S30600 or S30601, and leaves filler selection to agreement because it is not in Table 6. For sizes, lead times, mill certificates, or dual SA-312/A312 supply, contact SHH STEEL at admin@steelspecs.com or browse the ASME SA 312/SA 312M category.
Quality Steel Needed? Inquire for Offers
Related Products