ASME SA312 TP201 Stainless Steel Pipe | SA 312/SA 312M
What is ASME SA312 TP201 Stainless Steel Pipe
ASME SA-312/SA-312M covers seamless, welded, and heavily cold-worked austenitic stainless steel pipe intended for high-temperature and general corrosive service. Grade TP201 is listed in Table 1 as UNS S20100. Commercially the same product may be called SA312 TP201 pipe, ASTM A312 TP201 pipe, A312 Grade TP201, or 201 stainless steel pipe when the purchase order clearly references SA-312 or A312. For pressure piping and code work, cite the full grade designation and the edition of the standard on the purchase order and on the mill test certificate—do not rely on a bare “201” market label.
TP201 is an austenitic chromium–manganese–nickel–nitrogen grade. Versus classic 18-8 chromium–nickel grades, it raises manganese and allows controlled nitrogen while keeping nickel leaner (3.5–5.5% on heat analysis). Chromium remains in the 16.0–18.0% band. That chemistry still supports the tensile and elongation floors in SA-312 Table 4 for many general corrosive and utility services, at a more economical nickel bill of material than TP304-class pipe when the fluid and temperature suit 201-class stainless.
Common commercial names and how they map:
- ASME SA312 TP201 / SA-312 Grade TP201 — preferred marking language for ASME-code and dual-marked pipe
- ASTM A312 TP201 — same grade tables for chemistry and tensile when the ASTM edition is referenced
- UNS S20100 — unified numbering system identity used on MTCs and in cross-reference tables
- 201 stainless steel pipe — market shorthand; confirm SA-312/A312 and heat-analysis limits on the order
Related flat product in the same UNS family is available as plate. When a project mixes plate and pipe, buyers often pair this pipe grade with ASME SA240 UNS S20100 Stainless Steel Plate so that heat chemistry language stays consistent across forms. Pipe itself must still be ordered and tested to SA-312/A312—not to the plate specification.
SHH STEEL quotes TP201 against the edition named on the enquiry, including manufacturing type, size, finish, and supplementary requirements. See ASME SA 312/SA 312M and ASME SA312 TP201 Stainless Steel Pipe.
Manufacturing Types (SML / WLD / HCW)
ASME SA-312 defines three manufacturing routes that may be marked on finished TP201 pipe. Selecting the route is a purchase-order decision driven by design code, size range, wall thickness, and inspection preference. It does not change the Table 1 chemistry of Grade TP201.
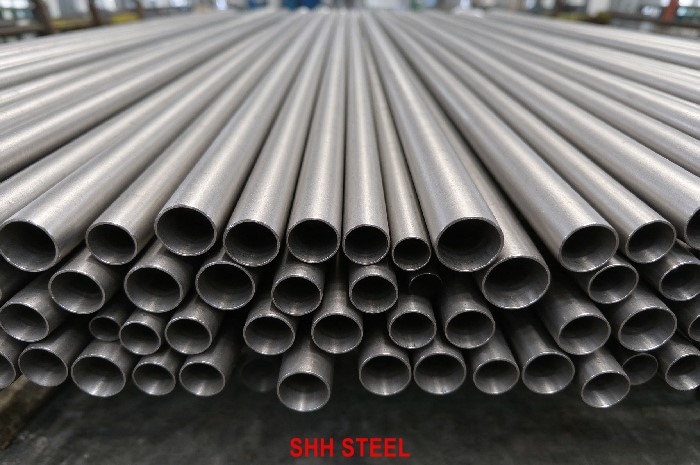
- Seamless (SML) — no welding at any stage of manufacture. Seamless is preferred when the project specification excludes welded pipe, when thick walls favor seamless production, or when the piping class documentation is written around seamless product only.
- Welded (WLD) — automatic welding without filler metal. The weld is finished so that the pipe meets dimensional and mechanical requirements after the final heat treatment required by SA-312. Welded product is widely used for common NPS and schedule combinations where the code accepts welded austenitic pipe.
- Heavily cold-worked (HCW) — welded pipe that is cold worked to a reduction of area of wall and weld of at least 35% before the final anneal, again without filler metal in the longitudinal weld. HCW is ordered when the buyer wants the HCW marking and the process controls written into SA-312 for that route.
Each finished length is hydrostatically tested or nondestructively electrically tested. The manufacturer may choose the method unless the purchase order fixes one. Marking on the pipe typically includes the manufacturer, grade, heat number, NPS or outside diameter and schedule or wall thickness, and the manufacturing type letters SML, WLD, or HCW. When comparing seamless versus welded TP201 offers, check manufacturing type and the hydro or NDE method on the mill test certificate—not only the grade stamp.
Chemical Composition of SA312 TP201
Two chemistry layers matter: melting (heat / ladle) analysis—mandatory per heat under ASME SA-312/ASTM A312 Table 1—and product analysis when ordered (Suppl. S1 / PO). SA-312/A312 defer product-analysis tolerances through ASTM A999/A999M §6.3 to ASTM A480/A480M-22a Table A1.1. SHH STEEL reports actual ladle and, when ordered, product values—never unpublished tighter windows.
Melting analysis (heat / ladle analysis) — Table 1
Heat analysis for Grade TP201 / UNS S20100 from ASME SA-312/SA-312M (ASTM A312/A312M) Table 1. Values are maximum unless a range is shown.
| Element | TP201 (UNS S20100) melting analysis |
|---|---|
| Carbon (C) | ≤ 0.15 |
| Manganese (Mn) | 5.5 – 7.5 |
| Phosphorus (P) | ≤ 0.060 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 16.0 – 18.0 |
| Nickel (Ni) | 3.5 – 5.5 |
| Nitrogen (N) | ≤ 0.25 |
Source: ASME SA-312/SA-312M ≡ ASTM A312/A312M Table 1 for Grade TP201. Do not treat secondary catalog sheets as a substitute for the ordered edition.
Mn and N distinguish 201 from classic TP304; Ni is leaner. Carbon ≤0.15% is above an “L” grade ceiling—review welding and post-weld exposure when sensitization risk matters.
Product analysis — A480/A480M Table A1.1 tolerances applied to Table 1
When product analysis is ordered, finished-pipe chemistry shall meet Table 1 as modified by the product-analysis tolerances of ASTM A480/A480M Table A1.1 (via A999 §6.3 deferral). The verified product-analysis limits for TP201 are:
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.15 | 0.01 over | ≤ 0.16 |
| Manganese (Mn) | 5.5 – 7.5 | 0.05 under / 0.06 over | 5.45 – 7.56 |
| Phosphorus (P) | ≤ 0.060 | 0.010 over | ≤ 0.070 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 16.0 – 18.0 | 0.20 under / over | 15.80 – 18.20 |
| Nickel (Ni) | 3.5 – 5.5 | 0.07 under / 0.10 over | 3.43 – 5.60 |
| Nitrogen (N) | ≤ 0.25 | 0.02 over | ≤ 0.27 |
If an enquiry only says “201 stainless pipe,” confirm Table 1 limits, manufacturing type, and product analysis before rolling. Plate chemistry: ASME SA240 UNS S20100 Stainless Steel Plate—pipe remains SA-312.
Mechanical Properties of SA312 TP201
Tensile requirements for TP201 are given in ASME SA-312/SA-312M (ASTM A312/A312M) Table 4. Specimens and orientation follow the testing clauses of the standard and the referenced general requirements (A999/A999M as applicable).
| Property | TP201 requirement (Table 4) |
|---|---|
| Tensile strength, min | 75 ksi [515 MPa] |
| Yield strength (0.2% offset), min | 38 ksi [260 MPa] |
| Elongation in 2 in. or 50 mm (or 4D) | 35% longitudinal / 25% transverse, min |
These minima are the mandatory acceptance floor. Actual mill test certificate values are often higher; design calculations should still use Table 4 unless the purchase order states higher guaranteed values that the mill has accepted in writing.
Hardness: A312/SA-312 Table 4 does not list a hardness maximum for TP201. Hardness is not a separately mandated Table 4 acceptance item. Do not treat catalog Brinell or Rockwell figures as specification-mandatory. If hardness matters for fabrication or end-user acceptance, state the limit on the purchase order and verify it on the MTC; otherwise omit hardness as a mandatory acceptance item.
Versus ASME SA312 TP304 Stainless Steel Pipe, TP201 shares 75 ksi tensile min but has higher 38 ksi yield min (TP304: 30 ksi). For chloride service prefer ASME SA312 TP316 Stainless Steel Pipe or ASME SA312 TP316L Stainless Steel Pipe. Flattening/bend and tension run on a lot basis; supplementary tests only when listed on the PO.
Dimensions and Tolerances
Dimensional practice for austenitic stainless steel pipe ordered to SA-312 typically follows ASME B36.19 / B36.19M stainless-steel pipe schedules. Outside diameter and wall thickness are stated as NPS and schedule, or as OD and specified wall. Common schedules for TP201 enquiry include Schedule 5S, 10S, 40S, and 80S. Other walls and non-standard OD/wall combinations are available by agreement when both the mill and the order accept them.
Size coverage in commercial practice:
- NPS / DN: commonly from NPS 1/8 upward; large NPS and heavy walls depend on manufacturing type (SML versus WLD/HCW) and mill capability—confirm on enquiry
- Schedules: 5S, 10S, 40S, 80S and special walls by agreement
- Length: single random (SRL), double random (DRL), or fixed cut lengths as stated on the purchase order
- Ends: plain end (PE), beveled end (BE), or other end preparations by agreement
OD, wall, and length tolerances follow SA-312 via ASTM A999/A999M and the dimensional standard on the order. SHH STEEL quotes the applicable clause rather than dumping entire A999 tables. Confirm max wall and NPS near the edge of B36.19 practice before acceptance.
Equivalent Grades
Equivalence for TP201 must be stated carefully. Chemistry approximations across regional designations help material selection discussions; they are not automatic one-to-one substitutes for ASME pressure-code pipe without an approved material specification and design-code acceptance.
| Designation | Notes |
|---|---|
| ASME SA-312 / ASTM A312 Grade TP201 | Governing pipe product standard for this article |
| UNS S20100 | Unified number listed in Table 1 |
| EN 1.4372 (X12CrMnNiN17-7-5) | Approximate wrought stainless designation; EN tube/pipe product forms are ordered under the relevant EN product specs, not by EN number alone on an SA-312 MTC |
| JIS SUS201 | Approximate Japanese grade name; confirm the Japanese pipe/tube product standard when ordering JIS product |
| Plate counterpart | ASME SA240 UNS S20100 Stainless Steel Plate for flat product in the same UNS family |
Within SA-312, ASME SA312 TP201LN Stainless Steel Pipe (UNS S20153) has its own Table 1/Table 4 limits—do not interchange with TP201. Sisters: ASME SA312 TP304 Stainless Steel Pipe, ASME SA312 TP304L Stainless Steel Pipe, ASME SA312 TP316 Stainless Steel Pipe, ASME SA312 TP316L Stainless Steel Pipe. Hub: ASME SA 312/SA 312M. Plate: ASME SA240 304 Stainless Steel Plate, ASME SA240 316 Stainless Steel Plate.
Pressure-code caution: EN/JIS approximations do not authorize B31 or Section VIII substitution without engineered approval.
Heat Treatment and Delivery Condition
All pipe furnished to ASME SA-312 shall be heat treated. For TP201 and other grades that do not carry an individual temperature row in Table 2, the default minimum solution-annealing temperature is 1900 °F [1040 °C], followed by water quenching or another rapid cool sufficient to prevent harmful carbide reprecipitation. That Table 2 default is SHH STEEL’s delivery baseline unless the ordered edition of SA-312 states otherwise for the heat.
Seamless pipe may be quenched after hot forming when the edition allows and finishing temperature is not below the min anneal. H-grade reheating notes do not change this TP201 path. HCW cold reduction is done before final anneal; delivery remains the annealed condition—cold work is not a final hardness condition.
Commercial delivery condition typically includes:
- Solution annealed to SA-312 Table 2 requirements for TP201
- Pickled and descaled, or bright annealed, as ordered (see Surface Finishes)
- Straightened and cut to the ordered length practice
- Hydrotested or NDE-tested per length as required by the standard and the purchase order
Corrosion Resistance
TP201 is selected for general corrosive service where lean-nickel austenitic stainless with manganese–nitrogen austenite stabilization is accepted by the end-user specification. In many oxidizing aqueous environments and atmospheric exposures, 201-class stainless can perform adequately for utility and light process duty. It is not a universal substitute for classic 18-8 or molybdenum-bearing grades.
Versus TP304: Similar Cr band, leaner Ni with Mn–N stabilization. Not automatically interchangeable with ASME SA312 TP304 Stainless Steel Pipe when specs are written around 304/304L. Plate: ASME SA240 304 Stainless Steel Plate.
Versus TP316: Mo-bearing grades resist chlorides/reducing media better. Do not use TP201 as a drop-in for ASME SA312 TP316 Stainless Steel Pipe or ASME SA240 316 Stainless Steel Plate in seawater/brine. Prefer Mo austenitic or duplex if chlorides dominate.
Oxidizing versus reducing media: Chromium-rich passive films help in many oxidizing environments. Strongly reducing acids, high chloride concentrations, crevice geometries, and stagnant seawater are poor matches for lean-nickel 201. Local corrosion (pitting and crevice attack) risk rises where chlorides concentrate under deposits or in poorly drained pockets.
Surface condition: Proper pickling and passivation after fabrication help restore a clean passive surface and remove free iron from handling. Mill annealed-and-pickled pipe already carries a descaled surface; site welding and grinding should be cleaned and passivated when the end-user specification requires it. Corrosion performance always depends on the actual fluid, temperature, velocity, and fabrication cleanliness—not on grade name alone.
Applications of SA312 TP201 Pipe
TP201 pipe is selected where austenitic stainless behavior, SA-312 product form, and a leaner nickel chemistry are acceptable for the fluid and temperature. Typical application areas include:
| Application area | Typical use of TP201 pipe | Selection note |
|---|---|---|
| Utility and process piping | Water, air, mild chemical transfer lines ordered to SA-312 | Confirm fluid compatibility with 201 chemistry |
| Structural / architectural | Handrail, support, and decorative pipe ordered as SA-312 product | Higher minimum yield versus TP304 can help section design |
| Food-contact and light process | Lines where 201 stainless is accepted by the end-user specification | Follow hygiene finish and welding procedure requirements |
| Transportation / OEM | Frames and piping kits converting to SA-312 documentation | Dual SA312/A312 marking often requested |
| General corrosive service | Mild to moderate environments without heavy chlorides | Prefer TP316/TP316L or higher alloys if chlorides dominate |
| High-temperature general service | Lines where SA-312 austenitic pipe is specified and 201 chemistry is accepted | Review sensitization risk for intermittent high-temperature exposure after welding |
When the same plant also uses 18-8 plate, buyers sometimes standardize documentation by pairing TP201 pipe with ASME SA240 UNS S20100 Stainless Steel Plate, or by staying entirely in the 304 family with ASME SA240 304 Stainless Steel Plate and ASME SA312 TP304 Stainless Steel Pipe. Match the grade family to corrosion and code needs first; nickel-cost savings are secondary to fitness for service.
Weldability
TP201 is generally weldable by common austenitic fusion processes with suitable heat input, interpass, and cleanliness:
- GTAW (TIG) — preferred for root passes and thin-wall pipe where weld metal cleanliness and heat-input control matter
- GMAW (MIG) — productive for fill and cap passes on thicker walls when procedures are qualified
- SMAW — widely used for field girth welds with coated austenitic electrodes selected by agreement
- Automatic orbital or mechanized GTAW — common for repetitive hygienic or high-integrity girth joints
With C up to 0.15%, evaluate HAZ sensitization for carbide-precipitation exposure after welding. Low heat input, controlled interpass, or post-weld anneal / lower-carbon alternatives are engineering choices—not automatic SA-312 requirements on every order.
Filler metal: SA-312 Table 6 shows the filler recommendation for TP201 as “…” (no AWS classification listed). Filler selection is by agreement—typically a matching 201-type consumable or an approved higher-alloy austenitic consumable documented on the WPS/PQR. Do not treat ER308 or ER308L as mandatory Table 6 filler for TP201. Record the agreed AWS (or EN) consumable on the welding procedure. Note that mill longitudinal welds for WLD and HCW product are made without filler metal; Table 6 guidance applies to joining with filler, not to the mill autogenous weld.
Girth welds follow the piping/vessel code (e.g. ASME B31 / Section IX) and are separate from mill hydro/NDE. Specify girth NDE on fabrication documents when required. Keep joints clean of oil, paint, and carbon-steel contamination.
Surface Finishes
Surface condition for SA312 TP201 pipe is stated on the order. Typical mill finishes include:
- Annealed and pickled (AP) — solution annealed, descaled in acid pickle or an equivalent process, producing a matte gray finish common for process and utility pipe
- Bright annealed (BA) — annealed in a protective atmosphere to a brighter surface where the order allows and mill capability exists for the size
- Mechanically polished — for example 180#, 320#, or 400# grit, or Ra-controlled polish on OD and/or ID for hygienic or architectural duty; polishing does not replace solution annealing
- Bead-finished welded OD — weld bead rolled or ground flush as agreed for WLD/HCW product
Passivation after pickle or polish can be added when the end-user specification requires it. For food or pharmaceutical lines, state both the Ra (or grit) target and the documentation package—including any surface roughness reports—on the enquiry. SHH STEEL will not imply a polished hygienic finish on standard AP pipe unless the purchase order says so. End preparation (plain or beveled) should be ordered together with finish so that bevel faces and ID cleanliness meet the same acceptance language.
Inspection and Testing
Base inspection and testing for SA-312 TP201 pipe combines chemistry, mechanical, and integrity checks. The following items form the usual acceptance package; supplementary requirements apply only when written on the purchase order.
- Heat (melting) analysis — mandatory per heat against Table 1 for TP201 (UNS S20100)
- Product analysis — when ordered (Suppl. S1 / purchase-order language), using A480 Table A1.1 tolerances via A999 §6.3
- Tension test — Table 4 tensile, yield, and elongation on a lot basis
- Flattening test — or alternate bend where the standard permits for certain welded pipe
- Hydrostatic test or nondestructive electric test — each length; manufacturer’s option unless the order fixes the method
- Visual and dimensional check — against ordered NPS/schedule or OD/wall and the applicable tolerance clauses
Mill test certificates: EN 10204 3.1 is the standard documentation package from SHH STEEL supply. EN 10204 3.2 or third-party witness (SGS, Bureau Veritas, TÜV, or the buyer’s nominated agency) is arranged when specified. Dual ASME SA-312 / ASTM A312 certification is available when chemistry, heat treatment, mechanical tests, and marking satisfy the edition(s) named on the order.
Optional / supplementary: PMI, RT/UT, intergranular corrosion or weld-decay tests, tighter straightness, special marking—only when listed on the PO. Keep heat numbers on cut pieces for MTC traceability.
Packaging and Shipping
Export and domestic shipments of SA312 TP201 pipe are packed for handling and ocean or land transport. Typical practices include:
- Seaworthy bundles — pipes strapped or cradled in bundles sized for container or break-bulk handling, with separators where needed to protect finish
- End caps / protectors — plastic or metal caps on plain or beveled ends to reduce damage and contamination during transit
- Marking — durable marking of grade (TP201), heat number, size (NPS or OD × wall / schedule), manufacturing type (SML / WLD / HCW), and mill identity as required by SA-312 and the purchase order
- Export packing — waterproof wrapping or tarpaulin as agreed for polished or sensitive finishes; container stuffing photos on request
Shipment docs typically include packing list, invoice, B/L or AWB, and MTC (3.1 or 3.2), plus origin/customs papers per Incoterms. State destination, packing preference, and extra marking at enquiry.
Why Choose SHH STEEL
SHH STEEL supplies specification-driven stainless plate and pipe. For SA312 TP201 we emphasize:
- Specification fidelity — chemistry and tensile to SA-312/A312 Table 1 and Table 4 for TP201 (S20100), not vague “201” catalog sheets
- Mill resources — SML, WLD, and HCW from qualified stainless pipe mills with heat traceability
- Documentation — EN 10204 3.1 MTCs standard; 3.2 or third-party inspection on request
- Dual marking — ASME SA-312 and ASTM A312 when the heat and tests meet both requirements you name
- Related forms — pipe aligned with ASME SA240 UNS S20100 Stainless Steel Plate when projects buy both
- Export packing — seaworthy bundles, end protectors, and durable grade/heat/size/type marking
Quotations follow your PO language. Grade hub: ASME SA 312/SA 312M.
Supply Capability
| Item | SHH STEEL capability for TP201 |
|---|---|
| Standard | ASME SA-312/SA-312M and/or ASTM A312/A312M Grade TP201 (UNS S20100) |
| Manufacturing types | SML, WLD, HCW |
| Size | NPS 1/8 and up per ASME B36.19; special OD/wall by agreement |
| Schedules | 5S, 10S, 40S, 80S and non-standard walls |
| Length | SRL, DRL, or cut-to-length |
| Finish | Annealed and pickled, bright annealed, polished by agreement |
| Testing | Tension, flattening/bend, hydro or NDE per length; supplementary tests on order |
| Documents | EN 10204 3.1; third-party inspection / 3.2 on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
| Contact | admin@steelspecs.com |
Stock moves with mill rolling cycles. Enquiries state China origin with approximate availability bands by size. Cut lengths, beveling, and packing-list marking are available on confirmed orders.
FAQ
-
Is ASME SA312 the same as ASTM A312?
- For chemistry (Table 1), tensile (Table 4), manufacturing types, and most testing language, ASME SA-312/SA-312M matches ASTM A312/A312M of the referenced edition. Dual SA312/A312 marking is common when ordered.
-
TP201 vs TP304 — which should I order?
- Order TP201 for S20100 Mn–N lean-nickel chemistry and 38 ksi min yield. Order TP304/TP304L when the project is written around classic 18-8 chemistry. They are not automatic drop-in replacements.
-
TP201 vs TP201LN?
- Different UNS numbers, Table 1 chemistries, and Table 4 tensile floors. Order the exact design grade (TP201 = S20100; TP201LN = S20153).
-
What is the maximum wall or NPS for TP201?
- No single marketing maximum in SA-312. Feasible NPS/wall depend on SML vs WLD/HCW, mill tooling, and B36.19 plus special walls by agreement. Confirm on enquiry.
-
Seamless vs welded TP201 — which is better?
- Neither is universally better. Choose the manufacturing type your design code and datasheet allow; both are legitimate SA-312 forms when tested to the standard.
-
Can you dual-certify SA312 / A312 TP201?
- Yes, when heat analysis, heat treatment, mechanical tests, and marking meet both editions named on the order.
-
Hydrostatic test vs NDE — which do I get?
- Each length is hydrotested or nondestructively electrically tested. Manufacturer may choose unless the purchase order fixes the method.
-
Does Table 4 specify hardness for TP201?
- No. Table 4 has no hardness maximum for TP201. Order hardness on the PO only if your project needs it.
-
What filler should I use to weld TP201 pipe?
- Table 6 lists “…” for TP201—filler by agreement, not ER308 mandatory. Mill WLD/HCW longitudinal welds use no filler. Document the consumable on the WPS.
-
Do you supply related plate in S20100?
- Yes—ASME SA240 UNS S20100 Stainless Steel Plate. Order pipe to SA-312 and plate to SA-240 separately.
Conclusion
ASME SA312 TP201 (UNS S20100) is the lean-nickel austenitic pipe grade in SA-312 for high-temperature and general corrosive service when manganese–nitrogen chemistry is accepted. Order the manufacturing type (SML/WLD/HCW), schedule or wall, finish, and any product analysis or supplementary tests explicitly. For stock checks, cut-length packages, or mill certificates, contact SHH STEEL at admin@steelspecs.com or browse the ASME SA 312/SA 312M category on steelspecs.com.
Quality Steel Needed? Inquire for Offers
Related Products