ASME SA213 UNS S31254 Stainless Steel Tube
What is ASME SA213 UNS S31254 Stainless Steel Tube
ASME SA-213 / SA-213M is the ASME Boiler and Pressure Vessel Code Book adoption of the seamless ferritic and austenitic alloy-steel boiler, superheater, and heat-exchanger tube product text. When Code-stamped boilers, seawater coolers, or chloride-side heat exchangers invoke that adoption by name, SA-213 is the governing product standard for this 6Mo superaustenitic tube — written as its own Code Book line, not as a merged synonym of ASTM A213. Begin from SA213/SA213M when the enquiry is Code-led.
UNS S31254 sits in the stainless chemistry table without a TP grade letter (Footnote C practice). Melting carbon is capped at ≤0.020%, chromium in a tight 19.5–20.5% band, nickel at 17.5–18.5%, molybdenum in a deliberate 6.0–6.5% window, nitrogen at 0.18–0.22%, and copper at 0.50–1.00%, with manganese ≤1.00%, silicon ≤0.80%, phosphorus ≤0.030%, and sulfur ≤0.010%. Table 4 is wall-split: 98 ksi [675 MPa] / 45 ksi [310 MPa] for wall ≤0.187 in. [5 mm], and 95 ksi [655 MPa] / 45 ksi [310 MPa] for thicker walls, with elongation 35% minimum and hardness max 220 HBW / 96 HRB. Buyers who write “254 SMO” or “6Mo HX tube” on a bill of materials still need to name SA-213 UNS S31254 on the purchase order so the mill applies the tube product standard, minimum-wall rules, and the Mo/N/Cu windows together. This is not a dual stamp of SA213 TP317LMN or of SA213 TP316L.
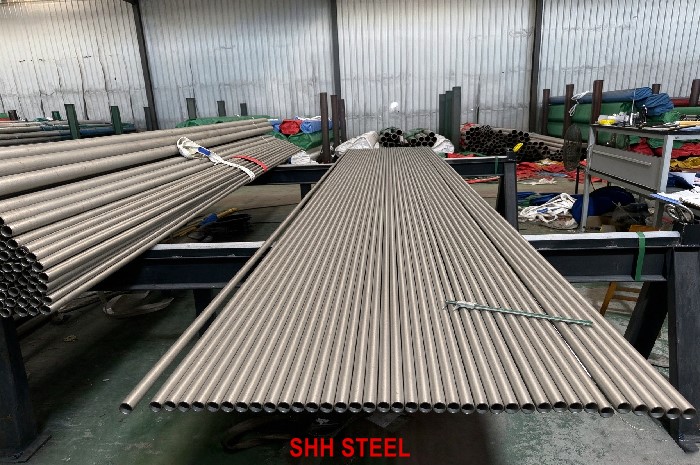
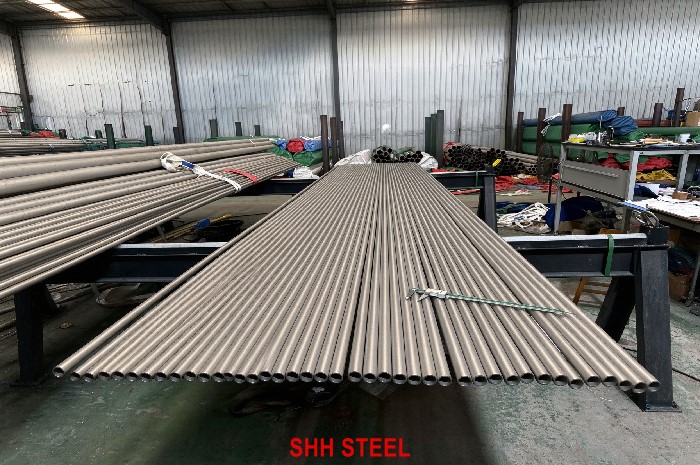
SHH STEEL can supply ASME SA213 UNS S31254 as seamless cold-finished and hot-finished tube in the usual OD × wall / BWG band, with EN 10204 3.1 certificates that report molybdenum, nitrogen, and copper together with the wall-appropriate tensile set, 35% elongation, and hardness. Dual SA-213/A213 marking is added only when the purchase order asks; the live twin is A213 UNS S31254.
Shop names include “S31254,” “254 SMO,” and “6Mo.” Helpful for routing; the commercial 254 SMO trademark nickname does not replace UNS S31254 on the MTC. The purchase order should still carry ASME SA-213 UNS S31254, wall basis, OD × wall or BWG, finish route, and any Supplementary Requirements when needed. Sister SA213 pages include SA213 TP317LMN, SA213 TP317LM, SA213 TP316L, and SA213 TP310MoLN. Seamless only — no Manufacturing Types (SML / WLD / HCW) product-form split on this page.
Chemical Composition of SA213 UNS S31254
Two chemistry layers matter for UNS S31254 under ASME SA-213. Melting analysis is mandatory for every heat; product analysis on finished tube applies only when Supplementary Requirement wording or the purchase order invokes it through the general requirements (commonly ASTM A1016/A1016M), with tolerances typically from ASTM A480/A480M Table A1.1. The defining package for a reviewer is molybdenum 6.0–6.5% together with nitrogen 0.18–0.22%, copper 0.50–1.00%, chromium 19.5–20.5%, and nickel 17.5–18.5% — a superaustenitic chloride-PREN story, not a commodity 316/317 window. Carbon ≤0.020%, sulfur ≤0.010%, and silicon ≤0.80% are tighter than many sister austenitics. Nitrogen analysis method is by agreement (Footnote B). There is no mandatory Nb or Ti band on the public row.
The tables below reproduce the melt limits for UNS S31254, the product-analysis limits from A480 Table A1.1 practice, and a short Mo/N snapshot against TP317LMN and TP316L. Later SA-213 / A213 editions place austenitic stainless grades in Table 2 (older editions used Table 1); confirm the ordered edition on the purchase order. UNCERTAIN: exact edition year and stainless chem table number; A480 product-tolerance digits for Mo 6.0–6.5 and Cu 0.50–1.00 are applied from sister high-Mo / Cu austenitic practice — confirm the A480 edition if product analysis is contractual.
Melting analysis (heat / ladle analysis)
| Element | UNS S31254 melting analysis |
|---|---|
| Carbon (C) | ≤ 0.020 |
| Manganese (Mn) | ≤ 1.00 |
| Phosphorus (P) | ≤ 0.030 |
| Sulfur (S) | ≤ 0.010 |
| Silicon (Si) | ≤ 0.80 |
| Chromium (Cr) | 19.5 – 20.5 |
| Nickel (Ni) | 17.5 – 18.5 |
| Molybdenum (Mo) | 6.0 – 6.5 |
| Nitrogen (N) | 0.18 – 0.22 |
| Copper (Cu) | 0.50 – 1.00 |
| Niobium (Nb) | … (no requirement) |
| Titanium (Ti) | … (no requirement) |
Source: public SA-213 / A213 stainless chemistry table for UNS S31254 (same grade text family; public A213/A213M − 13 excerpt). Molybdenum 6.0–6.5% and nitrogen 0.18–0.22% must both appear on the certificate; an MTC that only shows “254 SMO nickname chemistry” without the SA-213 ranges is incomplete for product acceptance. Where ellipses appear, the ordered edition sets no requirement for that element.
Product analysis — A480/A480M Table A1.1 tolerances applied
| Element | Melting | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.020 | 0.005 over | ≤ 0.025 |
| Manganese (Mn) | ≤ 1.00 | 0.03 over | ≤ 1.03 |
| Phosphorus (P) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Sulfur (S) | ≤ 0.010 | 0.005 over | ≤ 0.015 |
| Silicon (Si) | ≤ 0.80 | 0.05 over | ≤ 0.85 |
| Chromium (Cr) | 19.5 – 20.5 | 0.20 under / over | 19.30 – 20.70 |
| Nickel (Ni) | 17.5 – 18.5 | 0.15 under / 0.20 over | 17.35 – 18.70 |
| Molybdenum (Mo) | 6.0 – 6.5 | 0.10 under / over (UNCERTAIN — confirm A480 edition) | 5.90 – 6.60 |
| Nitrogen (N) | 0.18 – 0.22 | 0.01 under / 0.02 over | 0.17 – 0.24 |
| Copper (Cu) | 0.50 – 1.00 | 0.03 under / over (UNCERTAIN) | 0.47 – 1.03 |
Product analysis is not automatic — order it when the project needs finished-tube chemistry, especially the molybdenum, nitrogen, and copper windows. Read Mo, N, and Cu first: the 6% molybdenum floor drives PREN; nitrogen strengthens and further raises pitting resistance; copper supports the superaustenitic package.
Mo / N snapshot — TP316L / TP317LMN / S31254
| Element | TP316L (S31603) | TP317LMN (S31726) | S31254 |
|---|---|---|---|
| Mo | 2.00 – 3.00 | 4.0 – 5.0 (confirm edition) | 6.0 – 6.5 |
| N | … | 0.10 – 0.20 (confirm edition) | 0.18 – 0.22 |
| Cu | … | … | 0.50 – 1.00 |
| Cr | 16.0 – 18.0 | ~18 – 20 | 19.5 – 20.5 |
| Ni | 10.0 – 14.0 | ~13 – 17 | 17.5 – 18.5 |
Reading tip: a heat that clears TP317LMN still fails S31254 if molybdenum sits near 4–5% or copper is absent. Do not accept a verbal “6Mo / 254 SMO” shop note as proof that the MTC prints S31254 with the Mo, N, and Cu windows satisfied. UNCERTAIN: exact TP317LMN sister digits in the snapshot above — confirm against the ordered edition when comparing grades on a datasheet.
Mechanical Properties of SA213 UNS S31254
Table 4 for UNS S31254 is wall-split: tubes with wall thickness ≤0.187 in. [5 mm] carry a higher tensile floor than thicker walls, while yield, elongation, and hardness stay the same across both rows. That split matters on thin HX tubing datasheets — do not apply the 95 ksi thicker-wall tensile number to a ≤5 mm wall lot, and do not invent a single “98 ksi for all walls” rule when the ordered edition prints both rows.
| Property | Wall ≤ 0.187 in. [5 mm] | Wall > 0.187 in. [5 mm] |
|---|---|---|
| Tensile strength, min | 98 ksi [675 MPa] | 95 ksi [655 MPa] |
| Yield strength (0.2% offset), min | 45 ksi [310 MPa] | 45 ksi [310 MPa] |
| Elongation in 2 in. or 50 mm, min | 35% | 35% |
| Hardness, max | 220 HBW / 230 HV or 96 HRB | 220 HBW / 230 HV or 96 HRB |
Source: public SA-213 / A213 Table 4 for UNS S31254 (same grade text family). Mechanical property requirements generally do not apply to tubing smaller than 1/8 in. [3.2 mm] inside diameter or thinner than 0.015 in. [0.4 mm] wall. Flattening and flaring tests remain lot requirements. A tensile-only MTC that reports a 75/30 checklist against this grade is incomplete documentation practice. Hardness max 220 HBW / 96 HRB is higher than the 192 HBW / 90 HRB commodity austenitic ceiling — expect that on the certificate and do not treat a soft 90 HRB-only template as the S31254 limit. S31254 has no mandatory ASTM grain-size number in the heat-treatment column.
Dimensions and Tolerances
Dimensional supply for ASME SA213 UNS S31254 is tube language — outside diameter × wall thickness (minimum wall or average wall) and, commercially, BWG / gauge — not ASME B36.19 pipe schedules as the primary size story. Usual SA-213 sizes run from about 1/8 in. [3.2 mm] inside diameter to 5 in. [127 mm] outside diameter, with minimum wall from about 0.015 to 0.500 in. [0.4 to 12.7 mm]; other diameters may be furnished when all other requirements are met.
Seawater cooler and chloride-side heat-exchanger datasheets that pick 6Mo S31254 usually assume minimum wall — state wall basis on the purchase order, and remember that the Table 4 tensile floor itself depends on whether wall is ≤ or > 0.187 in. [5 mm]. Outside-diameter and wall variations follow the general requirements invoked by SA-213 (commonly ASTM A1016/A1016M). The Mo/N/Cu package does not change the dimensional tolerance tables; it changes which heat clears the grade stamp.
| Item | Typical SA213 UNS S31254 dimensional practice |
|---|---|
| Product form | Seamless only (cold-finished or hot-finished) |
| Usual size band | ~1/8 in. [3.2 mm] ID to 5 in. [127 mm] OD; wall ~0.015–0.500 in. [0.4–12.7 mm] |
| Wall basis | Minimum wall (common for seawater / chloride HX datasheets) or average wall if PO says so |
| OD / wall tolerance | Per general requirements (commonly A1016/A1016M) for the ordered finish |
| Length | Straight random / cut-to-length; U-bend by agreement |
BWG / gauge callouts are accepted on enquiry; certificates should still show OD and wall in inch or millimetre units. U-bends and polished ID finishes are commercial options — they do not replace the molybdenum, nitrogen, and copper window checks.
Equivalent Grades
Equivalence talk for S31254 should start from the Code Book product standard and the UNS, not from the commercial 254 SMO nickname. ASME SA-213 UNS S31254 is the governing designation on this page. ASTM A213 UNS S31254 is the separate ASTM twin used when dual marking or a non-Code purchase is agreed — it is not a substitute lead standard for an SA-213 order. Related Mo-bearing grades (TP317LMN, TP317LM, TP316L, TP310MoLN) are sister options under the same hub family, not automatic dual stamps.
| Designation | Notes |
|---|---|
| ASME SA-213 / SA-213M UNS S31254 | Governing Code Book seamless boiler / HX tube product standard for this article |
| UNS S31254 | Unified number — no TP letter (Footnote C) |
| 254 SMO / 6Mo (commercial) | Shop / trademark names for the superaustenitic chemistry family — do not replace S31254 on the MTC |
| ASTM A213 UNS S31254 | Separate ASTM product specification — dual-mark only when the PO asks; twin page A213 UNS S31254 |
| Related high-Mo 317 | SA213 TP317LMN — lower Mo than 6.0–6.5%; not interchangeable |
| Related commodity Mo | SA213 TP316L — 2–3% Mo; different PREN story |
| Related plate | A240 / SA240 flat product in the S31254 / 254 SMO family — order plate and tube under their own standards |
Hub entry point: SA213/SA213M. When a bill of materials only says “254 SMO,” ask whether Mo 6.0–6.5%, N 0.18–0.22%, and Cu 0.50–1.00% are actually required before shipping S31254 or a TP317LMN alternative.
Heat Treatment and Delivery Condition
UNS S31254 under ASME SA-213 is furnished solution treated at a minimum of 2100 °F [1150 °C], then quenched in water or cooled rapidly by other means. That anneal temperature sits well above the 1900 °F commodity austenitic minimum — do not apply a generic “solution anneal 1900 °F” stamp to an S31254 heat. Public Table 3 for S31254 does not print a mandatory grain-size number (ellipsis), so H-grade grain-size framing does not apply.
Cold-finished versus hot-finished is a process and dimensional route, not a second product standard. Both routes still require the 2100 °F solution treatment on finished tube. High-Mo superaustenitics need a thorough, hot enough anneal so molybdenum and nitrogen stay in solution rather than forming unwanted phases that cut toughness or corrosion performance. Delivery condition for SHH STEEL S31254 is solution annealed and pickled (or bright annealed by agreement), with anneal temperature and quench method on the EN 10204 3.1 certificate. Straightening, cutting, and end finishing follow heat treatment.
UNCERTAIN: confirm ordered-edition footnote attachment near the S31254 heat-treatment row (public OCR does not show Footnote F on that line the way some sister rows do). If a later edition attaches quench / A262 capability language, follow the ordered text rather than inventing S4 test obligations that the edition does not require. If a project datasheet asks for an E112 grain-size report, put that supplementary requirement on the purchase order.
Corrosion Resistance
S31254 under ASME SA-213 is selected primarily for high PREN chloride, seawater-side, and aggressive aqueous heat-exchanger duty associated with the 6% molybdenum floor plus nitrogen and copper — not as a dry high-temperature oxidation upgrade over TP310S. The Mo 6.0–6.5% band with N 0.18–0.22% and Cu 0.50–1.00% supports pitting and crevice resistance far above commodity 316L / 317L in many chloride-bearing services, which is why the grade is ordered for seawater coolers and process condensers that reject 316-family tubes.
Where a datasheet mixes “254 SMO” with dry furnace oxidation or carburization duty, ask whether the service is actually looking for a high-Si / Ce–N / 310-family tube instead of a 6Mo superaustenitic. SHH STEEL will not treat a molybdenum PMI peak alone as proof of full S31254 compliance — Mo, N, and Cu windows, heat treatment at 2100 °F, and the intended medium have to be read together. For lower-Mo nitrogen-bearing framing open SA213 TP317LMN.
Applications of SA213 UNS S31254 Tube
Typical ASME SA213 UNS S31254 placements are Code-stamped seawater coolers, chloride-side heat exchangers, and process condensers where the material list names S31254 or explicitly requires Mo 6.0–6.5% with N 0.18–0.22% and Cu 0.50–1.00% — not generic “316L,” “317LMN,” or “6Mo nickname” replacements. Bundles that already distinguish 254 SMO-class chemistry from TP317LMN are the natural fit.
When the enquiry only says “254 SMO” without UNS language, confirm whether the buyer actually needs SA213 TP317LMN, SA213 TP316L, or another Mo-bearing grade before substituting. SHH STEEL quotes S31254 when the enquiry names the UNS or the Mo/N/Cu package explicitly.
Weldability
S31254 welds as a high-molybdenum, nitrogen-bearing superaustenitic. Filler selection should respect the 6% molybdenum floor and the nitrogen / copper package rather than copying a plain ER316L procedure without review. Matching or near-matching 6Mo / superaustenitic fillers (often over-alloyed in Mo and N relative to the base metal) are the usual starting point; confirm chemistry against the WPS when the project treats Mo/N/Cu as contractual on the weld metal as well as the tube.
Autogenous welds and thin-wall HX joints need heat-input control and careful interpass practice to protect the as-annealed superaustenitic condition near the HAZ. Post-weld heat treatment is not a default SA-213 requirement for this grade — if the vessel code or the buyer wants a separate resolution anneal after welding, write that as a negotiated step at a temperature that respects the 2100 °F solution-treatment floor. SHH STEEL can coordinate weld coupons when the PO asks.
Surface Finishes
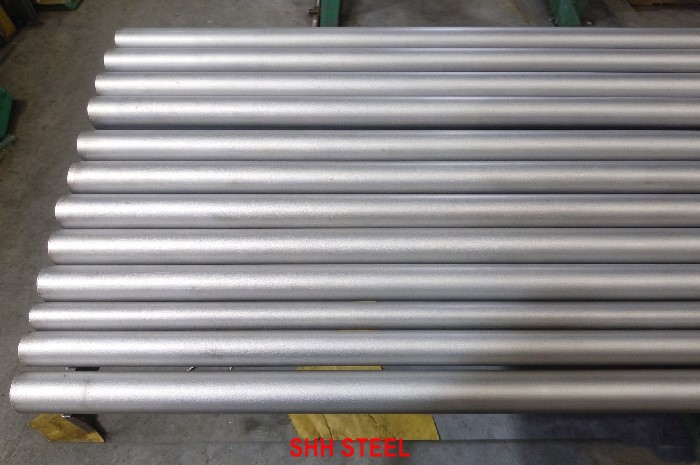
Standard mill delivery for ASME SA213 UNS S31254 is solution annealed and pickled, leaving a clean matte finish suitable for seawater cooler and chloride-side heat-exchanger tube duty. Bright annealing is available by agreement when OD appearance or polish steps favor it.
ID/OD polish and U-bend conditioning are commercial additions — they do not replace the molybdenum, nitrogen, and copper window checks. End caps and dry export packaging matter more than paint on pickled stainless. SHH STEEL notes the ordered surface route on the packing list and aligns it with the MTC finish description for receiving inspection.
Inspection and Testing
Base ASME SA-213 testing for UNS S31254 includes heat analysis (C ≤0.020%, Cr 19.5–20.5%, Ni 17.5–18.5%, Mo 6.0–6.5%, N 0.18–0.22%, Cu 0.50–1.00%, Mn ≤1.00%, Si ≤0.80%, P ≤0.030%, S ≤0.010%), tension tests to the wall-appropriate 98/45 or 95/45 ksi floors with 35% elongation, hardness to 220 HBW / 96 HRB, and flattening / flaring tests for the ordered size. Hydrostatic testing or NDE follows the path selected on the purchase order.
Certificate reviewers should confirm the molybdenum, nitrogen, and copper windows — and which wall-split tensile row applies — rather than trusting a “254 SMO” shop nickname or a 316-family PMI without Mo ≥6.0%. Product analysis, when ordered, applies A480 tolerances with Mo and Cu digits noted as UNCERTAIN above if the ordered A480 edition differs. EN 10204 3.1 is default; 3.2 when required. Dual SA-213/A213 names appear only when dual marking was ordered.
Packaging and Shipping
S31254 tube leaves SHH STEEL bundled, capped or end-protected, and tagged for export or domestic delivery according to length mix and bend form. Bundle tags repeat ASME SA-213 UNS S31254, heat number, size, and wall basis so receivers can match the 3.1 certificate — including Mo, N, and Cu — without opening every bundle.
Export packing uses seaworthy bundling appropriate for pickled stainless. Marking follows SA-213 and any dual-mark text the PO adds, referencing A213 UNS S31254 only when dual ASTM marking was ordered. The commercial 254 SMO nickname may appear in packing notes for routing, but the stencil and MTC still carry UNS S31254.
Why Choose SHH STEEL
SHH STEEL treats ASME SA213 UNS S31254 as a Code Book 6Mo superaustenitic product with enforceable C ≤0.020%, Cr 19.5–20.5%, Ni 17.5–18.5%, Mo 6.0–6.5%, N 0.18–0.22%, Cu 0.50–1.00%, wall-split 98/45 or 95/45 ksi tensile, 35% elongation, hardness max 220 HBW / 96 HRB, 2100 °F anneal, and marking rules — not as “317LMN with a trademark sticker” checked only by a Mo PMI peak. Enquiry review verifies the molybdenum, nitrogen, and copper windows before release.
That stops silent substitution with TP317LMN or TP316L heats on datasheets that actually require S31254. We keep SA-213 and A213 independent, dual-mark only on request, and put Mo, N, and Cu on the 3.1 certificate so inspectors can verify the grade. The commercial 254 SMO nickname is allowed for routing — it never replaces S31254 on the MTC.
Cross-links: SA213 TP317LMN, SA213 TP316L, SA213 TP317LM, hub SA213/SA213M.
Supply Capability
SHH STEEL can supply ASME SA213 UNS S31254 stainless steel tube against the edition and finish route named on your enquiry. The capability table below summarizes sizes, finishes, and documents we regularly quote, followed by the Stock / Available sizes map for 6Mo seawater cooler and chloride-side heat-exchanger tube.
| Item | SHH STEEL capability for UNS S31254 |
|---|---|
| Standard | ASME SA213 / SA213M (dual A213 marking on request) |
| Grade | UNS S31254 (no TP letter) |
| Product form | Seamless only — cold-finished and hot-finished |
| Size | Typical OD × min wall (or average wall) in the SA-213 usual band; other diameters by agreement |
| Wall / gauge | Minimum wall or average wall; BWG / gauge callouts accepted on enquiry; note Table 4 wall-split at 0.187 in. [5 mm] |
| Length | Cut-to-length for seawater / chloride HX bundles; U-bend by agreement |
| Documentation | EN 10204 3.1 MTC with Mo / N / Cu windows; witness on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
Stock / Available sizes
SHH STEEL quotes S31254 against a stock-and-mill enquiry range rather than a frozen SKU or tonnage list. Representative OD × wall / BWG combinations below are an enquiry map for 6Mo seawater cooler and chloride-side heat-exchanger tube — confirm live availability and cut lengths on the RFQ.
| OD (in.) | Typical wall / BWG enquiry band | Notes |
|---|---|---|
| 1/2 – 1 | BWG 16–12 / ~0.065–0.109 in. | Small HX / cooler sizes (often ≤5 mm wall → 98 ksi row) |
| 1-1/4 – 2 | BWG 14–10 / ~0.083–0.134 in. | Common seawater / chloride HX band |
| 2-1/2 – 3 | 0.120 – 0.250 in. min wall | Heavier HX wall — check ≤/> 0.187 in. tensile split |
| 3-1/2 – 5 | 0.180 – 0.300 in. min wall | Upper usual SA-213 OD by agreement |
Send OD × wall (or BWG), wall basis, quantity, length mix, finish route, and any dual-mark needs with the RFQ so we can align mill capacity to the Mo/N/Cu package and the correct Table 4 wall-split row on the first reply.
FAQ
-
Is ASME SA-213 the same as ASTM A213 for UNS S31254?
- No. ASME SA-213 / SA-213M is the ASME Code Book adoption; ASTM A213 / A213M is the separate ASTM product specification. Chemistry — including C ≤0.020%, Cr 19.5–20.5%, Ni 17.5–18.5%, Mo 6.0–6.5%, N 0.18–0.22%, and Cu 0.50–1.00% — wall-split tensile 98/45 or 95/45 ksi, elongation 35%, and hardness floors align in the shared grade text family, but the standards remain independent documents. Dual marking is a purchase-order option, not proof that the two titles are one standard.
-
Does ASME SA213 UNS S31254 have a TP grade letter?
- No. S31254 appears in the stainless chemistry table without a TP letter (Footnote C practice). Order and mark by UNS S31254 under ASME SA-213 / SA-213M. Do not invent a “TP31254” stencil or assume the grade dual-stamps as TP317LMN or TP316L. The purchase order and MTC should carry the UNS designation explicitly so inspectors can match Mo, N, Cu, and the wall-split tensile row to the correct grade.
-
Is 254 SMO the same as ASME SA213 UNS S31254?
- 254 SMO is a commercial / trademark shop name for the 6Mo superaustenitic chemistry family around S31254. It is useful for routing, but it does not replace ASME SA-213 UNS S31254 on the purchase order or the MTC. SHH STEEL will stencil and certify UNS S31254; packing notes may mention 254 SMO only as a buyer routing aid when requested. Always confirm Mo 6.0–6.5%, N 0.18–0.22%, and Cu 0.50–1.00% against the certificate.
-
How does S31254 differ from TP317LMN under SA-213?
- S31254 requires molybdenum 6.0–6.5%, nitrogen 0.18–0.22%, and copper 0.50–1.00%, with wall-split tensile floors of 98/45 or 95/45 ksi and a 2100 °F anneal. TP317LMN is a lower-Mo nitrogen-bearing 317-family grade with a different tensile set and no mandatory copper window on the same scale. They are related high-Mo concepts, not dual stamps. Do not accept a TP317LMN certificate as S31254 clearance.
-
Why does Table 4 split tensile for S31254 by wall thickness?
- The public grade text sets 98 ksi [675 MPa] tensile for wall ≤0.187 in. [5 mm] and 95 ksi [655 MPa] for thicker walls, while yield stays at 45 ksi and elongation at 35% for both. Thin HX tubing datasheets must use the higher row; thicker walls must not invent a single 98 ksi rule. State wall on the RFQ so the mill applies the correct Table 4 line and the certificate matches the ordered size.
-
What hardness limit applies to ASME SA213 UNS S31254 tube?
- Table 4 caps S31254 hardness at 220 HBW / 230 HV or 96 HRB — higher than the 192 HBW / 90 HRB commodity austenitic ceiling. Hardness is checked together with the wall-appropriate tensile set and 35% elongation. A hardness result alone does not prove Mo/N/Cu compliance; certificate reviewers should still read the molybdenum, nitrogen, and copper windows on the MTC.
-
What heat treatment applies to SA213 UNS S31254?
- Solution treatment at a minimum of 2100 °F [1150 °C] followed by rapid cooling is the public path — notably hotter than the 1900 °F commodity austenitic minimum. There is no mandatory ASTM grain-size number for this grade in the public heat-treatment column. Footnote F / A262 attachment on the ordered edition is UNCERTAIN — confirm against the Code Book text named on the PO before assuming S4 test obligations.
-
Should I order minimum wall or average wall for S31254?
- Seawater cooler and chloride-side heat-exchanger datasheets that pick S31254 usually assume minimum wall. Average wall is acceptable when the purchase order says so and the general requirements for the ordered finish are applied. State wall basis, OD × wall or BWG, and length mix on the RFQ — and note which Table 4 wall-split tensile row applies — so the mill does not default to a basis your inspector will reject.
-
Does ASME SA213 UNS S31254 cover welded or HCW tube?
- No. ASME SA-213 for this stainless series is a seamless boiler, superheater, and heat-exchanger tube product standard. SHH STEEL supplies S31254 as seamless cold-finished or hot-finished tube only. Welded (WLD) or heavily cold-worked welded (HCW) manufacturing types are outside this page’s product form and are not offered as a Manufacturing Types split under the SA213 UNS S31254 listing.
-
Can SHH STEEL dual-certify SA-213 and A213 for S31254?
- Yes, when the purchase order asks for dual marking and the heat meets both product standards’ grade text for UNS S31254. Dual marking is a documentation and stencil option — it does not merge the two standards into one title. For non-Code purchases that only want the ASTM twin, see A213 UNS S31254; for Code-led work, keep SA-213 as the lead standard on the PO.
-
Is S31254 a drop-in replacement for TP316L in chloride service?
- Not as a silent drop-in. S31254 is a 6Mo superaustenitic with far higher PREN framing than TP316L’s 2–3% molybdenum window, a different tensile set, and a 2100 °F anneal. It is often the correct upgrade when chloride or seawater duty has rejected 316L, but the purchase order must name UNS S31254 explicitly — chemistry, tensile, hardness, and heat treatment all change. Do not stencil 316L heats as S31254.
Conclusion
ASME SA213 UNS S31254 is the 6Mo / 254 SMO class superaustenitic seamless stainless steel tube grade for Code seawater cooler, chloride-side heat-exchanger, and related boiler / HX service when C ≤0.020%, Cr 19.5–20.5%, Ni 17.5–18.5%, Mo 6.0–6.5%, N 0.18–0.22%, Cu 0.50–1.00%, wall-split 98/45 or 95/45 ksi tensile with 35% elongation, hardness max 220 HBW / 96 HRB, and a 2100 °F [1150 °C] solution anneal are required together. SHH STEEL supplies cold-finished and hot-finished seamless tube in the usual OD × wall / BWG band with EN 10204 3.1 MTCs that report the Mo, N, and Cu windows. The commercial 254 SMO nickname does not replace UNS S31254 on the certificate. For quotations and technical review, contact admin@steelspecs.com.
Quality Steel Needed? Inquire for Offers
Related Products