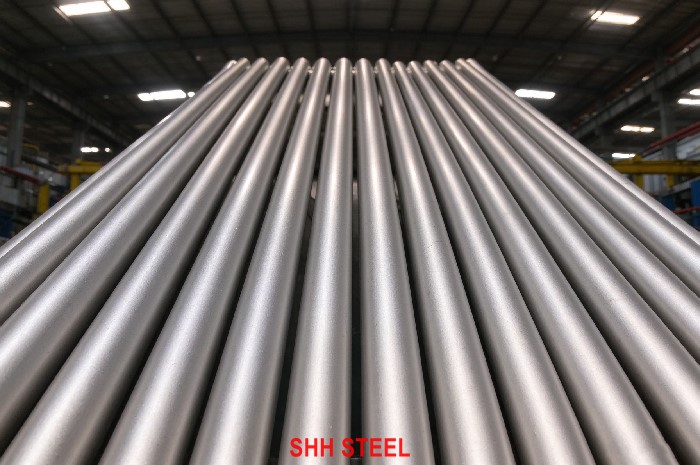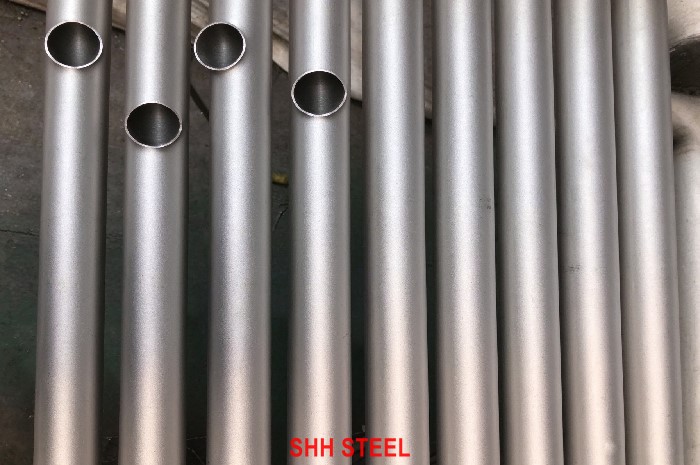
ASME SA312 UNS S32053 Stainless Steel Pipe | SA 312/SA 312M
What is ASME SA312 UNS S32053 Stainless Steel Pipe
ASME SA-312/SA-312M covers seamless, welded, and heavily cold-worked austenitic stainless steel pipe for high-temperature and general corrosive service. UNS S32053 appears in Table 1 with no TP designation, so the pipe is ordered, stencilled, and certified by its UNS number alone. It is a high-nickel, high-chromium superaustenitic with 5–6% molybdenum and nitrogen. The Table 1 melting analysis is C ≤0.03%, Mn ≤1.00%, P ≤0.030%, S ≤0.010%, Si ≤1.00%, Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, with no copper requirement. The combination of 5–6% Mo, 0.17–0.22% N, and a 24–26% nickel base is what defines the grade: high pitting resistance with a stable fully austenitic structure.
Table 4 sets a single tensile row of 93 ksi [640 MPa] tensile and 43 ksi [295 MPa] yield, with 35% longitudinal and 25% transverse elongation. For heat treatment, Table 2 lists S32053 together with S31727 at 1975–2155 °F [1080–1180 °C] with rapid cooling, which is above the 1900 °F default (the Table 2 pairing was read from a two-column layout and is noted in the uncertainty file). UNS S32053 is not an H grade, so there is no carbon floor, no Table 5 grain-size rule, and no H-grade reheat clause. Table 6 does not clearly assign an AWS filler class to S32053 in the extract used for this page, so the consumable is by agreement. Industry practice for 5–6% Mo superaustenitics is an overalloyed Ni-Cr-Mo filler, but the class must be qualified on S32053 and frozen on the WPS. The usual service niche is severe chloride process duty, hot brines, and aggressive chemical streams where the designer wants 6Mo-class pitting resistance on a higher-nickel base for structural stability.
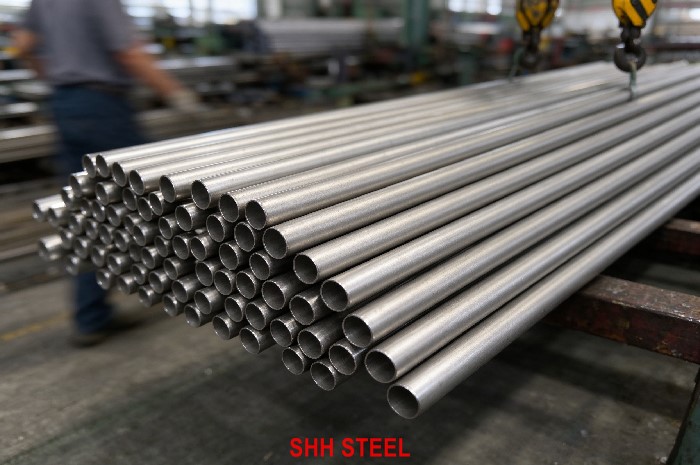
SHH STEEL can supply ASME SA312 UNS S32053 stainless steel pipe to the edition named on your enquiry, in seamless (SML), welded (WLD), and heavily cold-worked (HCW) routes. We work to ASME B36.19 schedules and to special OD and wall combinations by agreement, issue EN 10204 3.1 mill test certificates that report the full Table 1 row including Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, and can dual-mark SA-312/A312 when heat analysis, anneal, mechanical tests, and marking satisfy both editions on the purchase order. Tell us NPS, wall or schedule, finish, length, and any supplementary tests when you enquire.
Common commercial names and how they map to the ordered product are listed below. Market shorthand is useful in conversation, but the purchase order and certificate should always carry the full SA-312/A312 designation plus UNS S32053 so receiving inspection has one unambiguous identity to check.
- ASME SA312 UNS S32053 — preferred marking for ASME-code and dual-marked pipe (no TP name exists)
- ASTM A312 UNS S32053 — same Table 1 and Table 4 rows when the ASTM edition is referenced
- Proprietary superaustenitic trade names — map any brand name back to UNS S32053 and check the full Table 1 row
- ASTM A312 UNS S32053 — same Table 1 / Table 4 when the ASTM edition is referenced
UNS S32053 is not a drop-in for ASME SA312 UNS S31254 Stainless Steel Pipe, ASME SA312 UNS S31266 Stainless Steel Pipe, or ASME SA312 UNS S31727 Stainless Steel Pipe, even though these grades often appear together on the same bid list. Versus S31254, S32053 runs higher chromium and nickel (22–24% and 24–26% vs 19.5–20.5% and 17.5–18.5%), slightly lower molybdenum (5.0–6.0% vs 6.0–6.5%), no copper range, a single 93/43 ksi tensile row, and the 1975–2155 °F anneal instead of 2100 °F minimum. Versus S31266, it has no tungsten and a lower strength floor. Versus S31727, it is a much richer alloy with no copper requirement, though the two share the same Table 2 anneal window. Each has its own Table 1 row and Table 4 floor, so dual marking across them is rarely possible. For the full family overview see the ASME SA 312/SA 312M hub.
Manufacturing Types (SML / WLD / HCW)
ASME SA-312 allows three manufacturing routes for UNS S32053, and the choice is a purchase-order decision driven by design code, size, wall thickness, and inspection preference. The route never changes the chemistry: every heat must still meet Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22% together with the rest of the Table 1 row, and every length must be solution annealed at 1975–2155 °F [1080–1180 °C] with rapid cooling before it leaves the mill.
- Seamless (SML) — no welding at any stage. Usually preferred for heavier walls, smaller diameters, and critical process lines where the project specification excludes welded pipe.
- Welded (WLD) — made from UNS S32053 strip or plate by automatic welding without filler metal, then annealed. Practical and economical for larger diameters and thinner walls, provided the plate heat itself meets the UNS S32053 row.
- Heavily cold-worked (HCW) — welded pipe cold worked at least 35% in wall and weld before the final anneal, with the weld radiographed before cold work. Ordered when the buyer wants that route and its marking.
Every finished length is hydrostatically tested or nondestructively electrically tested, and the mill may choose the method unless the purchase order fixes one. Pipe NPS 10 and larger may be marked “NH” only when the purchaser agrees to a system test instead. In practice UNS S32053 is a made-to-order grade at most mills, with minimum melt quantities above those of commodity TP316L or TP317L, so grouping project sizes onto one heat helps both lead time and chemistry consistency. Confirm the route, edition, wall basis, and any corrosion or supplementary tests before the mill order is placed so the certificate matches the design basis.
Chemical Composition of SA312 UNS S32053
Melting analysis (heat / ladle analysis) — Table 1
Heat analysis for UNS S32053. Values are maximum unless a range is shown; ellipses (…) mean no requirement.
| Element | UNS S32053 melting analysis |
|---|---|
| Carbon (C) | ≤ 0.03 |
| Manganese (Mn) | ≤ 1.00 |
| Phosphorus (P) | ≤ 0.030 |
| Sulfur (S) | ≤ 0.010 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 22.0 – 24.0 |
| Nickel (Ni) | 24.0 – 26.0 |
| Molybdenum (Mo) | 5.0 – 6.0 |
| Nitrogen (N) | 0.17 – 0.22 |
Source: SA-312 Table 1, UNS S32053. No Cu requirement (ellipsis).
Product analysis — A480/A480M Table A1.1 tolerances applied to Table 1
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.03 | 0.005 over | ≤ 0.035 |
| Manganese (Mn) | ≤ 1.00 | 0.03 over | ≤ 1.03 |
| Phosphorus (P) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Sulfur (S) | ≤ 0.010 | 0.005 over | ≤ 0.015 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 22.0 – 24.0 | 0.25 under / over | 21.75 – 24.25 |
| Nickel (Ni) | 24.0 – 26.0 | 0.20 under / over | 23.80 – 26.20 |
| Molybdenum (Mo) | 5.0 – 6.0 | 0.10 under / over | 4.90 – 6.10 |
| Nitrogen (N) | 0.17 – 0.22 | 0.01 under / 0.02 over | 0.16 – 0.24 |
Vs S31254: higher Cr/Ni; Mo 5–6 vs 6.0–6.5; no Cu range; different tensile and anneal. Vs S31727: no Cu 2.8–4; much higher Cr/Ni/Mo; 93/43 vs 80/36. Mo ±0.10 on 5–6%. N 0.01 under / 0.02 over on 0.17–0.22. Mn ≤1.00 with +0.03. Ni uses 0.20 band (20–30%).
When reviewing a certificate for UNS S32053, check every element in the Table 1 row rather than only chromium and nickel. The elements that define this grade, Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, are exactly the ones a commodity 300-series heat will miss, and a missing or out-of-range value is a nonconformance even when tensile results look good. Product analysis, when ordered, is judged against the A480 tolerances shown above. Designers should take allowable stresses only from the governing code tables listed for UNS S32053, not from a neighbouring grade.
Mechanical Properties of SA312 UNS S32053
| Property | S32053 |
|---|---|
| Tensile, min | 93 ksi [640 MPa] |
| Yield, min | 43 ksi [295 MPa] |
| Elongation | 35% L / 25% T |
Source: SA-312 Table 4 for UNS S32053. One tensile row applies regardless of wall thickness; no hardness maximum is asserted here and there is no Table 5 grain-size requirement because UNS S32053 is not an H grade.
The 93/43 ksi minimums are the values your receiving inspector should look for on the MTC, and they are not interchangeable with sister rows: S31725 is 75/30, S31726 is 80/35, S31727 is 80/36, S31730 is 70/25, and S32053 is 93/43 ksi. Base testing covers tension on a lot basis, flattening on a sample of lengths, and hydrostatic or electric testing of every length. Elevated-temperature tensile, impact, and hardness limits are purchase-order or construction-code options rather than base SA-312 requirements, so write them on the order if your piping class needs them.
Like other austenitics, UNS S32053 work-hardens during cold bending or expanding, so severe forming may need an intermediate anneal that again meets the 1975–2155 °F [1080–1180 °C] practice. For pressure design, use the allowable stresses listed for UNS S32053 in the governing Section II Part D or project-code tables; copying TP316L or TP317L allowables into the calculation package is a common and avoidable error.
Dimensions and Tolerances
Dimensional supply for UNS S32053 pipe follows ASME B36.19 schedules for the common NPS and schedule combinations, with special OD and wall by agreement when an exchanger, header, or process skid needs a non-standard section. Outside-diameter variations follow ASTM A999/A999M, and wall-thickness variations follow SA-312 Table 3 as summarised below. State on the order whether wall is nominal or minimum (Supplementary S8), so the mill rolls to the interpretation your design assumed.
| NPS designator | Wall over | Wall under |
|---|---|---|
| 1/8 to 2-1/2 incl., all t/D | 20.0% | 12.5% |
| 3 to 18 incl., t/D up to 5% | 22.5% | 12.5% |
| 3 to 18 incl., t/D over 5% | 15.0% | 12.5% |
| 20 and larger, welded, all t/D | 17.5% | 12.5% |
| 20 and larger, seamless, t/D up to 5% | 22.5% | 12.5% |
| 20 and larger, seamless, t/D over 5% | 15.0% | 12.5% |
Source: SA-312 Table 3; outside diameter variations per A999/A999M.
- Lengths — single random, double random, or cut-to-length by agreement
- Cut lengths — typically no more than 1/4 in. [6 mm] over unless a tighter band is ordered
- Ends — plain or beveled; confirm bevel angle and root face when the WPS is already frozen
Many chemical-process buyers order UNS S32053 by OD × wall rather than by NPS and schedule, especially for exchanger and instrument lines. For thin schedules with socket-weld or threaded ends, check that the remaining wall is still adequate after the 12.5% under-tolerance. Jointers are not permitted unless the order allows them, and cut-to-length programmes should include an allowance for fit-up scrap so pieces do not arrive short.
Equivalent Grades
Equivalence for UNS S32053 is mainly an ASME/ASTM identity question. The governing pipe designation is ASME SA-312 UNS S32053, and any trade name, European number, or plate counterpart has to be mapped back to that Table 1 row before a mill is asked to dual-mark or substitute.
| Designation | Notes |
|---|---|
| ASME SA-312 UNS S32053 | Governing pipe grade (no TP designation) |
| ASTM A312 UNS S32053 | Same Table 1 / Table 4 when the ASTM edition is referenced |
| Proprietary superaustenitic trade names | map any brand name back to UNS S32053 and check the full Table 1 row |
| ASTM A312 UNS S32053 | same Table 1 / Table 4 when the ASTM edition is referenced |
| SA-240 / A240 UNS S32053 | Plate and sheet counterpart where listed—not a pipe specification |
Related SA-312 grades on steelspecs.com include ASME SA312 UNS S31254 Stainless Steel Pipe, ASME SA312 UNS S31266 Stainless Steel Pipe, and ASME SA312 UNS S31727 Stainless Steel Pipe. These pages sit close together because buyers often compare them, but none of them is an automatic equivalent of UNS S32053. European numbers and brand names are engineering maps only; if a project specification quotes one, ask the mill to certify against the SA-312 UNS S32053 row and list any extra European requirements separately on the order.
Heat Treatment and Delivery Condition
All SA-312 pipe is delivered in the solution-annealed condition. For UNS S32053, Table 2 lists S32053 together with S31727 at 1975–2155 °F [1080–1180 °C] with rapid cooling, which is above the 1900 °F default (the Table 2 pairing was read from a two-column layout and is noted in the uncertainty file). Because the grade is not an H grade, there is no grade-specific heat-treatment lot marking requirement and no grain-size test, but most process projects still ask for heat and lot identity on the stencil so traceability survives fabrication.
- Solution anneal at 1975–2155 °F [1080–1180 °C] — followed by rapid cooling in water or by other rapid means
- No Table 5 grain-size rule — not an H grade
- Pickled and passivated — free of scale and embedded iron, which matters for crevice resistance
- Bright anneal — available by agreement when the end user requires a scale-free surface
The anneal temperature should be stated on the MTC, not just the words “solution annealed”, so that inspection can verify it against the 1975–2155 °F [1080–1180 °C] requirement. Rapid cooling is what keeps the high-alloy structure free of chromium carbides and molybdenum-rich intermetallic phases, so a slow furnace cool is not acceptable even if tensile results pass. If pipe is hot-formed or heavily cold-formed during fabrication, plan a re-anneal to the same practice before it goes into corrosive service.
Corrosion Resistance
UNS S32053 is chosen for severe chloride process duty, hot brines, and aggressive chemical streams where the designer wants 6Mo-class pitting resistance on a higher-nickel base for structural stability. The combination of 5–6% Mo, 0.17–0.22% N, and a 24–26% nickel base is what defines the grade: high pitting resistance with a stable fully austenitic structure. SA-312 does not publish corrosion rates or critical pitting temperatures for any grade, so the selection must be backed by process-licensor data, published alloy data, or project testing rather than by the specification itself.
In practice, most corrosion failures in this class of alloy trace back to fabrication rather than base-metal chemistry: heat tint left on weld roots, iron contamination from carbon-steel tools, chloride-bearing insulation, and crevices under gaskets or deposits. Ask for pickled and passivated delivery, keep UNS S32053 apart from carbon steel in storage and fabrication, and remove weld oxide before commissioning. When the corrosion case needs proof, order Supplementary S7 intergranular testing (ASTM A262 Practice E) or a project pitting test such as ASTM G48; neither is automatic under SA-312.
Applications of SA312 UNS S32053 Pipe
Buyers usually arrive at UNS S32053 after a corrosion review has ruled out commodity 316L or 317L but has not justified the cost of a nickel alloy. The table below shows typical uses; every application still needs confirmation of temperature, concentration, and chloride level against real data.
| Application | Why UNS S32053 | Note |
|---|---|---|
| Chemical and acid process lines | Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22% | Confirm concentration and temperature |
| Flue-gas and scrubber systems | Chloride-bearing condensate | Watch deposits and crevices |
| Pulp and paper liquors | Mixed chloride and oxidising chemistry | Compare with sister UNS rows |
| Heat exchanger and instrument piping | Corrosion margin over 317L | Often seamless, ordered by OD × wall |
If only moderate chloride resistance is needed, ASME SA312 TP317L Stainless Steel Pipe or ASME SA312 TP316L Stainless Steel Pipe are usually easier to source and cheaper. If the duty calls for full 6Mo performance, compare ASME SA312 UNS S31254 Stainless Steel Pipe before stretching a leaner heat into service it was not designed for. The right grade is the one your corrosion engineer and the governing code both support, and we are happy to quote alternatives side by side.
Weldability
UNS S32053 welds well with GTAW, GMAW, and SMAW when the procedure is qualified on the actual grade. Table 6 does not clearly assign an AWS filler class to S32053 in the extract used for this page, so the consumable is by agreement. Industry practice for 5–6% Mo superaustenitics is an overalloyed Ni-Cr-Mo filler, but the class must be qualified on S32053 and frozen on the WPS. Mill longitudinal welds on WLD and HCW pipe are autogenous, so the filler question applies only to fabrication welds.
Good practice for this alloy class is low heat input, controlled interpass temperature (commonly 150 °C or below), full back-purging with argon to keep the root bright, and removal of heat tint by pickling or mechanical cleaning. Molybdenum segregates in autogenous weld metal, so overalloyed filler is normally used for corrosion-critical joints rather than fusing the root without filler. Dissimilar joints to carbon steel need a transition procedure approved by the piping engineer.
Surface Finishes
Standard delivery for UNS S32053 is annealed and pickled, which gives a clean matte surface free of scale and embedded iron. Other finishes are available by agreement and should be written on the order with a clear measurement basis.
- Annealed and pickled (AP) — standard process-piping finish
- Bright annealed — scale-free surface from a protective atmosphere
- Mechanically polished or electropolished — by agreement, with Ra target and OD/ID scope stated
For corrosion-critical service, the finish is less about appearance than about removing anything that could start a pit or crevice. If you need a polished or electropolished ID, specify the Ra value, whether it applies to OD, ID, or both, and whether it is measured before or after passivation, so that both mill and inspector are working to the same number.
Inspection and Testing
Base SA-312 testing for UNS S32053 covers heat analysis, tension tests, flattening tests, and hydrostatic or nondestructive electric testing of every length. Supplementary requirements such as product analysis, ultrasonic or radiographic weld examination, intergranular corrosion testing, or third-party witness apply only when written on the purchase order.
- Chemistry — full Table 1 row on the MTC, including Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%
- Tensile — 93/43 ksi with 35% L / 25% T elongation
- Heat treatment — actual anneal temperature against 1975–2155 °F [1080–1180 °C]
- Integrity — hydrostatic or electric test result for each length
- Options — PMI, EN 10204 3.2, S7 / G48 corrosion tests, UT/RT of welds
We recommend a positive material identification check on receipt for any UNS S32053 order, because the distinguishing elements are easy to verify with a portable analyser and a mixed-up length is far cheaper to catch before fabrication than after. When a third-party inspector is required, book the witness before final testing so the inspector sees the actual lengths being tested.
Packaging and Shipping
UNS S32053 pipe is packed to protect both the surface and the identity of each length. Typical export packing uses plastic end caps, wrapping or woven bags, and seaworthy wooden cases or bundles with stainless or non-metallic strapping, with heat number, size, and grade marked on each package.
- Marking — SA-312 UNS S32053, manufacturing type, size, heat number, and edition on every length
- Segregation — kept apart from carbon steel and from sister UNS grades in the same shipment
- Documents — packing list and MTC numbers matching the stencil
Because several grades in this family look identical on the rack, we keep UNS S32053 physically separated from ASME SA312 UNS S31254 Stainless Steel Pipe and ASME SA312 UNS S31266 Stainless Steel Pipe during packing and list each heat on the packing list. On arrival, receiving staff should check stencil, packing list, and certificate against each other before the pipe enters the fabrication shop.
Why Choose SHH STEEL
Grades like UNS S32053 are where specification detail decides whether a shipment is accepted. SHH STEEL reads the Table 1, Table 2, and Table 4 rows for the exact UNS on your enquiry, checks mill offers against them before quoting, and tells you openly where the standard is silent, such as Table 6 filler assignments, rather than filling gaps with guesses. Our aim is a certificate package your inspector can clear on the first review.
- Specification fidelity — full Table 1 reporting including Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, correct 93/43 ksi row, and anneal at 1975–2155 °F [1080–1180 °C]
- Mill sourcing — made-to-order melts for specialty UNS grades, with remnant stock checked for urgent small lots
- Certification — EN 10204 3.1 as standard, 3.2 and third-party witness by agreement, dual SA-312/A312 when both editions are met
- Honest limits — we state where SA-312 is silent and where a sister grade would serve you better
- Export packing — capped, segregated, and documented for ocean freight
Supply Capability
We supply ASME SA312 UNS S32053 pipe for project and maintenance orders, from single lengths for replacement work to full heats for new process units. The summary below shows our normal range; anything outside it can usually be arranged by agreement with the mill.
| Item | Capability |
|---|---|
| Grade | ASME SA312 / ASTM A312 UNS S32053 (no TP designation) |
| Manufacturing types | Seamless (SML), welded (WLD), heavily cold-worked (HCW) |
| Sizes | ASME B36.19 schedules plus special OD × wall by agreement |
| Heat treatment | Solution annealed at 1975–2155 °F [1080–1180 °C], rapid cooled |
| Certification | EN 10204 3.1; 3.2 / third-party by agreement |
| Testing options | PMI, product analysis, UT/RT, S7 / G48 corrosion tests |
Because UNS S32053 is rarely held as open stock, most orders are made to order, and lead time depends on the next available melt campaign. Small urgent quantities can sometimes be met from remnant lengths of earlier certified heats, so it is always worth asking. Send us the edition, sizes, quantities, manufacturing type, and any supplementary tests, and we will come back with a clear offer and delivery estimate.
FAQ
-
Is ASME SA312 the same as ASTM A312?
- For chemistry (Table 1), tensile (Table 4), manufacturing types, and most testing language, ASME SA-312/SA-312M matches ASTM A312/A312M of the referenced edition. Dual SA312/A312 marking of UNS S32053 is common when ordered. Name both editions on the purchase order and the mill test certificate so inspectors can verify the heat against the exact books you cited.
-
What is the UNS number for this grade, and is there a TP name?
- Table 1 lists S32053 as the unified number for this pipe grade with an ellipsis in the TP column, so there is no TP designation. Cite UNS S32053 on the purchase order, stencil, packing list, and mill test certificate so that chemistry and tensile rows cannot be confused with a neighbouring grade that shares a similar commercial nickname.
-
UNS S32053 vs UNS S31727 — which should I order?
- S31727 is a leaner Cu–Mo–N grade (Cr 17.5–19.0%, Ni 14.5–16.5%, Mo 3.8–4.5%, Cu 2.8–4.0%) at 80/36 ksi. S32053 is a high-Ni superaustenitic with Mo 5.0–6.0%, no copper range, and 93/43 ksi. They share the 1975–2155 °F anneal but address different corrosion cases, so order the UNS on your datasheet.
-
UNS S32053 vs UNS S31254 — which should I order?
- S31254 is the classic 6Mo grade with Mo 6.0–6.5%, Cu 0.50–1.00%, thickness-split tensile rows, and a 2100 °F minimum anneal. S32053 uses Mo 5.0–6.0%, higher Cr and Ni, no copper, a single 93/43 ksi row, and 1975–2155 °F. Both serve severe chloride duty, but they are separate UNS rows and are not substitutes without engineering approval.
-
Seamless vs welded UNS S32053 — which is better?
- Neither is universally better. Seamless suits heavier walls and services where the project excludes welded pipe, while welded pipe is economical for larger diameters and thinner walls. Both are legitimate SA-312 forms and both must meet the full UNS S32053 chemistry and anneal. State SML, WLD, or HCW on the order and check the same letters on the marking.
-
Can you dual-certify SA312 / A312 UNS S32053?
- Yes, when heat analysis (including Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%), the solution anneal, mechanical tests on the 93/43 ksi row, and marking meet both editions named on the order. Write the ASME and ASTM edition years on the purchase order and require the MTC to reference both, so receiving inspection can clear the heat without a second paperwork chase.
-
Hydrostatic test or NDE — which will I get?
- Each length is either hydrostatically tested or nondestructively electrically tested, and the manufacturer may choose unless the purchase order fixes the method. If your piping class or client specification requires one method, state it on the order and check that the chosen test is recorded on the MTC for every length supplied.
-
What heat treatment applies to UNS S32053?
- Table 2 lists S32053 together with S31727 at 1975–2155 °F [1080–1180 °C] with rapid cooling, which is above the 1900 °F default (the Table 2 pairing was read from a two-column layout and is noted in the uncertainty file). It is not an H grade, so there is no grain-size requirement or H-grade reheat clause. Ask the mill to show the actual anneal temperature on the certificate rather than just the words solution annealed.
-
What Table 1 chemistry defines UNS S32053?
- Table 1 sets C ≤0.03%, Mn ≤1.00%, P ≤0.030%, S ≤0.010%, Si ≤1.00%, Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, with no copper requirement. These are melting-analysis limits from the ordered edition; product analysis, when required, uses the A480 tolerances. Check that every element is reported, because the distinguishing elements are exactly the ones a commodity 300-series heat would miss.
-
What are the Table 4 tensile requirements for UNS S32053?
- Table 4 sets tensile strength of 93 ksi [640 MPa] minimum and yield strength of 43 ksi [295 MPa] minimum, with 35% longitudinal and 25% transverse elongation. A single row applies regardless of wall thickness. Use the allowable stresses listed for UNS S32053 in the governing code, not those of a sister grade with a different tensile row.
-
What filler metal should I use to weld UNS S32053 pipe?
- Table 6 does not clearly assign an AWS filler class to S32053 in the extract used for this page, so the consumable is by agreement. Industry practice for 5–6% Mo superaustenitics is an overalloyed Ni-Cr-Mo filler, but the class must be qualified on S32053 and frozen on the WPS. Qualify the procedure on the actual grade, use low heat input and full back-purging, and remove heat tint after welding so the joint keeps its corrosion resistance.
-
What heat-treatment temperature applies to UNS S32053?
- Table 2 lists S32053 with S31727 at 1975–2155 °F [1080–1180 °C] followed by rapid cooling. That is above the 1900 °F default and is needed to keep the high-Mo structure free of intermetallic phases. Ask the mill to record the actual anneal temperature on the MTC so it can be checked against the window.
Conclusion
ASME SA312 UNS S32053 is a TP-less high-nickel, high-chromium superaustenitic with 5–6% molybdenum and nitrogen, defined by Cr 22.0–24.0%, Ni 24.0–26.0%, Mo 5.0–6.0%, and N 0.17–0.22%, a 93/43 ksi tensile row, and a solution anneal at 1975–2155 °F [1080–1180 °C]. Order it by UNS number, check every Table 1 element and the anneal temperature on the certificate, and compare it carefully with ASME SA312 UNS S31254 Stainless Steel Pipe and ASME SA312 UNS S31266 Stainless Steel Pipe before accepting any substitution. For stock, mill certificates, or a quotation on SA312 UNS S32053 pipe, contact admin@steelspecs.com or browse the ASME SA 312/SA 312M category.
Quality Steel Needed? Inquire for Offers
Related Products