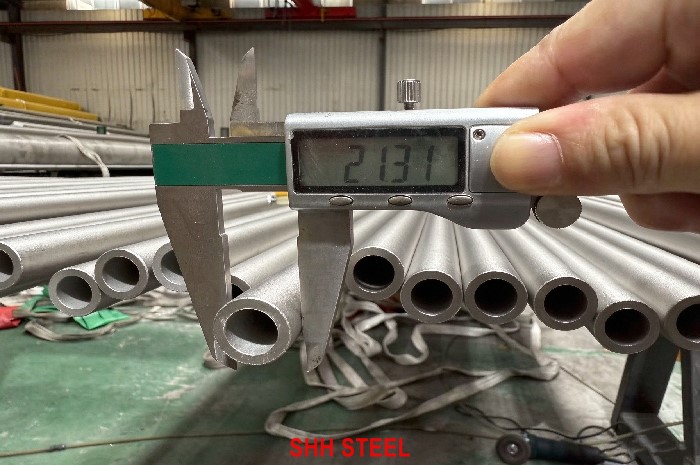
ASTM A312 TP XM-19 Stainless Steel Pipe
What is ASTM A312 TP XM-19 Stainless Steel Pipe
A312/A312M is the ASTM product specification for seamless, welded, and heavily cold-worked austenitic stainless steel pipe intended for high-temperature and general corrosive service. It stands on its own as an ASTM standard, and this page is written against it. TPXM-19 (UNS S20910) is one of the less common rows in its Table 1, and that is exactly why buyers ask us to spell out what the specification actually fixes for this alloy and what is left to agreement between purchaser and mill.
TPXM-19 is the most heavily alloyed of the XM grades in A312. It combines 20.5–23.5% chromium, 11.5–13.5% nickel, and 1.50–3.00% molybdenum with 4.0–6.0% manganese and 0.20–0.40% nitrogen, plus small additions of niobium and vanadium, and that package gives it the highest Table 4 floor in this group at 100 ksi tensile and 55 ksi yield. It is ordered when a line needs both high strength and corrosion resistance at least in the 316 class, which is a combination few standard grades offer.
SHH STEEL can supply ASTM A312 TPXM-19 pipe as seamless (SML), welded (WLD), or heavily cold-worked (HCW) product, in ASME B36.19 stainless schedules or special OD and wall by agreement, with EN 10204 3.1 mill test certificates that report the full Table 1 heat analysis, the Table 4 tension results, and the heat-treatment record. Where a purchase order also asks for ASME SA-312 marking, dual marking can be offered on heats that qualify under both documents, but the ASTM grade remains the one this page describes.
Enquiries describe it as XM-19, TP XM-19, 22-13-5, or by producer trade names, and the order should carry ASTM A312 TPXM-19 / UNS S20910 so the certificate can be checked against Table 1. Trade names are shorthand only, and some producer brochures quote properties well above the specification, so the contract value is always the Table 4 floor.
If TPXM-19 turns out not to be the right fit, the closest sister pages in the same ASTM series are A312 TPXM-29, A312 TPXM-10, A312 TPXM-11, A312 TP316L, and A312 UNS S31254. All A312 grades are collected on the A312/A312M hub, so a short list can be compared against one standard before the enquiry goes out.
Manufacturing Types (SML / WLD / HCW)
ASTM A312 allows three manufacturing routes for TPXM-19 pipe, and the route is a purchase-order decision rather than a property of the grade. Whichever route is chosen, the heat must still meet the same Table 1 limits (C ≤0.06%, Mn 4.0–6.0%, Cr 20.5–23.5%, Ni 11.5–13.5%, Mo 1.50–3.00%, Nb 0.10–0.30%, N 0.20–0.40%, and V 0.10–0.30%), the same Table 4 tension floor, and the same 1900 °F [1040 °C] minimum solution anneal (Table 2 default) with rapid cooling heat-treatment requirement before any length is released.
- Seamless (SML) pierced and hot or cold finished, chosen for heavy wall, high pressure, or owner specifications that exclude a weld seam
- Welded (WLD) formed from flat-rolled product and welded without filler or with filler where the edition allows, economical in thinner walls and larger diameters
- Heavily cold-worked (HCW) welded pipe given at least 35% cold reduction of the weld and base metal before the final anneal, which refines the weld structure toward seamless behaviour
TPXM-19 is a high-value specialty alloy, so seamless pipe in small and medium sizes is the common route, and welded or HCW product is usually quoted against a defined project quantity. Tell us which route your design code or client specification accepts, because a quotation that leaves the route open forces the mill to choose and can create disputes at receiving inspection.
Chemical Composition of ASTM A312 TPXM-19
The melting analysis in Table 1 is what the heat must meet when it is cast, and it is the first table a reviewer should compare against the mill certificate. For TPXM-19 (UNS S20910) the defining limits are C ≤0.06%, Mn 4.0–6.0%, Cr 20.5–23.5%, Ni 11.5–13.5%, Mo 1.50–3.00%, Nb 0.10–0.30%, N 0.20–0.40%, and V 0.10–0.30%. The table below reproduces the Table 1 row as published, with elements carrying no requirement shown as such rather than filled with invented values.
| Element | TPXM-19 (UNS S20910) melting analysis |
|---|---|
| Carbon (C) | ≤ 0.06 |
| Manganese (Mn) | 4.0 – 6.0 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 20.5 – 23.5 |
| Nickel (Ni) | 11.5 – 13.5 |
| Molybdenum (Mo) | 1.50 – 3.00 |
| Niobium (Nb) | 0.10 – 0.30 |
| Nitrogen (N) | 0.20 – 0.40 |
| Vanadium (V) | 0.10 – 0.30 |
Five lines deserve attention on the certificate: chromium, nickel, and molybdenum for corrosion resistance, and nitrogen plus manganese for strength. Niobium and vanadium are present in narrow 0.10–0.30% bands that help hold strength and refine grain, and both must be reported because they are Table 1 requirements, not optional extras.
Product analysis is a separate check made on the finished pipe, and ASTM A312 refers it to the permitted variations in ASTM A480 Table A1.1. The second table adds those tolerances to the melt limits so you can see the band that a check analysis on the pipe is allowed to fall within when Supplementary Requirement S1 or an owner check is ordered.
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | ≤ 0.06 | 0.01 over | ≤ 0.07 |
| Manganese (Mn) | 4.0 – 6.0 | 0.05 under / over | 3.95 – 6.05 |
| Phosphorus (P) | ≤ 0.045 | 0.010 over | ≤ 0.055 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 20.5 – 23.5 | 0.25 under / over | 20.25 – 23.75 |
| Nickel (Ni) | 11.5 – 13.5 | 0.15 under / over | 11.35 – 13.65 |
| Molybdenum (Mo) | 1.50 – 3.00 | 0.05 under / 0.10 over | 1.45 – 3.10 |
| Niobium (Nb) | 0.10 – 0.30 | 0.05 under / over | 0.05 – 0.35 |
| Nitrogen (N) | 0.20 – 0.40 | 0.02 under / 0.04 over | 0.18 – 0.44 |
| Vanadium (V) | 0.10 – 0.30 | 0.03 under / over | 0.07 – 0.33 |
Read the product limits as acceptance bounds for a check analysis only. A heat that sits outside the Table 1 melt range is non-conforming even if a later product analysis lands inside the widened band, so the certificate should always show the ladle analysis first.
Mechanical Properties of ASTM A312 TPXM-19
Table 4 sets the room-temperature tension requirements for TPXM-19: 100 ksi [690 MPa] tensile strength and 55 ksi [380 MPa] yield strength minimum, with elongation of 35% longitudinal / 25% transverse minimum. The table below shows those values in the form used on the specification, and the mill certificate should report actual results against each line.
| Property | TPXM-19 requirement (Table 4) |
|---|---|
| Tensile strength, min | 100 ksi [690 MPa] |
| Yield strength (0.2% offset), min | 55 ksi [380 MPa] |
| Elongation in 2 in. or 50 mm (or 4D) | 35% longitudinal / 25% transverse, min |
At 55 ksi minimum yield, TPXM-19 offers nearly twice the yield floor of TP316 at 30 ksi. Where the governing code lists allowable stresses for S20910, that difference can justify a much thinner wall or a higher pressure rating, but the weld has to be able to match it, which is why the filler choice below matters.
No hardness maximum is set for this grade in Table 4, so a hardness figure on a certificate is information rather than an acceptance criterion unless your order adds one. If a project specification imposes hardness or impact testing, write it on the purchase order so the mill can plan the test pieces before the pipe is cut.
Dimensions, Tolerances and Stock Sizes
Dimensions for ASTM A312 TPXM-19 pipe are normally ordered by NPS and schedule from ASME B36.19, or by outside diameter and wall where the design calls for a non-standard size. Outside-diameter tolerance and wall tolerance come from the specification itself, and wall is read as nominal unless Supplementary Requirement S8 asks for minimum wall. The permitted variations in wall thickness from Table 3 are shown below by NPS band and wall-to-diameter ratio.
| NPS designator | Wall over | Wall under |
|---|---|---|
| 1/8 to 2-1/2 incl., all t/D | 20.0% | 12.5% |
| 3 to 18 incl., t/D up to 5% | 22.5% | 12.5% |
| 3 to 18 incl., t/D over 5% | 15.0% | 12.5% |
| 20 and larger, welded, all t/D | 17.5% | 12.5% |
| 20 and larger, seamless, t/D up to 5% | 22.5% | 12.5% |
| 20 and larger, seamless, t/D over 5% | 15.0% | 12.5% |
In practice the under-tolerance of 12.5% is the figure that matters for pressure design, because the designer has already sized the nominal wall with that allowance in mind. The over-tolerance varies with NPS and the wall-to-diameter ratio, which matters more for fit-up and weld preparation than for strength. For TPXM-19, whose higher strength or special chemistry often justifies a lighter or more closely engineered wall, confirm whether your calculation assumed nominal or minimum wall before the order is placed.
Stock / Available sizes. The table below shows the representative size band we quote for ASTM A312 TPXM-19, with example OD × wall combinations taken from B36.19 schedules. It is a supply and stock-enquiry range rather than a promise that every size sits on the floor today: for TPXM-19 some small and medium seamless sizes in Sch 10S, 40S, and 80S may be available from existing material, while larger diameters and welded pipe are normally mill orders. Special OD, special wall, and cut lengths are always handled on enquiry.
| Representative size | Example OD × wall | Typical schedules / notes |
|---|---|---|
| NPS 1/2 – 2 | 21.34 × 2.77 mm (NPS 1/2 Sch 40S); 60.33 × 3.91 mm (NPS 2 Sch 40S) | Sch 10S / 40S / 80S; small-bore process and instrument take-offs |
| NPS 2-1/2 – 6 | 88.90 × 5.49 mm (NPS 3 Sch 40S); 168.28 × 3.40 mm (NPS 6 Sch 10S) | Sch 10S / 40S / 80S; the most frequent enquiry band |
| NPS 8 – 12 | 219.08 × 8.18 mm (NPS 8 Sch 40S); 323.85 × 4.57 mm (NPS 12 Sch 10S) | Sch 10S / 40S; confirm SML or WLD route on enquiry |
| NPS 14 – 24 | 406.40 × 4.78 mm (NPS 16 Sch 10S); 609.60 × 9.53 mm (NPS 24 Sch 40S) | Sch 10S / 40S; usually mill-order, mostly welded |
| Special OD × wall | Any OD and wall the mill can qualify | On enquiry: state OD, nominal or minimum wall, and length practice |
Read the example sizes as orientation for writing the enquiry, not as a price list. When you send a size list we check live availability line by line, separate what can ship from existing material from what needs a mill slot, and give the lead time for each group so the purchase order can be split if the schedule demands it.
Equivalent Grades
Buyers often arrive with a trade name, a plate designation, or a European number rather than the A312 row. The table below maps the names we see on enquiries for TPXM-19, but only the ASTM A312 grade and UNS number are contractual on this page; everything else is a cross-reference that needs checking against its own standard.
| Designation | Notes |
|---|---|
| ASTM A312 TPXM-19 / UNS S20910 | Governing grade on this page |
| ASME SA-312 TPXM-19 | Separate Code standard; dual mark only when the order names both |
| XM-19 / 22-13-5 | Market names; confirm the full Table 1 row including Nb and V |
| AWS A5.9 ER209 | Filler listed for TPXM-19 in Table 6 |
| EN / JIS | No one-to-one equivalent asserted |
The ASME SA-312 row is listed because some Code projects require it, not because it is a synonym. ASME SA-312 is a separate standard adopted into the Boiler and Pressure Vessel Code, and the SA312 TPXM-19 page covers that document on its own terms. When both marks are wanted, the order should name both specifications and their editions so the certificate can state compliance with each.
Heat Treatment and Delivery Condition
All A312 pipe is furnished heat treated, and TPXM-19 has no individual temperature row in Table 2, so the default applies: solution anneal at 1900 °F [1040 °C] minimum followed by water quenching or another rapid cool sufficient to prevent harmful carbide reprecipitation. Seamless pipe may be quenched after hot forming when the finishing temperature is not below that minimum. In practice producers often anneal higher than the minimum to dissolve nitrides fully, and the actual temperature should be on the certificate.
Delivery condition for TPXM-19 is solution annealed, then descaled by pickling or by blasting and pickling, straightened, and cut to the ordered length practice. HCW pipe receives its cold reduction before the final anneal, so cold work is never the delivered condition. Ask for the actual annealing temperature and cooling method to be recorded on the certificate, because a reviewer cannot otherwise confirm the Table 2 requirement from the document alone.
Corrosion Resistance
ASTM A312 contains no corrosion table, so the following is engineering commentary rather than a specification requirement. With 20.5–23.5% chromium, 1.50–3.00% molybdenum, and up to 0.40% nitrogen, TPXM-19 sits at or above TP316L for pitting and crevice resistance in most chloride-bearing waters. That is the main reason it is chosen over the leaner XM grades, which have no molybdenum at all.
Carbon is limited to 0.06% and niobium is present, which together reduce the risk of intergranular attack after welding, although S7 testing should still be ordered if the owner needs documentary proof. Like other austenitic alloys, TPXM-19 is not immune to chloride stress corrosion cracking at elevated temperature, and service in hot seawater or strong acids deserves a specific review.
Applications of ASTM A312 TPXM-19 Pipe
Applications for ASTM A312 TPXM-19 pipe make use of its combination of high strength and molybdenum-bearing corrosion resistance. The table below summarizes typical uses, each subject to confirmation of code allowables for S20910.
| Application area | Typical use of TPXM-19 pipe | Selection note |
|---|---|---|
| Chemical and process | Higher-strength austenitic lines with Mo chemistry ordered to A312 | Confirm fluid compatibility with S20910 |
| Marine / chloride-bearing | Topsides and process piping where XM-19 is specified | Not automatic substitute for duplex in severe seawater |
| Oil and gas / OEM | Piping kits needing high yield austenitic stainless documentation | Dual SA312/A312 marking often requested |
| Power and utility | High-stress stainless auxiliary lines where S20910 is accepted | Use Table 4 floors in design, not catalog “typical” values |
| General corrosive + strength | Where 316-class Mo is not enough on strength but XM-19 is accepted | Do not substitute TP316 for TPXM-19 when 100/55 ksi is required |
| Fabricated spool pieces | Welded assemblies ordered as A312 TPXM-19 | Use ER209 filler guidance; document WPS |
Treat the table as a starting point for discussion with the process licensor or corrosion engineer, not as an approval. Code allowable stresses, temperature limits, and any owner material lists decide whether TPXM-19 is acceptable on a given line, and those checks should be made before the pipe is ordered rather than after it arrives.
Weldability
TPXM-19 welds by GTAW, GMAW, SMAW, and orbital GTAW with normal austenitic practice: clean preparation, moderate heat input, controlled interpass temperature, and a back-purged root. Table 6 lists ER209 (filler UNS S20980 / W32240) for TPXM-19, which is the matching high-manganese nitrogen consumable and the sensible starting point for both seam repair and fabrication welding. A 308- or 316-type filler would undermatch the 100/55 ksi base metal by a wide margin.
Qualify the procedure on TPXM-19 itself rather than on a convenient 304 coupon, because the qualification has to demonstrate the strength and soundness of this chemistry. Clean joint preparation, controlled heat input and interpass temperature, and a back-purged root are the normal baseline; the certificate for any WLD pipe should also state whether filler metal was used in the longitudinal seam.
Surface Finishes
Surface condition for ASTM A312 TPXM-19 pipe should be stated on the purchase order rather than left to mill default. On stainless pipe, residual scale, embedded free iron, and chloride contamination from handling can matter as much as the nominal finish name, and they are far easier to prevent at the mill than to correct on site.
- Annealed and pickled the standard delivery after solution treatment for process piping
- Blasted and pickled when heavier scale needs mechanical help before chemical descaling
- Bright annealed by agreement, generally on smaller sizes where the furnace atmosphere can be controlled
- Passivated or polished by agreement, with the method and acceptance criteria written on the order
For TPXM-19, the high chromium and molybdenum content means a well-pickled surface gives excellent corrosion resistance, so removal of weld tint and embedded iron deserves the same care as on 316L. If the line will be inspected for surface iron, specify the test method at the enquiry stage so that the packing and handling plan supports it.
Inspection and Testing
The base acceptance package for ASTM A312 TPXM-19 pipe combines heat analysis, tension testing, the flattening or bend test that applies to the manufacturing type, and a hydrostatic or non-destructive electric test on every length. Visual and dimensional inspection confirm the size and surface before marking. For TPXM-19 we recommend reading molybdenum, nitrogen, niobium, and vanadium together with the 55 ksi yield result, since all of them are Table 1 or Table 4 requirements that a generic certificate template can easily omit.
Supplementary requirements are optional until they are written on the order. The options buyers request most often for this grade are summarized below, and each one adds test time that should be allowed for in the delivery schedule.
| Option | Purpose |
|---|---|
| S1 product analysis | Confirms chemistry on finished pipe |
| S5 radiography | Weld integrity on WLD pipe |
| S7 intergranular corrosion | A262 Practice E after sensitizing treatment |
| S8 minimum wall | Wall interpreted as minimum rather than nominal |
| S9 weld decay | Compares weld and base-metal loss rates |
Third-party inspection, witness points, and EN 10204 3.2 certification are available when the order names the inspection agency. Agree the hold points before production starts, because witnessing a hydrotest or a tension test after the fact is not possible.
Packaging and Shipping
ASTM A312 TPXM-19 pipe is packed for handling and for ocean or land transport. Each length is marked with ASTM A312, the grade TPXM-19 / UNS S20910, the manufacturing type, size, heat number, and the test method used, with SA-312 added only when the order asks for dual marking. Bundle lists repeat the heat numbers so receiving can match pipe to certificates without opening every wrap.
- End caps or bevel protectors fitted as ordered
- Bundles strapped with protected contact points to limit iron pick-up
- Wooden cases or seaworthy bundles for export, with moisture protection for sea freight
- Small-bore or polished pipe cased separately where damage risk is higher
Stainless pipe should not be stored or lifted in contact with carbon steel, and for a specialty grade such as TPXM-19 it is worth keeping the material segregated by heat on arrival, since mixing it with common 304 stock is the most frequent cause of misuse on site.
Why Choose SHH STEEL
SHH STEEL supplies specification-driven stainless pipe, and for a specialty grade such as ASTM A312 TPXM-19 we quote against the edition you name rather than a generic catalogue sheet. We report the full Table 1 heat analysis, the Table 4 tension results, and the heat-treatment record, and we tell you early when a size or route is a mill order instead of letting the lead time surprise you.
- Familiarity with high-strength molybdenum-bearing XM grades and the ER209 matching-filler question they raise
- Clear advice on sister grades under ASTM A312, so TPXM-19 is not confused with a commoner alloy that looks similar on paper
- Honest separation of specification requirements from producer or market guidance in every document we send
- EN 10204 3.1 certificates as standard, with third-party inspection and 3.2 certification on request
The aim is a delivery that clears receiving inspection on the first review. That means the certificate, the stencil, and the purchase order all say the same thing about grade, UNS number, manufacturing type, size, and heat treatment, and that any agreed variation is written down before the pipe is made.
Supply Capability
SHH STEEL can supply ASTM A312 TPXM-19 stainless steel pipe against the edition and manufacturing type named on your enquiry. The capability table below summarizes the routes, sizes, finishes, and documents we regularly quote for this grade, and each line can be narrowed to your project specification.
| Item | SHH STEEL capability for TPXM-19 |
|---|---|
| Standard | ASTM A312 / A312M, TPXM-19 / UNS S20910 |
| Manufacturing types | SML, WLD, HCW |
| Size | NPS 1/8 and up per ASME B36.19; special OD and wall by agreement |
| Schedules | 5S, 10S, 40S, 80S and non-standard walls |
| Length | Single random, double random, or cut to length |
| Heat treatment | 1900 °F [1040 °C] minimum solution anneal (Table 2 default) with rapid cooling |
| Filler guidance | ER209 (S20980 / W32240) per Table 6 |
| Testing | Tension (100/55 ksi), flattening or bend, hydrostatic or electric test per length; S1, S5, S7, S8, S9 on order |
| Documents | EN 10204 3.1 with full Table 1 analysis; 3.2 and third-party inspection on request |
| Trade terms | FOB, CFR, CIF, EXW and other agreed Incoterms |
Stock / Available sizes. The representative band for TPXM-19 is NPS 1/2 to 24 in Sch 10S, 40S, and 80S as listed under Dimensions. Selected common OD × wall combinations may be available from existing material, while heavy-wall seamless, unusual schedules, and special cut lengths are normally mill orders. We do not publish stock part numbers or tonnage claims for this grade; ask for a live check against your size list instead.
Enquiries move fastest when they state the A312 edition, TPXM-19 / UNS S20910, the manufacturing type, NPS or OD × wall (and whether the wall is nominal or minimum), length practice, finish, and any product-analysis, corrosion-test, or 3.2 requirements. Dual SA-312 marking, bevelled ends, and cut lengths are available on confirmed orders when the order says so.
FAQ
-
Is ASTM A312 TPXM-19 the same as ASME SA-312 TPXM-19?
- They are two independent standards. ASTM A312/A312M is the ASTM product specification, and ASME SA-312 is the separate document adopted into the Boiler and Pressure Vessel Code. The technical rows for UNS S20910 are closely aligned in current editions, but a pipe is only certified to the document named on the order, so when both are needed the purchase order should list both specifications and editions and the certificate should state compliance with each.
-
What is the UNS number for ASTM A312 TPXM-19?
- ASTM A312 TPXM-19 is UNS S20910, often described in the market as 22-13-5 after its nominal chromium, nickel, and manganese levels. The UNS number should appear on the mill certificate and on the stencil next to the ASTM A312 mark, because a trade name alone makes it hard for receiving inspection to tie the chemistry on the certificate to the pipe in the rack.
-
What are the tensile and yield requirements for ASTM A312 TPXM-19 pipe?
- Table 4 requires 100 ksi [690 MPa] tensile strength and 55 ksi [380 MPa] yield strength minimum, with elongation of 35% longitudinal / 25% transverse minimum. These are room-temperature minimums for acceptance only; design allowables at temperature come from the applicable piping code, and they should be checked there before a wall thickness is fixed.
-
What heat treatment does ASTM A312 TPXM-19 pipe receive?
- TPXM-19 has no individual Table 2 row, so it is solution annealed at the 1900 °F [1040 °C] minimum default and then water quenched or rapidly cooled. The delivered condition is solution annealed and descaled, and the certificate should record the actual annealing temperature and the cooling method so a reviewer can confirm the requirement without asking the mill.
-
Which filler metal is used to weld ASTM A312 TPXM-19?
- Table 6 lists AWS A5.9 ER209 (filler UNS S20980 / W32240) for TPXM-19, the matching high-manganese nitrogen consumable that keeps the weld in step with the 100/55 ksi base metal. Whatever is chosen should be recorded on the WPS and PQR, and the procedure should be qualified on TPXM-19 base metal so that the joint strength and soundness are demonstrated on the real chemistry.
-
Is ASTM A312 TPXM-19 pipe available seamless and welded?
- Yes. ASTM A312 allows seamless (SML), welded (WLD), and heavily cold-worked (HCW) pipe for TPXM-19, all meeting the same chemistry, tension, and heat-treatment rules. Seamless is usual for heavy wall and high pressure, while welded is often more economical in thin walls and larger diameters; state the accepted route on the order.
-
What sizes of ASTM A312 TPXM-19 pipe can SHH STEEL supply?
- We quote NPS 1/2 to 24 in Sch 10S, 40S, and 80S as the representative band, plus NPS 1/8 and up and special OD and wall by agreement. Some common sizes may be available from existing material, while heavy-wall seamless and unusual schedules are normally mill orders, so send a size list for a live check.
-
What documents come with ASTM A312 TPXM-19 pipe?
- Each shipment carries an EN 10204 3.1 mill test certificate showing the A312 edition, TPXM-19 / UNS S20910, manufacturing type, heat number, the full Table 1 heat analysis, Table 4 tension results, heat treatment, and the hydrostatic or electric test. Third-party inspection and 3.2 certification can be added when the order names the agency.
-
Is TPXM-19 stronger than TP316 stainless pipe?
- Yes, by a large margin. Table 4 requires 100 ksi tensile and 55 ksi yield for TPXM-19, against 75 ksi and 30 ksi for TP316, and the corrosion resistance is at least comparable because TPXM-19 carries 1.50–3.00% molybdenum with higher chromium and nitrogen. The trade-off is cost and availability.
-
How does TPXM-19 differ from TPXM-29?
- Both reach 100/55 ksi in Table 4, but TPXM-29 is a lean-nickel 18Cr-3Ni-13Mn alloy with no molybdenum, while TPXM-19 has 11.5–13.5% nickel and 1.50–3.00% molybdenum. TPXM-19 is chosen for corrosion plus strength; TPXM-29 for strength and galling resistance at lower alloy cost.
-
Can TPXM-19 be used in seawater piping?
- It is often considered for seawater and brackish water because of its molybdenum and nitrogen, and it performs better than 304-type alloys there. Whether it is adequate depends on temperature, velocity, and crevice conditions, so compare it with super-austenitic grades such as UNS S31254 and get a corrosion review before committing.
Conclusion
ASTM A312 TPXM-19 (UNS S20910) is the high-strength, molybdenum-bearing 22-13-5 grade of the series, ordered when a line needs a 100/55 ksi floor together with corrosion resistance in the 316 class or better. The specification fixes C ≤0.06%, Mn 4.0–6.0%, Cr 20.5–23.5%, Ni 11.5–13.5%, Mo 1.50–3.00%, Nb 0.10–0.30%, N 0.20–0.40%, and V 0.10–0.30%, a Table 4 floor of 100 ksi [690 MPa] tensile and 55 ksi [380 MPa] yield, and 1900 °F [1040 °C] minimum solution anneal (Table 2 default) with rapid cooling heat treatment, while filler selection is ER209 per Table 6. Put the manufacturing type, size and wall basis, finish, and any supplementary tests on the purchase order, and review the EN 10204 3.1 certificate against Tables 1, 2, and 4 before release. SHH STEEL can supply ASTM A312 TPXM-19 pipe to the edition you name; compare sister grades on the A312/A312M hub, or send your size list to admin@steelspecs.com.
Quality Steel Needed? Inquire for Offers
Related Products