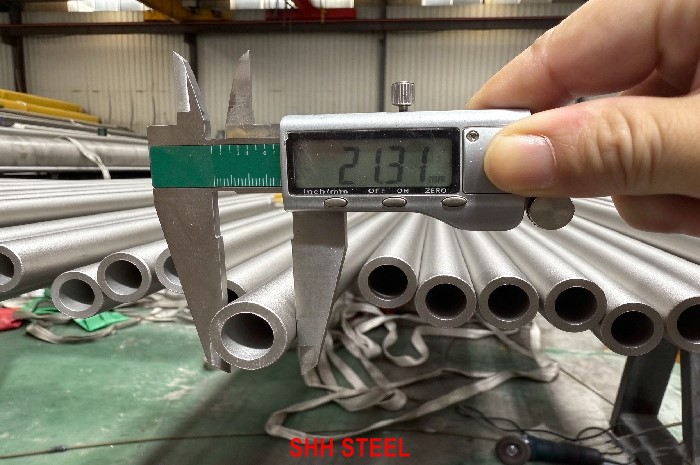
ASTM A312 TP310HCb Stainless Steel Pipe
What is ASTM A312 TP310HCb Stainless Steel Pipe
ASTM A312/A312M is the ASTM product specification for seamless, straight-seam welded, and heavily cold-worked austenitic stainless steel pipe intended for high-temperature and general corrosive service. It stands on its own as an ASTM document, with its own chemistry table, tensile table, heat-treatment table, and testing clauses, and a purchase order written to it should name the ASTM edition directly. This page covers Grade TP310HCb / UNS S31041 under that specification and draws every number from the referenced A312/A312M tables rather than from catalogue habit.
TP310HCb is the niobium-stabilized H grade that combines a controlled carbon band with grain-size control of the 25Cr–20Ni ASTM A312 family. Table 1 sets C 0.04–0.10%, Cr 24.0–26.0%, Ni 19.0–22.0%, Mo ≤0.75%, Nb 10×C min / 1.10 max, with manganese capped at 2.00%, silicon at 1.00%, phosphorus at 0.045% and sulfur at 0.030%. The 310 family is the highest chromium–nickel group among the common A312 heat-resisting grades, and buyers usually reach for it when the 309 family is close to its oxidation limit or when the service cycles hard between ambient and furnace temperature. Table 4 releases the grade at 75 ksi [515 MPa] tensile and 30 ksi [205 MPa] yield with 35% longitudinal / 25% transverse elongation, and the pipe is delivered solution annealed at 1900 °F [1040 °C] minimum with rapid cooling.
The “HCb” suffix stacks two ideas: an H-grade carbon band of 0.04–0.10% with ASTM grain size No. 6 or coarser, plus niobium stabilization at 10×C minimum. The result is a pipe intended for creep-range service that is also welded heavily in fabrication. Read the suffix as part of the grade identity, because a length stenciled only “310” does not tell receiving inspection which Table 1 row the heat was melted to.
SHH STEEL can supply ASTM A312 TP310HCb stainless steel pipe as seamless (SML), welded (WLD), or heavily cold-worked (HCW) product in ASME B36.19 schedules and in special OD and wall combinations, with EN 10204 3.1 mill test certificates as the standard document package and EN 10204 3.2 or third-party witness when the enquiry asks for it. Where a project also runs under the ASME Boiler and Pressure Vessel Code, dual A312/SA-312 marking can be arranged, but only when the purchase order names both standards and the heat qualifies under each. ASME SA-312 is a separate standard with its own adoption history, and the same grade is described on its own page at SA312 TP310HCb.
Buyers comparing TP310HCb within the ASTM A312 series usually look next at A312 TP310S, A312 TP310H, A312 TP310Cb, and at the matching 309-family grade A312 TP309HCb. The full grade list is on the A312/A312M hub, which is the quickest way to check a neighbouring grade when the datasheet leaves more than one heat-resisting option open.
Manufacturing Types (SML / WLD / HCW)
ASTM A312 allows three manufacturing routes for TP310HCb pipe, and the choice belongs on the purchase order because it changes inspection, marking, and sometimes the design allowance, while it never changes the chemistry. Whichever route is chosen, the heat must still meet C 0.04–0.10%, Cr 24.0–26.0%, Ni 19.0–22.0%, Mo ≤0.75%, Nb 10×C min / 1.10 max, and every length still has to pass through the solution anneal before release.
- Seamless (SML) — produced without welding at any stage, and preferred for high-pressure service, heavy wall, and owners who exclude welded pipe from the line class. For creep-range lines, seamless is often specified on heavy walls, while welded product suits large-diameter ducting where the seam is radiographed and the grain-size check is made on the finished pipe.
- Welded (WLD) — made by an automatic welding process with no filler metal in the longitudinal seam, then solution annealed. Ask for the strip or plate heat number on the certificate, because that heat is what carries the Table 1 chemistry.
- Heavily cold-worked (HCW) — welded pipe cold worked by at least 35% reduction in both wall and weld before the final anneal, with the weld radiographed before cold work. Order HCW only when the project specifically calls for that marking and its process controls.
Chemical Composition of ASTM A312 TP310HCb
Two layers of chemistry matter on an ASTM A312 TP310HCb order. The heat (ladle) analysis is mandatory for every heat and must meet Table 1, while product analysis on the finished pipe is made only when the purchase order calls for it, using the tolerances that A312 brings in through ASTM A999/A999M and ASTM A480/A480M Table A1.1. SHH STEEL reports actual heat values on the certificate and, when ordered, product values as well; we do not quote tighter in-house windows as if they were part of the standard.
Heat analysis — ASTM A312 Table 1
The table below sets out the Table 1 heat-analysis limits for TP310HCb / UNS S31041. Values are maxima unless a range is shown, and an ellipsis means the edition places no requirement on that element.
| Element | TP310HCb / UNS S31041 heat analysis, % |
|---|---|
| Carbon (C) | 0.04 – 0.10 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 24.0 – 26.0 |
| Nickel (Ni) | 19.0 – 22.0 |
| Molybdenum (Mo) | ≤ 0.75 |
| Niobium (Nb) / Columbium (Cb) | 10 × C min, 1.10 max |
Reading the table, the defining lines are chromium at 24.0–26.0%, nickel at 19.0–22.0%, and the niobium line of 10×C minimum and 1.10% maximum. The niobium floor is tied to the actual carbon of the heat, so a heat with C 0.06% needs at least 0.60% Nb and still no more than 1.10%; check that arithmetic on every certificate rather than just confirming that a niobium value is printed. Nb and Cb are the same element. Some editions carry a footnote quoting 1.00% Nb maximum for certain grades while the TP310HCb cell itself prints 1.10%; this page follows the table cell and leaves the footnote conflict flagged as uncertain until the ordered edition is checked.
Product analysis — A480/A480M Table A1.1 tolerances
When product analysis is ordered, the Table A1.1 tolerances are applied to the Table 1 limits as shown below. The tolerance applies to an individual product determination; it does not widen the heat-analysis range that the mill must meet in the first place.
| Element | Melting (Table 1) | Tolerance (A480 A1.1) | Product analysis limit |
|---|---|---|---|
| Carbon (C) | 0.04 – 0.10 | 0.01 under / over | 0.03 – 0.11 |
| Manganese (Mn) | ≤ 2.00 | 0.04 over | ≤ 2.04 |
| Phosphorus (P) | ≤ 0.045 | 0.010 over | ≤ 0.055 |
| Sulfur (S) | ≤ 0.030 | 0.005 over | ≤ 0.035 |
| Silicon (Si) | ≤ 1.00 | 0.05 over | ≤ 1.05 |
| Chromium (Cr) | 24.0 – 26.0 | 0.25 under / over | 23.75 – 26.25 |
| Nickel (Ni) | 19.0 – 22.0 | 0.15 under / 0.20 over | 18.85 – 22.20 |
| Molybdenum (Mo) | ≤ 0.75 | 0.05 over | ≤ 0.80 |
| Niobium (Nb / Cb) | 10×C min – 1.10 max | 0.05 over on max (Cb+Ta to 1.50 band) | max ≤ 1.15 product; heat-analysis 10×C floor not relaxed |
310 family side by side
Because four 310-family rows sit next to each other in Table 1, it helps to see them together. The comparison below uses the same Table 1 values and shows where TP310HCb differs from its sisters; chromium is 24.0–26.0% for all four.
| Element | TP310S | TP310H | TP310Cb | TP310HCb |
|---|---|---|---|---|
| C | ≤ 0.08 | 0.04 – 0.10 | ≤ 0.08 | 0.04 – 0.10 |
| Ni | 19.0 – 22.0 | 19.0 – 22.0 | 19.0 – 22.0 | 19.0 – 22.0 |
| Mo | ≤ 0.75 | … | ≤ 0.75 | ≤ 0.75 |
| Nb | … | … | 10×C – 1.10 | 10×C – 1.10 |
| Table 5 grain size | — | No. 6 or coarser | — | No. 6 or coarser |
Reading across, the S and Cb grades share the 0.08% carbon cap, the H and HCb grades share the 0.04–0.10% band and the Table 5 grain-size rule, and the niobium line appears only on the two stabilized rows. In the 310 family nickel is 19.0–22.0% on every row, so the comparison turns entirely on carbon, niobium, and grain size. The differences look small on paper but they decide which heats a mill can allocate, so name the exact TP designation and UNS number on the order instead of a family name.
Mechanical Properties of ASTM A312 TP310HCb
Room-temperature tensile requirements for TP310HCb come from ASTM A312 Table 4. They are minima for release testing, not typical values, and they are the same 75/30 ksi floor shared by the other 310-family grades. Mill results usually sit above these figures, but design should still use the table unless the purchase order states higher guaranteed values.
| Property | ASTM A312 TP310HCb / UNS S31041 |
|---|---|
| Tensile strength, min | 75 ksi [515 MPa] |
| Yield strength, min | 30 ksi [205 MPa] |
| Elongation, min | 35% longitudinal / 25% transverse |
| Hardness | No Table 4 maximum |
| Grain size (Table 5) | ASTM No. 6 or coarser (UNS S31041) |
The row that sets TP310HCb apart is grain size. Table 5 requires ASTM grain size No. 6 or coarser, and that check is what lets the H grade carry its elevated-temperature strength, because a coarser austenite grain resists creep better than a fine one. The tensile floor itself is no higher than TP310S, so a buyer comparing room-temperature certificates will not see the difference; it shows up in the grain-size report and in the carbon band.
Dimensions, Tolerances and Stock Sizes
Dimensional supply for ASTM A312 TP310HCb follows ASME B36.19 for the standard NPS and schedule combinations, with special outside diameters and walls available by agreement when a furnace, heater, or duct needs a section the schedules do not cover. Outside-diameter variations follow ASTM A999/A999M, and wall-thickness variations follow A312 Table 3, summarized below.
| NPS designator | Wall over | Wall under |
|---|---|---|
| 1/8 to 2-1/2 incl., all t/D | 20.0% | 12.5% |
| 3 to 18 incl., t/D up to 5% | 22.5% | 12.5% |
| 3 to 18 incl., t/D over 5% | 15.0% | 12.5% |
| 20 and larger, welded, all t/D | 17.5% | 12.5% |
| 20 and larger, seamless, t/D up to 5% | 22.5% | 12.5% |
| 20 and larger, seamless, t/D over 5% | 15.0% | 12.5% |
In short, the under-tolerance on wall is 12.5% across the whole range, while the permitted over-tolerance depends on the NPS, the wall-to-diameter ratio, and for NPS 20 and larger on whether the pipe is welded or seamless. State on the order whether the wall is nominal or minimum (Supplementary S8), because the two readings produce different pipe from the same line item, and the difference matters most on thin-wall heat-resisting ducts.
- Lengths — single random, double random, or cut-to-length as ordered
- Cut lengths — normally no more than 1/4 in. [6 mm] over the ordered length unless the PO sets a tighter band
- Ends — plain or beveled; confirm bevel angle and root face if the WPS is already fixed
- Jointers — not permitted unless the purchase order expressly allows them
Stock / Available sizes
SHH STEEL quotes ASTM A312 TP310HCb against a practical stock-and-mill enquiry range rather than a fixed list of stock-keeping units. The representative sizes below are the combinations most often discussed for this grade; availability for a given manufacturing route and exact wall still has to be confirmed at enquiry, and we do not publish tonnages against individual lines.
| Representative size (ASME B36.19) | Typical schedules / notes for TP310HCb |
|---|---|
| NPS 1/2 – 2 | Sch 10S / 40S / 80S; instrument and small process connections |
| NPS 2-1/2 – 6 | Sch 10S / 40S / 80S; common furnace and process line sizes |
| NPS 8 – 12 | Sch 10S / 40S; confirm SML or WLD at enquiry |
| NPS 14 – 24 | Sch 10S / 40S; usually welded and often mill-order depending on wall |
| Special OD × wall | By agreement — state OD, wall (nominal or minimum), and length practice |
Example enquiries we handle are framed as OD × wall, for instance NPS 4 Sch 40S or a special OD with a minimum wall for a heater coil, and we answer with what can ship from selected stock and what needs a mill slot. TP310HCb is a specialty grade and is normally produced to order; remnant lengths from a recent qualified heat are occasionally available and are worth asking about for small urgent quantities. Special sizes, cut lengths, and mixed seamless and welded packages are on enquiry.
Equivalent Grades
Equivalence for TP310HCb is first an identity question within ASTM A312 and only second a cross-reference to other systems. The governing designation on this page is ASTM A312 Grade TP310HCb / UNS S31041; trade names, plate counterparts, and foreign designations all need to be mapped back to that row before a mill is asked to substitute or dual-mark.
| Designation | Notes |
|---|---|
| ASTM A312 / A312M TP310HCb / UNS S31041 | Governing pipe grade for this page |
| ASME SA-312 TP310HCb | Separate ASME standard; dual marking only when the PO names both and the heat qualifies |
| 310HCb / 310HNb (trade names) | Confirm UNS S31041 chemistry on the MTC; not a grade name by itself |
| ASTM A240 UNS S31041 | Plate and sheet counterpart — not a pipe specification |
| EN / JIS | No one-to-one equivalent asserted here |
Read the notes column literally: an EN or JIS designation is a starting point for engineering comparison, not a substitute grade, and for an H or stabilized grade the carbon band, niobium line, and grain-size rule rarely map across cleanly. Within ASTM A312 the closest relatives are A312 TP310S, A312 TP310H, A312 TP310Cb, but each one is a separate row with its own limits, so an order for one is not satisfied by a certificate for another.
Compared with A312 TP309HCb, the 310 family adds about two points of chromium and seven of nickel, which buys oxidation and scaling margin at the top of the heat-resisting range; it is overkill on lines that TP309HCb handles comfortably. Versus A312 TP347H, which stabilizes an 18-8 base with niobium, TP310HCb stabilizes a much richer base for hotter service; the two are not interchangeable and dual marking between them does not apply. Where a project spans pipe and plate, carry the same UNS number through both forms but still order the pipe to A312.
Heat Treatment and Delivery Condition
All pipe furnished to ASTM A312 is heat treated. Table 2 lists TP310HCb in the same group as TP309H, TP309HCb, TP310H at a solution-annealing temperature of 1900 °F [1040 °C] minimum, followed by water quenching or another rapid cool. The temperature looks the same as the default used for many non-H grades, but the route to it is different: clause 6.2 requires H-grade pipe to be reheated to the solution temperature for the required time before quenching, so a direct quench straight off the hot-forming operation is not accepted for TP310HCb.
- Reheated solution anneal — 1900 °F [1040 °C] minimum, then rapid cool (Table 2)
- Grain size — ASTM grain size No. 6 or coarser, reported on the certificate
- Lot identification — heat number and heat-treatment lot marked on each length (clause 17)
- Surface — free of scale and contaminating iron; pickled or equivalent as ordered
For an H grade the furnace record is part of the product, so ask for the heat-treatment lot on the certificate and keep it matched to the stencil on each length. That is how receiving inspection connects a given pipe to its grain-size result. If the purchase order also requires a post-fabrication treatment, write the temperature and hold time explicitly and make sure it does not undo the grain structure the H grade was bought for.
Corrosion Resistance
The case for TP310HCb is primarily oxidation and scaling resistance at high temperature. The 24.0–26.0% chromium forms a protective oxide that holds up in hot air and many combustion atmospheres where 18-8 grades scale away, and the 19.0–22.0% nickel keeps the matrix fully austenitic and tough through thermal cycling. The 310 family takes this to the top of the common A312 range, which is why it is chosen for the hottest sections of furnaces and heaters.
TP310HCb pairs creep-range carbon with niobium stabilization, so it is meant for lines that both run hot and spend part of their life cold and wet during shutdown. The niobium protects weld heat-affected zones from chromium-carbide sensitization; the grade still does not exceed the oxidation limit of its family, and it is not a cure for carburizing or sulfidizing atmospheres.
Applications of ASTM A312 TP310HCb Pipe
Buyers typically select TP310HCb when creep-range design and welded-zone stabilization are both on the datasheet. The table below lists the services where we most often see the grade on an enquiry, together with the reason it is chosen and the point worth checking before ordering.
| Application | Why TP310HCb | Check before ordering |
|---|---|---|
| Fired-heater tubes with welded headers | Creep range plus weld stability | Grain-size result on the MTC |
| Refinery furnace outlet lines | Shutdown polythionic-acid risk | Confirm stabilizing treatment needs |
| High-temperature reactor piping | H-grade strength with Nb | Seamless on heavy wall |
| Hot-gas ducting with frequent welds | Stabilized HAZ | Radiograph welded seams |
| Thermal processing headers | Creep and cycling | Check filler choice on the WPS |
Reading the table, the common thread is heat: TP310HCb is rarely bought for room-temperature corrosion alone, where cheaper grades do the job. Typical size mixes run from instrument connections at NPS 1/2–2, through process lines at NPS 3–8, up to welded ducts at NPS 12–24, and the availability of fittings and flanges in matching chemistry can limit the line list, so check companion components before the isometrics are frozen. When TP310HCb replaces another grade in an existing unit, review the weld procedures as well, because a base-metal change alone does not update a WPS.
Weldability
TP310HCb welds readily by GTAW, GMAW, SMAW, and SAW, and its fully austenitic structure means no preheat is normally required. The mill longitudinal seam on WLD and HCW pipe is made without filler metal, so the filler question only arises for field and shop joints. Table 6 of A312 shows no AWS filler classification for TP310HCb, which means the filler is selected by agreement on the welding procedure specification rather than dictated by the pipe standard.
In practice the WPS will usually choose a matching 310-type filler, or a richer one where dilution or dissimilar joints are involved, and that choice should be documented and qualified for the service temperature. Because the grade combines creep strength with stabilization, the filler should be chosen with both in mind, and the procedure qualification should reflect the service temperature. Keep interpass temperatures controlled, as for other high-alloy austenitics, to limit hot-cracking risk in a fully austenitic weld, and avoid long holds in the carbide-precipitation range during repair welding.
Surface Finishes
A312 requires pipe to be free of scale and contaminating iron particles, and the way that condition is reached becomes the surface finish. For TP310HCb, which mostly goes into hot service, the finish is usually chosen for cleanliness and inspection rather than appearance, but it still needs to be stated on the order so the mill and the receiving inspector are working to the same expectation.
- Annealed and pickled — the standard mill finish for most sizes; matte and free of scale
- Bright annealed — for smaller sizes where a clean, oxide-free bore is wanted; the anneal must still meet the Table 2 minimum
- Blasted and pickled — common on heavier walls and larger diameters
- Polished — by agreement where internal or external roughness is specified
- Passivated — on request where the end-user specification asks for it
Inspection and Testing
Base inspection and testing for ASTM A312 TP310HCb combine chemistry, mechanical, and integrity checks, and the list below is the usual acceptance package. Supplementary requirements apply only when they are written on the purchase order.
- Heat analysis — every heat against Table 1 for TP310HCb, including C 0.04–0.10%, Cr 24.0–26.0%, Ni 19.0–22.0%, Mo ≤0.75%, Nb 10×C min / 1.10 max
- Product analysis — when ordered, using A480 Table A1.1 tolerances
- Tension test — Table 4 tensile, yield, and elongation on a lot basis (75/30 ksi minima)
- Grain size — ASTM grain size No. 6 or coarser
- Flattening test — or the alternative bend where permitted, typically on 5% of the lot
- Hydrostatic or electric test — every length; manufacturer’s option unless the order fixes the method
- Visual and dimensional check — against the ordered size and the tolerance clauses
EN 10204 3.1 is the standard certificate from SHH STEEL supply. For this grade it must show the carbon value against the 0.04–0.10% band, the niobium value so Nb ≥10×C can be checked, the Table 5 grain-size result, and the heat-treatment lot. EN 10204 3.2 or third-party witness by SGS, Bureau Veritas, TÜV, or the buyer’s nominated agency is arranged when specified, and the inspector should be booked before final testing rather than after the pipe is packed.
Supplementary options worth considering for TP310HCb are summarized below; none of them applies unless the order names it.
| Option | Purpose |
|---|---|
| S1 product analysis | Confirms chemistry on the finished pipe |
| S5 radiography | Weld integrity on WLD pipe |
| S7 intergranular corrosion | A262 Practice E check of the as-supplied condition |
| S8 minimum wall | Wall ordered as minimum rather than nominal |
| S9 weld decay | Compares weld and base-metal loss rates |
On receipt, check the stencil reads TP310HCb or S31041 and not just “310,” then compare the certificate against the limits above. Confirm the niobium arithmetic against the reported carbon before release. Positive material identification by optical emission on a sample length is a sensible extra when several 310-family grades share the same storage area, because handheld XRF cannot resolve carbon and is limited for niobium.
Packaging and Shipping
Packaging for ASTM A312 TP310HCb is chosen to keep the surface free of iron contamination and the ends protected through export transit. Each length carries the A312 marking required by clause 17, normally including the manufacturer, the specification, the grade, the manufacturing type, the size, the heat number and heat-treatment lot, and the test method, and the packing list repeats those identifiers so bundles can be checked without unpacking.
- End caps on all lengths; bevel protectors on beveled ends
- Bundles strapped with non-metallic or covered straps to avoid contact with carbon steel
- Wooden cases or crates for bright-annealed, polished, or thin-wall pipe
- Moisture protection for sea freight on request
- Packing lists that match heat numbers to bundle numbers
Why Choose SHH STEEL
SHH STEEL supplies specification-driven stainless pipe, and for ASTM A312 TP310HCb we quote against the edition you name rather than a generic catalogue sheet. We report the full Table 1 chemistry, the Table 4 results, and the heat-treatment evidence the grade calls for, and we match the manufacturing route and size to the enquiry instead of pushing whatever is nearest on the shelf.
- Both controls on one certificate — carbon band, grain size, and niobium arithmetic
- Straight advice when a sister grade such as TP310S or TP310H would actually suit the service better
- SML, WLD, and HCW routes with EN 10204 3.1 certificates; 3.2 inspection on request
- Dual A312/SA-312 marking only when the purchase order asks for both standards
- Cut lengths, beveling, and project packing coordinated on confirmed orders
If you are still choosing between 310-family grades, send the design temperature, the atmosphere, whether the line is welded heavily in fabrication, and whether shutdown condensate is expected. We will answer with the grade that fits that combination rather than the one whose name is closest to the datasheet.
Supply Capability
SHH STEEL can supply ASTM A312 TP310HCb / UNS S31041 stainless steel pipe to the edition and manufacturing type named on your enquiry. The table summarizes the routes, sizes, finishes, and documents we regularly quote for this grade, and it is a capability statement rather than a promise that every combination is in stock today.
| Item | SHH STEEL capability for TP310HCb |
|---|---|
| Standard | ASTM A312 / A312M TP310HCb / UNS S31041 |
| Manufacturing types | SML, WLD, HCW |
| Size | NPS 1/8 and up per ASME B36.19; special OD/wall by agreement |
| Schedules | 5S, 10S, 40S, 80S and non-standard walls |
| Length | SRL, DRL, or cut-to-length |
| Finish | Annealed and pickled; blasted and pickled; bright annealed or polished by agreement |
| Testing | Tension (75/30 ksi), flattening/bend, hydro or NDE per length; Table 5 grain size No. 6 or coarser; Nb arithmetic on MTC; S1/S5/S7/S8/S9 on order |
| Documents | EN 10204 3.1; third-party inspection / 3.2 on request |
| Trade terms | FOB / CFR / CIF / EXW and other agreed Incoterms |
Stock / Available sizes. The representative range for TP310HCb is set out in the Dimensions section: NPS 1/2–24 with Sch 10S, 40S, and 80S as typical, plus special OD × wall on enquiry. Selected common sizes may be available from stock or recent heats, while heavy-wall seamless, unusual schedules, and special cut lengths are normally mill-order. We do not invent stock lists or tonnage claims, so ask for a live check against your size list.
A good enquiry for this grade states the A312 edition, TP310HCb (UNS S31041), the manufacturing type, NPS or OD × wall with nominal or minimum wall, length practice, finish, and any product-analysis, corrosion-test, or 3.2 requirement. With that information we can line up a mill slot or a stock allocation against your need date, and combining project sizes into one heat helps with chemistry consistency and mill minimums.
FAQ
-
Is ASTM A312 the same as ASME SA-312 for TP310HCb?
- No. ASTM A312/A312M and ASME SA-312 are two independent standards, even though the referenced editions are closely aligned on Table 1 chemistry, Table 4 tensile values, and most testing language for TP310HCb. If the piping is built to the ASME Code, name both standards on the purchase order and ask for dual marking; otherwise order to ASTM A312 alone and do not treat the titles as synonyms.
-
What is the UNS number for ASTM A312 TP310HCb?
- The UNS number is UNS S31041. It identifies the same chemistry across product forms, so plate to ASTM A240 and pipe to ASTM A312 can share it, but the pipe still has to be ordered and certified to A312. Put both the TP designation and the UNS number on the order and check that both appear on the certificate and the stencil.
-
What chemical composition defines TP310HCb pipe?
- Table 1 of ASTM A312 sets C 0.04–0.10%, Cr 24.0–26.0%, Ni 19.0–22.0%, Mo ≤0.75%, Nb 10×C min / 1.10 max, with Mn ≤2.00%, Si ≤1.00%, P ≤0.045% and S ≤0.030%. Those limits apply to the heat analysis; product analysis, when ordered, uses the A480 Table A1.1 tolerances, which widen individual readings slightly but never replace the heat requirement.
-
What are the tensile requirements for ASTM A312 TP310HCb?
- Table 4 requires 75 ksi [515 MPa] minimum tensile strength and 30 ksi [205 MPa] minimum yield strength, with elongation of 35% longitudinal and 25% transverse. These are the same floors as the other 310-family grades. There is no hardness maximum in Table 4, so any hardness limit for bending or expanding must be written on the order.
-
TP310HCb vs TP310H — what does niobium add?
- Both are H grades with a 0.04–0.10% carbon band and ASTM grain size No. 6 or coarser, but TP310HCb adds niobium at 10×C minimum and 1.10% maximum. The niobium stabilizes carbon so welded zones are less prone to sensitization during shutdown, which is the usual reason to pay the premium. Where welds never see aqueous conditions, TP310H may be enough.
-
TP310HCb vs TP309HCb — which grade suits higher temperature?
- The 310 family, with chromium 24.0–26.0% and nickel 19.0–22.0%, has more oxidation and scaling margin than the 309 family at 22.0–24.0% chromium, so TP310HCb is the more conservative choice for the hottest sections, while TP309HCb covers many lines more economically. The step between families is mainly about oxidation margin, not room-temperature strength, because both share the 75/30 ksi Table 4 floor. Choose by the actual atmosphere and metal temperature, and remember that the richer grade costs more and can be harder to source in special sizes.
-
What heat treatment applies to ASTM A312 TP310HCb pipe?
- Table 2 lists TP310HCb at 1900 °F [1040 °C] minimum followed by rapid cooling. Because it is an H grade, clause 6.2 requires the pipe to be reheated to that temperature before quenching, so direct quench after hot forming is not accepted, and the heat-treatment lot must be marked on each length.
-
Seamless vs welded TP310HCb pipe — which is better?
- Neither is better in general. Seamless suits heavy walls, high pressure, and line classes that exclude welded pipe, while welded pipe is economical on larger diameters and thinner walls and is common in furnace ducting. Both must meet the same Table 1 chemistry and Table 4 tensile values, and the choice should follow the design code and the inspection plan.
-
What filler metal is used to weld TP310HCb pipe?
- Table 6 of ASTM A312 shows no AWS filler classification for TP310HCb, so the filler is chosen by agreement and recorded on the welding procedure specification. A matching 310-type filler is typical, with a richer filler for dissimilar joints, and the procedure should be qualified for the service temperature rather than copied from a room-temperature job.
-
Hydrostatic test vs NDE — which do I get on TP310HCb pipe?
- Every length receives either a hydrostatic test or a nondestructive electric test, and the manufacturer chooses unless the purchase order specifies one. If your inspection plan depends on a particular method, write it on the order. Pipe NPS 10 and larger may ship marked “NH” only when the purchaser accepts a system test instead of the hydrotest.
-
Does TP310HCb require grain-size control?
- Yes. Table 5 requires ASTM grain size No. 6 or coarser for TP310HCb, and the result should be reported on the certificate together with the heat-treatment lot. The coarser grain supports creep strength at elevated temperature, which is why H grades carry this requirement and the S and plain Cb grades do not.
-
How do I check the niobium on a TP310HCb certificate?
- Take the reported carbon, multiply by ten, and confirm the niobium value is at least that figure and no more than 1.10%. For example, C 0.06% needs Nb at least 0.60%. Product tolerance does not relax the heat-analysis floor, and handheld XRF is not reliable for niobium, so use the mill certificate or lab analysis.
Conclusion
ASTM A312 TP310HCb / UNS S31041 is the niobium-stabilized H grade that combines a controlled carbon band with grain-size control of the 25Cr–20Ni family, with C 0.04–0.10%, Cr 24.0–26.0%, Ni 19.0–22.0%, Mo ≤0.75%, Nb 10×C min / 1.10 max, a 75/30 ksi Table 4 floor with 35% L / 25% T elongation, and a solution anneal at 1900 °F [1040 °C] minimum with clause 6.2 reheat and grain size No. 6 or coarser. It is ordered for heat, not for general corrosion, and it is not a drop-in for A312 TP310S. Put the manufacturing type, size and wall basis, finish, and the grade-specific evidence on the purchase order, then review the EN 10204 3.1 certificate before release. SHH STEEL can supply TP310HCb pipe to the edition you name; browse the sister grades on the A312/A312M hub, or send your size list to admin@steelspecs.com.
Quality Steel Needed? Inquire for Offers
Related Products